Featured Recycled Polymer Drinkware & Precision Closures
Explore commercialized drinkware units, leak-proof helmet caps, and ergonomic straw assemblies fabricated from post-consumer recycled feedstocks and food-grade polymers under certified ISO cleanroom protocols.
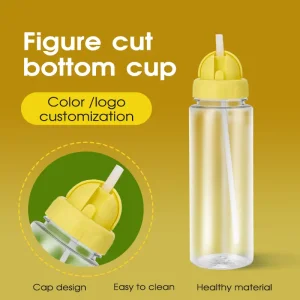
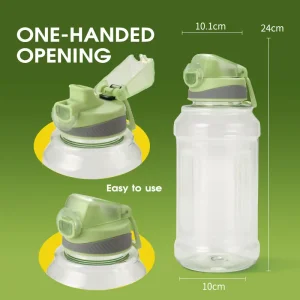
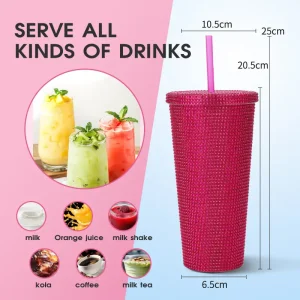
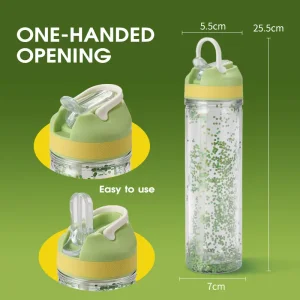
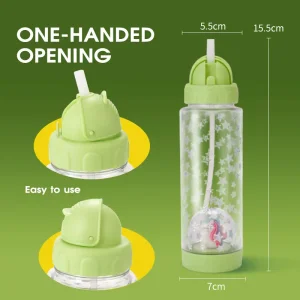
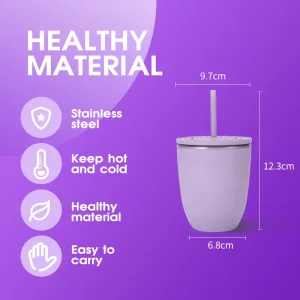
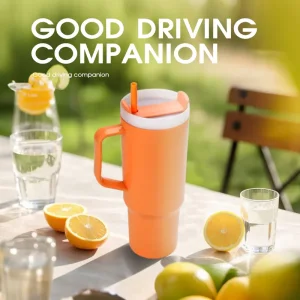
The Paradigm Shift: From Downcycling to Food-Grade Bottle Valorization
Over the past decade, China’s industrial recycling architecture has transformed from labor-intensive mechanical separation into high-precision, AI-sorted, chemical-grade re-polymerization complexes capable of meeting strict international food-contact mandates.
In mature manufacturing provinces like Zhejiang, bottle recycling has evolved far beyond the extraction of low-grade polyester fibers for non-woven textiles. Modern suppliers operating within the Jinhua and Wuyi industrial corridors utilize advanced optical sorting systems featuring short-wave infrared (SWIR) and hyper-spectral imaging to segregate post-consumer polyethylene terephthalate (PET) and polypropylene (PP) with 99.8% material purity. This incoming waste stream is processed through multi-stage caustic wash cycles, vacuum decontamination chambers, and solid-state polycondensation (SSP) reactors.
For international consumer brands, drinkware distributors, and supermarket sourcing divisions, sourcing recycled bottle products from Chinese industrial partners offers an unprecedented synergy of regulatory compliance and cost competitiveness. Rather than relying on single-origin European or North American compounders who face persistent recycled flake supply deficits, Chinese factories maintain extensive domestic reclamation networks. This ensures that custom injection molds, double-wall tumblers, and vacuum bottles manufactured with 30% to 100% PCR content achieve uniform color consistency, superior tensile strength, and zero non-food contact contaminants.
Engineering Metrics: Virgin vs. Post-Consumer Recycled (PCR) Resins
Specifying post-consumer drinkware requires strict adherence to intrinsic viscosity (IV), thermal degradation boundaries, and global food contact migration limits. Our factories execute laboratory-grade validation for every production run.
| Polymer Category | Intrinsic Viscosity (dL/g) | De-Polymerization Method | Acetaldehyde (AA) Content | FDA / EFSA Food Compliance | Optimal Drinkware Application |
|---|---|---|---|---|---|
| Food-Grade rPET (Bottle-to-Bottle) | 0.80 - 0.84 ± 0.02 | Mechanical Super-Clean + SSP Reactor | < 1.0 ppm (EU Standard) | Approved (FDA LNO / EFSA) | Single-wall cold tumblers, clear outer shells, dome lids |
| Post-Consumer Recycled PP (PCR-PP) | MFR: 12 - 25 g/10min | Multi-stage Extrusion & Vacuum Degassing | Not Applicable (Odor-Stripped) | Approved (EC 1935/2004) | Screw caps, spring-loaded flip lids, insulated base covers |
| Tritan™ Renew (Bio/Circular) | Specialty Copolyester | Chemical Molecular Recycling (Glycolysis) | Zero Detection | Fully Approved Global | High-impact shatterproof kids tumblers, dishwasher-safe bottles |
| Ocean-Bound Plastics (OBP) | 0.74 - 0.78 | Mechanical Intensive Cleaning | < 3.0 ppm | Outer Component Only | Non-contact handles, carrying straps, outer decorative sleeves |
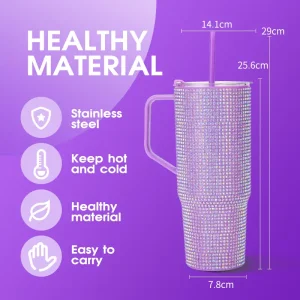
| 304 Stainless / PCR Composite | Structural Metallic | Recycled Metallurgical Smelting (60%+ Scrap) | Nil Leachables | FDA / German LFGB | Stanley-style double-wall vacuum vessels, iced-coffee mugs |
SSP Viscosity Stabilization
Solid State Polycondensation raises the intrinsic viscosity of post-consumer PET flakes up to 0.84 dL/g. This prevents wall embrittlement during high-speed injection-stretch blow molding (ISBM), guaranteeing superior drop resistance for sports water bottles.
VOC & Odor Desorption
Thermal desorption under high vacuum conditions extracts volatile organic compounds (VOCs), detergent residue, and volatile flavoring compounds from incoming post-consumer flakes, ensuring zero taste alteration in cold tea or coffee applications.
Pantone Color Neutralization
High-purity optical color-sorting combined with proprietary blue/violet color-correcting masterbatches balances the subtle grayish or yellowish tint common in recycled PET, allowing vibrant custom Pantone finishes without compromising GRS compliance.
Why Global Brands Consolidate Recycled Drinkware Sourcing in China
The unique concentration of tooling workshops, precision injection molding facilities, decoration specialists, and ocean freight logistics in Zhejiang establishes an impenetrable competitive advantage in speed-to-market and unit cost.
Vertically Integrated Ecosystem
Within a 30-kilometer radius in Jinhua/Wuyi, raw pellet suppliers, rapid tooling specialists, electroplating plants, silicone gasket compounders, and carton fabricators operate cohesively. This enables rapid prototype iterations in just 7 days.
Domestic Feedstock Price Stability
Unlike Western markets subject to sharp price volatility in recycled resin due to localized bottle collection deficits, Chinese recycling processors maintain vast, standardized municipal and commercial recycling networks, delivering predictable FOB costs.
High-Tonnage Precision Tooling
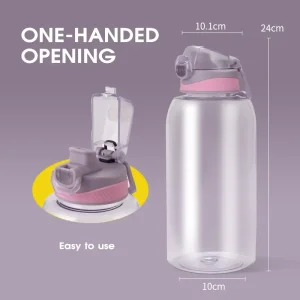
Our affiliated production floors maintain high-precision Haitian and Demag injection molding machines ranging from 120T to 650T. Multi-cavity hot-runner systems ensure ultra-tight dimensional tolerances for spring-loaded leak-proof lids and twist caps.
Advanced Automated Decoration
In-house surface treatment covers automated gradient spray painting, rhinestone drill sticker application, electrostatic powder coating, UV printing, and physical vapor deposition (PVD) vacuum electroplating—all configured for PCR substrate adhesion.
Port Proximity & Logistics Hub
Direct highway access to Ningbo and Shanghai ports guarantees container drayage within 4 to 6 hours. Global forwarders benefit from streamlined export clearance, palletization optimization, and temperature-controlled dry container loading.
Full Chain-of-Custody Documentation
Every shipment of recycled drinkware is accompanied by verifiable Transaction Certificates (TCs), raw material batch numbers, non-intentionally added substances (NIAS) screening reports, and heavy metal compliance verification.
Global Regulatory Framework & Enterprise Procurement Safeguards
Navigating cross-border customs regulations and food-contact compliance requires rigorous institutional oversight. We align all manufacturing workflows with FDA, EU, and California standards.
| Regulatory Standard | Jurisdiction | Key Testing Parameters | Factory Enforcement Method |
|---|---|---|---|
| FDA 21 CFR 177.1630 / 177.1520 | United States | Overall migration in distilled water, 10% ethanol, n-heptane; chloroform-soluble extractives | Batch testing by SGS / Intertek with FDA Letter of No Objection (LNO) verified polymers |
| EU Regulation No 10/2011 & (EC) 1935/2004 | European Union | Overall Migration Limit (OML < 10 mg/dm²), Specific Migration Limits (SML) for heavy metals, phthalates, and bisphenols | Migration testing using 3% acetic acid, 10% ethanol, and vegetable oil food simulants |
| German LFGB § 30 and 31 | Germany / EU Premium | Sensory evaluation (taste and odor transfer), overall migration, volatile organic components (VOCs) | Extended de-gassing thermal treatment and odorless food-grade silicone seals |
| California Proposition 65 | State of California, USA | Total lead content (< 100 ppm), cadmium, phthalates (DEHP, DBP, BBP, DINP, DIDP, DnOP < 0.1%) | Rigorous XRF screening of all color pigments, electroplating layers, and adhesive compounds |
| Global Recycled Standard (GRS 4.0) | International / ESG Audits | Chain of custody, environmental chemical management, social responsibility compliance | Annual third-party audit by Control Union / Intertek; automated TC issuing per export lot |
Quality Assurance Protocol for PCR Drinkware Production
Post-consumer plastics inherently present challenges regarding material variance and micro-contaminants. To address this, our quality control team implements an Eight-Point In-Line Inspection Matrix across every OEM production batch:
- Incoming Flake Spectroscopy: NIR scanning of resin lots to identify and reject PVC contamination below 10 ppm.
- Melt Flow Rate (MFR) Testing: Verification of batch fluidity to ensure consistent wall thickness in multi-cavity injection.
- Microbial Bioburden Analysis: High-temperature autoclave sterilization testing for caps and drinking spouts.
- Hydrostatic Vacuum Leak Testing: Positive and negative pressure decay testing for all sealed lids and tumbler bases.
- Adhesion Cross-Hatch Testing: ASTM D3359 standard tape tests on electroplated and gradient-sprayed surfaces.
- Thermal Cycling Stress: Alternating -20°C to +100°C shock resistance testing to prevent lid cracking.
From Baled Bottle to Finished Drinkware: 5 Controlled Stages
Our facility bridges the gap between raw bottle waste and high-value consumer lifestyle products through robotic automation, cleanroom injection, and strict quality gates.
Optical Sorting & Hot Flaking
Post-consumer PET bottles are de-labeled, crushed into 8-12mm flakes, optical-sorted by spectral color, and hot-washed with alkaline detergents to strip adhesives.
SSP Reactor Decontamination
Flakes undergo vacuum extrusion and solid-state polycondensation at 210°C to rebuild polymer molecular chains, extract VOCs, and guarantee food-safe chemical purity.
Precision Tooling & Molding
Pellets are molded on servo-electric injection presses using mirrored cavity steel tooling, ensuring burr-free spring closures, threads, and ergonomic handle contours.
Robotic Finishing & Assembly
Automated gradient spraying, electroplating, drill sticker affixing, and laser etching occur in cleanrooms, followed by ultrasonic gasket sealing and straw integration.
AQL 1.0 Inspection & Freight
Final random inspection under ISO 2859-1 standards checks visual finish, cap torque, drop impact, and barcode integrity before container loading for Ningbo dispatch.
Commercial Deployment Scenarios Across Global Channels
Different retail environments and institutional procurement programs require customized balance between recycled content, decoration aesthetics, and unit price points.
Tier-1 Supermarket & Retail Chains
Custom packaging, high-visibility shelf-ready display boxes (FSDU), barcode scan verification, and GRS hangtags designed for Walmart, Target, Carrefour, and Aldi procurement guidelines.
Corporate ESG Merchandising
Fortune 500 employee welcome kits and international conference gifts featuring exact corporate Pantone matching, laser-engraved logos, and quantified lifecycle CO2 reduction metrics.
Specialty Coffee & Quick-Service Chains
Reusable barista-standard straw tumblers and splash-proof hot drink lids engineered with heat-resistant PCR-PP to support circular deposit-return cup systems in municipal cafes.
High-Performance Sports & Fitness
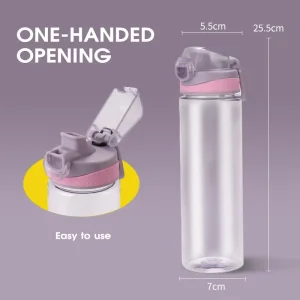
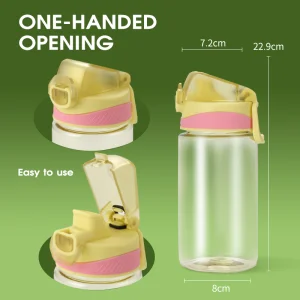
Lightweight 650ml to 1100ml hydration bottles featuring ergonomic finger-loops, one-touch spring pop-up lids, motivational time markings, and impact-modified polymer blends.
Trend-Led Fashion & Influencer Merchandising
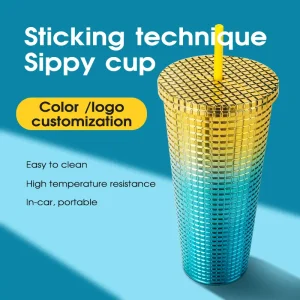
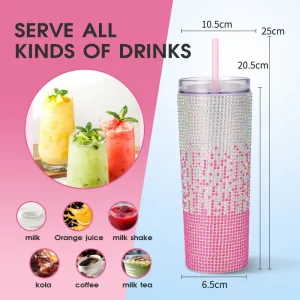
Eye-catching diamond drill stickers, electroplated metallic gradients, and rivet insulated tumblers designed for TikTok viral marketing, Amazon FBA bestsellers, and youth lifestyle boutiques.
Educational & Campus Sustainability
BPA-free student hydration sets featuring shatterproof construction, hygienic covered spouts, and personalized name-badge areas to replace disposable single-use plastic across school districts.
Future Trends Shaping Bottle Recycling & Drinkware Manufacturing
Anticipating regulatory tightening and consumer preferences ensures procurement strategies remain resilient against global trade tariffs and environmental restrictions.
Digital Product Passports (DPP)
By 2027, EU regulations will mandate QR-coded Digital Product Passports for drinkware items. Our factory lines are already integrating laser-etched matrix codes linking directly to raw material batch test records and recycling origin data.
Mandatory Recycled Content Quotas
With the EU Packaging and Packaging Waste Regulation (PPWR) requiring minimum 30% to 50% post-consumer content across consumer plastics by 2030, our R&D team has pre-validated 100% rPET formulations that maintain pristine optical clarity.
Chemical De-Polymerization Scale
Moving beyond mechanical flaking, China's massive investment in enzymatic and glycolytic chemical recycling unlocks infinite circular loops, breaking post-consumer bottles back down to pure DMT and MEG monomers with identical qualities to virgin petroleum resin.
Frequently Asked Questions: Sourcing Recycled Bottles & Tumblers
Clear, authoritative technical answers addressing minimum order volumes, material safety verifications, tooling turnaround times, and global shipping terms.
How can buyers authenticate genuine post-consumer recycled (PCR) content versus virgin resin?
Authentication is achieved through a multi-tier documentation and laboratory validation framework. First, we provide Global Recycled Standard (GRS 4.0) Transaction Certificates (TC) issued by independent certification authorities such as Intertek or Control Union for every export lot. Second, laboratory differential scanning calorimetry (DSC) and carbon-14 (C14) isotope testing can verify non-virgin polymer origins. Finally, our factory maintains rigorous chain-of-custody documentation linking every production shift to specific, traceable compounder batch lot numbers.
Are recycled PET and PCR-PP drinkware items completely safe for warm and acidic liquids?
Yes, provided the proper material grade is selected for the specific operational use-case. Our food-grade rPET is optimized for cold and ambient beverages up to 55°C (such as iced tea, fruit infusions, and chilled water). For warm beverages, coffee, and dishwasher exposure, we formulate lids and vessel bodies from food-grade PCR-PP (Polypropylene) or Tritan Renew, which maintain heat distortion temperatures (HDT) exceeding 100°C without leaching phthalates, BPA, or harmful micro-contaminants.
What is the typical Minimum Order Quantity (MOQ) for custom molds versus custom colors?
For existing factory tooling models (such as our YS series caps, egg-shaped tumblers, and sports bottles), the standard MOQ is 1,000 to 3,000 units with custom Pantone exterior spraying and custom silk-screen or laser logos. For bespoke custom tooling requiring new 3D injection molds, our engineering workshop initiates mold steel fabrication (P20 or S136 hardened stainless steel) with an MOQ of 10,000 units, accompanied by comprehensive DFM (Design for Manufacturability) analysis.
Does incorporating post-consumer recycled plastic cause surface defects or color hazing?
Our vacuum SSP processing and micro-filtration pellets reduce black specks and impurities to less than 0.01 per square decimeter. While raw un-tinted 100% rPET exhibits a very mild grayish-blue hue due to prior thermal cycles, our coloration laboratory neutralizes this using optical brighteners or vibrant custom tints (including macaron gradients, translucent frost, and opaque solid shades), delivering a flawless retail shelf presence indistinguishable from virgin resin.
What third-party factory audits and social compliance standards do your facilities maintain?
Our affiliated manufacturing sites in Wuyi and Jinhua maintain active certifications for ISO 9001 (Quality Management), ISO 14001 (Environmental Stewardship), and ISO 45001 (Occupational Health & Safety). In addition, we routinely pass international retailer ethical audits including BSCI (Business Social Compliance Initiative), SMETA 4-Pillar, and Disney FAMA authorizations. Overseas audit teams and third-party inspectors like SGS or Bureau Veritas are fully supported on-site.
What are standard sample lead times and mass manufacturing turnaround windows?
Rapid 3D printed prototype samples are delivered within 48 to 72 hours. Molded physical samples with Pantone color formulation and brand logos require 7 to 12 calendar days. Following final pre-production sample sign-off, mass production generally requires 25 to 35 days, contingent upon order volume and secondary decoration complexity. We provide weekly visual progress reports and pre-shipment container loading inspections.
How do Chinese factories assist buyers with EPR and carbon border tax (CBAM) accounting?
We provide full Life Cycle Assessment (LCA) data packages detailing kilowatt-hour consumption per piece, resin carbon offsets (typically 1.4 kg to 2.1 kg of CO2 equivalent saved per kg of PCR utilized compared to virgin resin), and standardized tare weight disclosures. This documentation integrates directly into European Extended Producer Responsibility (EPR) reporting portals and corporate ESG filings.
Specialty Closures, Rhinestone Tumblers & Custom Hydration Units
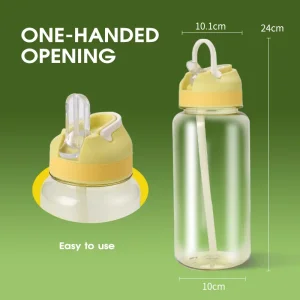
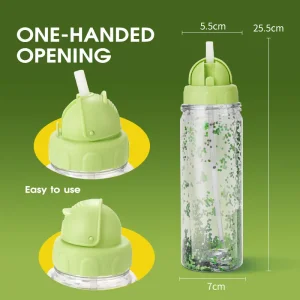
Explore our expanded series of spring-loaded push caps, electroplated grid finishes, and drill sticker tumblers engineered for maximum shelf appeal and reliable circular performance.
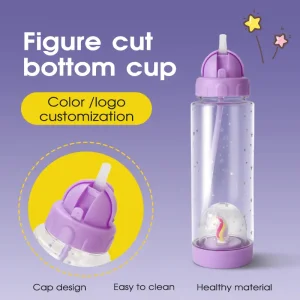
Initiate Your Sustainable Drinkware Development Cycle
Partner directly with Wuyi Ronchine Industry & Trade Co., Ltd. for verified food-contact compliance, low tool investment costs, and reliable container-load delivery. Speak with our bilingual engineering team today.