Certified GRS-Grade & Precision-Formed Drinkware Prototypes
Direct factory-floor tooling models available for OEM/ODM private-label scaling, featuring post-consumer recycled (PCR) stainless steel, electroplated gradient CMF, and hermetic lid engineering.
Solving Scope 3 Emissions in Global Drinkware Supply Chains
As European CBAM regulations and corporate ESG mandates accelerate, shifting from virgin austenitic steel to verified Global Recycled Standard (GRS) material is the primary lever for B2B brand compliance.
CBAM & CSRD Readiness
Under the EU Carbon Border Adjustment Mechanism (CBAM) and Corporate Sustainability Due Diligence Directive, importers must document embedded carbon emissions. Our GRS-certified production facilities track precise embodied emissions per metric ton of melted scrap, providing verifiable primary data rather than generic industry averages.
73% Life-Cycle Carbon Reduction
Transitioning from virgin nickel-chromium ore smelting to electric arc furnace (EAF) remelting of post-consumer 304 and 316 scrap reduces life-cycle carbon intensity from ~6.8 kg CO2e/kg down to <1.85 kg CO2e/kg. This provides multinational drinkware brands with substantial, audit-ready Scope 3 reductions.
Zero Greenwashing Vulnerability
Retail litigation regarding unsubstantiated environmental claims is rising across North America and the EU. By pairing Textile Exchange Content Claim Standard (CCS) verification with individual Transaction Certificates (TCs) for every production batch, we eliminate marketing liability for our OEM/ODM distributors.
China Factory 4.0: The Wuyi-Yongkang Hardware Hub Superiority
Centering your production in Wuyi County, Zhejiang province leverages the world’s dense stainless steel hardware manufacturing belt, integrating tooling, deep drawing, automated polishing, and high-vacuum lines within a 15-kilometer radius.
Intelligent CNC Hydroforming & Drawing
Our facility operates multi-station synchronized hydraulic presses equipped with progressive servo-die tooling. This ensures wall thickness uniformity down to 0.40mm on inner liners while maintaining tensile strength, reducing raw material mass without compromising structural integrity or vacuum collapse thresholds.
Automated Lead-Free Vacuum Brazing
Traditional drinkware manufacturing relied on lead-containing glass beads for vacuum port sealing. Our modern automated continuous vacuum furnace lines utilize pure copper-alloy and silver-matrix induction brazing at 1050°C under 10⁻⁴ Pa negative pressure, guaranteeing 100% non-toxic, non-leaching thermal barriers.
Cluster Agility & Rapid Tooling
With raw stainless slitting centers, injection molding partners for lids, silicon gasket vulcanization facilities, and automated electrostatic powder coating workshops located immediately within the Wuyi industrial grid, new product sampling cycles are compressed to 7–12 days from CAD sign-off.
Recycled Metallurgy Roadmap: Microstructure & Alloy Integrity
Maintaining strict food-contact safety requires rigorous chemical composition controls during scrap re-melting. Our GRS-certified 304 and 316 alloys meet or exceed ASTM A240 standards.
Elemental Purity & Spectroscopy Benchmarks
Secondary metallurgy presents risks of residual tramp elements (e.g., Cu, Sn, Pb, As) that degrade corrosion resistance or compromise food safety. Every master coil batch received from our GRS-certified rolling mills undergoes Optical Emission Spectroscopy (OES) testing to confirm:
- Chromium (Cr 17.5% – 19.5%): Stable passive chromium oxide (Cr2O3) boundary layer prevent pitting corrosion from acidic fruit juices and cold-brew beverages.
- Nickel (Ni 8.0% – 10.5%): Maintains stable face-centered cubic austenitic grain matrices, crucial for deep drawing ductility and low-temperature impact resilience.
- Carbon (C ≤ 0.07%): Mitigates chromium carbide precipitation along grain boundaries during laser seam welding, preventing intergranular corrosion.
2025–2030 Technical Evolution Roadmap
The technological trajectory of high-performance recycled drinkware is shifting toward closed-loop circular systems and intelligent monitoring. Key milestones currently deploying across our factory lines include:
- Phase 1 (Active): 90%+ PCR post-consumer recycled stainless content for inner and outer vacuum vessels, verified via batch transaction certificates.
- Phase 2 (Active Deployment): Closed-loop factory scrap reclamation, routing 100% of stamping trimmings back to certified induction melt shops.
- Phase 3 (Pilot Testing): Laser-etched QR code digital product passports (DPP) documenting embodied carbon and material origin from mine/scrap yard to shelf.
Global Procurement Specifications: CMF, Tooling & Testing
Tier-1 retailers, promotional brands, and institutional importers demand repeatable mechanical performance and advanced surface treatment options that pass strict retail-level durability standards.
Advanced CMF & Surface Finishes
We provide solvent-free electrostatic powder coating, automated 3D gradient spray finishing, physical vapor deposition (PVD) metallic electroplating, and custom rhinestone drill application. Finishes withstand standard cross-hatch adhesion testing (ASTM D3359 Class 4B/5B) and 100+ commercial dishwasher thermal cycles.
Thermal Retention & Pressure Decay
Double-wall vacuum chambers undergo dual 100% thermal station verification (both infrared thermal image sensing and temperature decay testing). Our baseline standard maintains liquids above 68°C after 6 hours from a 98°C pour, or below 8°C for 24 hours under chilled beverage conditions.
Custom Molds & Amortization Terms
Dedicated OEM tooling for novel lid geometries, ergonomic carry handles, and silicone base boots are managed in-house. Tooling costs are amortized and fully refunded once order volumes cross established program thresholds (typically 50,000 to 100,000 units within a 12-month contract).
Localized Compliance & International Food-Contact Verification
Cross-border distribution requires multi-jurisdictional compliance. Our quality systems ensure end-to-end documentation against major regional market requirements.
US FDA 21 CFR 175.300
Testing confirms total extractive residues and heavy metal migration thresholds under simulated acid and alcohol liquid food environments.
German LFGB & EU 1935/2004
Rigorous sensorial taste tests, volatile organic compound (VOC) tests on silicone components, and extractive testing via SGS or TÜV Rheinland.
California Prop 65
100% total lead and phthalate compliance (CPSC requirements), ensuring no warning labels are required for North American consumer retail.
Textile Exchange GRS 4.0
Full chain-of-custody documentation tracing post-consumer feedstocks from certified recyclers through smelting, drawing, and export crating.
Material Performance Comparison: GRS 304 vs. Virgin 304 vs. Polymers
Select the appropriate material configuration based on thermal duty cycles, retail price targets, and corporate carbon accounting requirements.
| Material Category | Embodied CO2e / kg | Yield Strength (MPa) | Corrosion Resistance | Food Safety Accreditations | Circular Recyclability |
|---|---|---|---|---|---|
| GRS Post-Consumer Recycled 304 | < 1.85 kg | ≥ 205 MPa | High (PREN 18.0 - 20.0) | FDA, LFGB, EU 1935/2004 | Infinite Closed-Loop |
| Virgin Austenitic 304 (06Cr19Ni10) | ~ 6.80 kg | ≥ 205 MPa | High (PREN 18.0 - 20.0) | FDA, LFGB, EU 1935/2004 | High (Energy Intensive) |
| Recycled 316 Marine Grade (PCR) | < 2.20 kg | ≥ 220 MPa | Superior (PREN 23.0 - 25.0) | Medical & Food Certified | Infinite Closed-Loop |
| Virgin Polypropylene (PP) | ~ 2.40 kg | 30 – 40 MPa | Moderate (Acid sensitive) | BPA-Free Options | Downcycled (Degrades) |
| Tritan™ Copolyester | ~ 3.80 kg | 45 – 55 MPa | High (Impact Resistant) | FDA, BPA/BPS Free | Specialized Chemical Stream |
Five-Stage Precision Quality Assurance Architecture
Every production lot moves through five strictly logged quality gates before shipment containers depart Ningbo Port.
Metallurgical Audit
Spectroscopic chemical check of GRS coils; verification of vendor Scope Certificates (SC) and material thickness tolerances.
Laser Seam Welding
Automated longitudinal tube welding under argon shielding gas prevents micro-porosity and ensures airtight joints.
Vacuum Evacuation
Continuous vacuum furnace cycle at 1050°C creates high-vacuum insulation cavity with non-toxic getter activation.
Thermal Decay QC
100% of cups undergo computer-vision robotic infrared temperature reading to identify thermal leakage.
TC Issuance & Pack
Release of final Transaction Certificate (TC) matching export invoice; carton drop testing per ISTA-1A protocols.
High-Demand Commercial Styles & Combination Drinkware Sets
Volume-ready configurations engineered for retail shelves, corporate gifting programs, and e-commerce brands requiring reliable factory lead times.
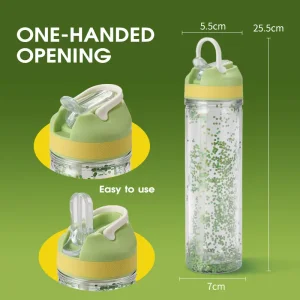
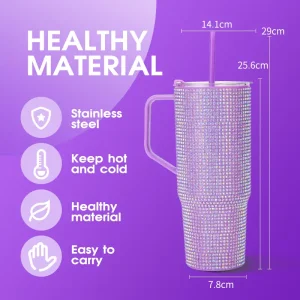
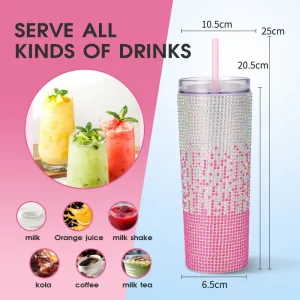
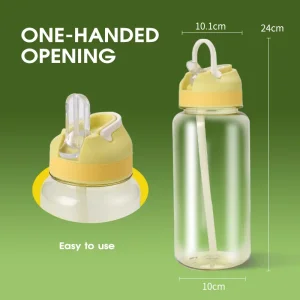
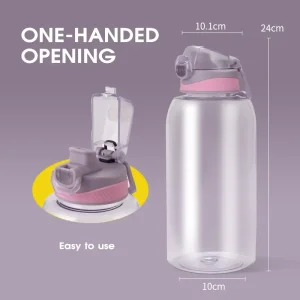
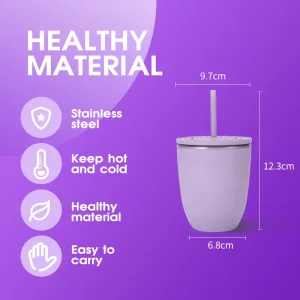
Wholesale Drill Sticker - Tall and Straight YS-2045D Manufacturer, Factory
Explore Engineering Specs
Frequently Asked Sourcing & Compliance Questions
Key facts and operational details regarding GRS documentation, factory minimums, tooling, and shipping procedures.
How is GRS material verified throughout manufacturing?
Verification relies on the Textile Exchange Content Claim Standard. The upstream melting mill issues a Transaction Certificate (TC) for raw coil delivery. During stamping, drawing, vacuum brazing, and packing at our Wuyi factory, identity preservation prevents blending with virgin metals. Upon container loading, an official third-party TC is generated explicitly tying the finished cup quantities and weights to your import bill of lading.
Does recycled stainless steel show lower corrosion resistance?
No. Austenitic grade 304 recycled stainless steel maintains the identical chemical requirements (18% Chromium, 8% Nickel) and microcrystalline face-centered cubic structure as virgin material. It undergoes electrolytic polishing and nitric acid passivation to establish an impermeable chromium oxide film, matching virgin steel performance in 48-hour neutral salt spray (ASTM B117) and artificial saliva/acid testing.
What is your baseline MOQ for custom OEM/ODM programs?
For catalog models using existing tooling with custom Pantone powder-coating and laser-etched logos, minimum order quantities start at 1,000 units. For fully bespoke geometric silhouettes requiring progressive deep-draw molds and custom-molded silicone lids, tooling MOQs begin at 3,000 to 5,000 units, with initial mold fabrication fees credited upon reaching agreed annual delivery volumes.
What lead times apply to sampling and full container shipping?
Rapid 3D-printed aesthetic prototypes are dispatched within 72 hours. Functional stainless steel samples finished in target Pantone colors and brand graphics take 7 to 12 days. Full 40HQ container production (approx. 24,000 to 36,000 double-wall tumblers) requires 30 to 38 calendar days following pre-production sample sign-off, direct from our factory to Ningbo or Shanghai port.
Are lids and accessories also certified eco-friendly?
Yes. Beyond our stainless vessels, we offer circular accessory streams including certified Post-Consumer Recycled Polypropylene (PCR PP), Recycled Tritan™ Copolyester, food-grade biodegradable PLA, and natural ocean-bound plastics. All polymer formulations are free of BPA, BPS, and ortho-phthalates, accompanied by corresponding FDA 21 CFR and LFGB migration certifications.
How do you verify vacuum insulation integrity prior to crating?
We run a 3-stage validation process: First, pneumatic air-decay pressure testing verifies seam integrity before brazing. Second, raw brazed cups enter an automated multi-sensor infrared chamber that detects thermal dissipation under forced hot air. Third, completed assemblies rest for 14 days in ambient buffer storage before an inspection cycle screens for delayed vacuum leaks.
Partner Directly with Wuyi Ronchine Industry & Trade Co., Ltd.
Headquartered in Wuyi County, Zhejiang, we operate the premier production infrastructure behind the YAMI and Jass Life drinkware brands. We eliminate intermediary trading margins, providing corporate procurement teams with direct factory engineering support, compliant GRS documentation, and dependable container shipments via Ningbo Port.
Direct Export Channels
- Engineering Inquiries: [email protected]
- Direct Phone: +86 579 8770 8330
- Mobile & WhatsApp: +86 150 6802 5714
- Factory Schedule: Monday – Saturday (GMT+8 China Standard Time)