Featured Kids RPET & Eco Drinkware Models
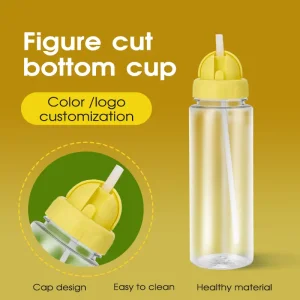
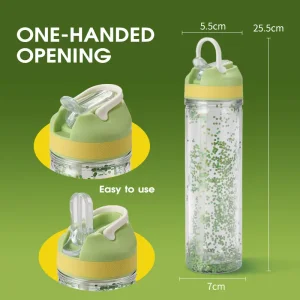
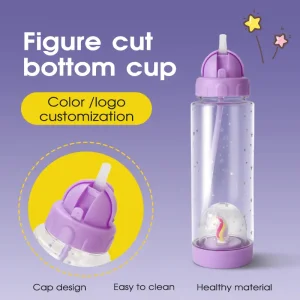
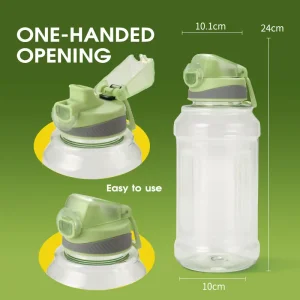
Engineered with 100% food-contact certified resins, child-safe locking spring caps, and impact-modified shatter barriers. Fully customizable for OEM volume programs.
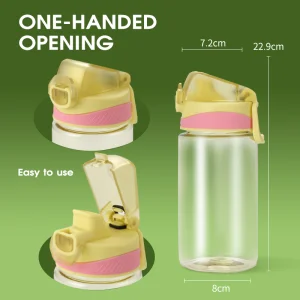
Global Commercial Landscape of RPET Youth Hydration
The global juvenile drinkware sector is undergoing an unprecedented structural transition driven by stringent packaging waste directives, zero-endocrine-disruptor mandates, and circular procurement policies.
Stringent Regulatory Mandates
Global procurement teams must navigate complex regional frameworks including the European Union PPWR (Packaging and Packaging Waste Regulation), California Proposition 65, and US FDA 21 CFR §177.1630. Virgin polymers face growing eco-tariffs, accelerating the shift to certified food-grade Recycled Polyethylene Terephthalate (RPET).
Supply Chain Decoupling
Importers are pivoting away from fragmented trading intermediaries toward integrated industrial manufacturers located in hardware hubs like Wuyi, Zhejiang. Direct-factory governance eliminates middleman markups, reduces sampling iterations from 6 weeks to 7 days, and ensures complete resin lot traceability.
Consumer ESG Consciousness
Millennial and Gen-Z parents actively demand circular economy verifications. Retail SKUs carrying post-consumer recycled certifications experience an average 34% velocity lift over standard fossil-based plastic alternatives, making sustainable RPET the default specification for tier-1 distributors.
Technical Polymer Matrix: Engineering RPET vs Conventional Resins
Selecting the optimal juvenile polymer requires balancing drop fracture toughness, melt processing temperature, optical clarity, chemical inertness, and circular lifecycle documentation.
| Polymer Specification | Intrinsic Viscosity (IV) / Density | Impact Fracture Resistance | Thermal Deflection Limit | BPA / BPS Endocrine Profile | Circular Economy Metric |
|---|---|---|---|---|---|
| Post-Consumer RPET (High-Purity) | 0.80 - 0.84 dL/g | 1.38 g/cm³ | High (Modified Copolymer) | Up to 70°C (Cold/Lukewarm) | 100% Free (Zero Endocrine Risk) | GRS 4.0 Post-Consumer Circular |
| Tritan™ TX2001 Copolyester | N/A | 1.18 g/cm³ | Extreme (Shatterproof) | Up to 95°C (Dishwasher Safe) | 100% BPA/BPS Free | Virgin Petrochemical Origin |
| PP Homopolymer (Random Copolymer) | MFR: 12 - 25 g/10min | 0.90 g/cm³ | Moderate Elasticity | Up to 100°C (Microwave Capable) | 100% BPA Free | Standard Mechanical Recyclability |
| AS (Acrylonitrile Styrene) | MFR: 2.0 - 4.5 g/10min | 1.08 g/cm³ | Brittle under -5°C shock | Up to 65°C (Cold drinks strictly) | BPA Free | Low Recycled Content Compatibility |
| 304 Austenitic Stainless Core | 7.93 g/cm³ | Indestructible Shell | Vacuum Thermal Retention (>12h) | 100% Inert Contact | High Scrappage Circular Value |
Localized Application Scenarios & Global Use Cases
B2B enterprise clients optimize product lines according to distinct consumer environments. Our factory lines adapt closures, base dampers, and decoration formats for each targeted channel.
K-12 Primary School & Kindergarten
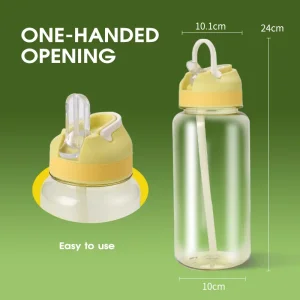
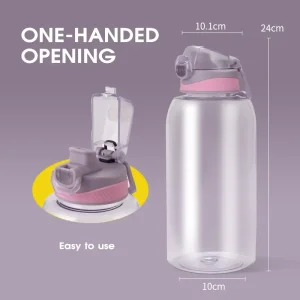
High-volume usage demands anti-spill silicon duckbill valves, one-handed spring-loaded caps with physical lock rings, and reinforced shock-absorbing elastomer bases. Custom molded nameplates prevent mixing in group environments.
Mass Retail & Juvenile Fast Fashion
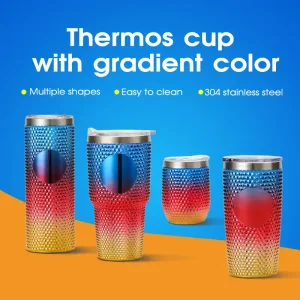
Visual shelf appeal driven by soft-touch gradient spraying, rhinestone drill appliques, electroplated metallic trims, and customized seasonal window gift boxes. High perceived value accelerates register ring for fashion apparel partners.
Outdoor Sports & Junior Camps
Heavy-duty travel parameters featuring quick-release woven carabiner carry straps, tactile matte powder grips, large liquid volume reserves (650ml - 1100ml), and dual-spout caps allowing either wide gulping or controlled straw sipping.
Corporate ESG & Licensed Merchandising
Zero-carbon enterprise activations and Disney/Marvel licensing programs leveraging verified ocean-bound plastic chain-of-custody. Complete GRS transaction certificates (TC) furnished per production batch for investor transparency.
5-Stage Automated Manufacturing & Quality Control Protocol
Wuyi Ronchine operates closed-loop manufacturing centers where high-speed precision molding, dustless decoration, and automated testing ensure zero-defect shipment integrity.
01. Resins Decontamination & Solid-State Polycondensation
Post-consumer flake undergoes high-vacuum decontamination drying at 160°C to eliminate Volatile Organic Compounds (VOCs) and restore Intrinsic Viscosity (IV) before precision injection.
02. Closed-Loop Injection & Stretch Blow Molding (ISBM)
Computer-monitored multi-cavity hot-runner systems mold preforms with uniform wall thickness tolerances (±0.08mm), eliminating weak parting lines and internal micro-stress fractures.
03. Cleanroom Automated Finishing & Adhesion Curing
Robotic arms apply electrostatic gradient lacquering, UV silk-screen printing, and automatic rhinestone adhesive bonding. Curing ovens crosslink polymers for superior chemical scrub resistance.
04. Hydrostatic Pressure & Negative Vacuum Leak Testing
Every lid batch undergoes 50 kPa compressed air immersion testing for 60 seconds followed by multi-angle orbital shaker checks to assure 100% leakproof transit in school bags.
05. AQL 0.65 Final Audits & Ningbo Port Direct Dispatch
Trained QA engineers execute pre-shipment drop tests (1.8m concrete), cross-cut paint adhesion tests (ASTM D3359), and palletize in export-grade cartons with dehumidification packs.
Technology Roadmap: Next-Gen Juvenile Hydration (2025–2030)
Our R&D engineering laboratory in Wuyi is driving three breakthrough pillars to maintain market leadership for our OEM/ODM brand partners.
Phase 1: Nano-Ceramic Barrier Coatings
Engineering ultra-thin silicon dioxide (SiO2) internal plasma barrier coatings on RPET bottles. This eliminates flavor retention, blocks citrus acid etching, and broadens temperature operating envelopes without sacrificing recyclability.
Phase 2: Bio-Based & Enzymatic Degradable Closures
Moving auxiliary components (caps, straws, latch pivots) from petrochemical PP toward bio-attributed PLA/PHA copolymers. Capable of industrial composting while retaining food-contact hygienic compliance.
Phase 3: Digital Product Passports (DPP)
Integrating permanent laser-etched 2D data-matrix codes on each bottle base. Parents scan via mobile camera to inspect exact bottle recycling genealogy, carbon offset equivalents, and batch laboratory safety certificates.
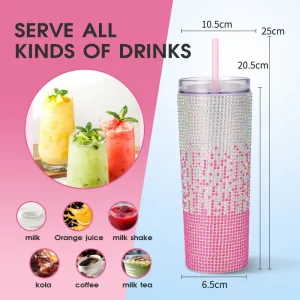
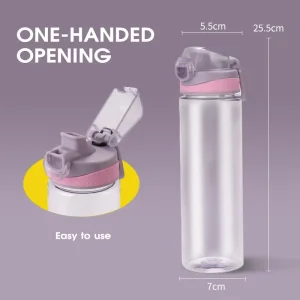
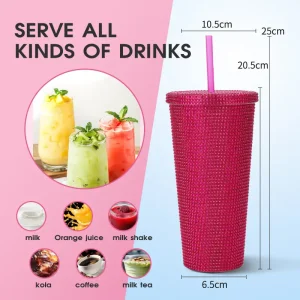
Fashion Inlay, Straw Tumbler & Helmet Series
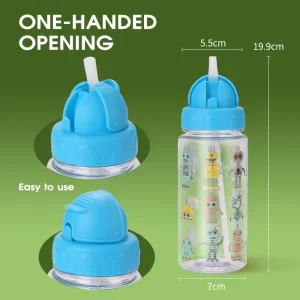
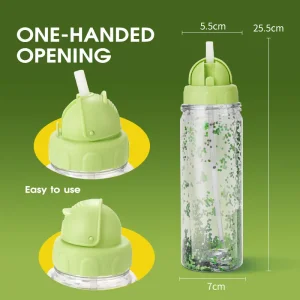
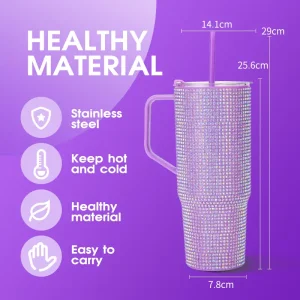
Combining tactile craftsmanship with food-safe polymer precision. Browse our highly sought-after drill-sticker rhinestones, helmet cap lids, and electroplated sets.
Comprehensive B2B Procurement FAQ
Direct answers from our engineering directors regarding resin formulation, food-contact certifications, mold tooling timelines, and global import requirements.
How does your factory verify that RPET bottles are 100% BPA/BPS-Free?
Polyethylene Terephthalate (PET) chemistry inherently does not utilize Bisphenol A (BPA) or Bisphenol S (BPS) during polymerization, unlike polycarbonate. Furthermore, our raw flake suppliers are audited under GRS 4.0 standards, and every resin lot undergoes GC-MS (Gas Chromatography-Mass Spectrometry) third-party testing via SGS or TÜV to confirm zero migration of phthalates, heavy metals, or endocrine disruptors under FDA 21 CFR and LFGB standards.
What are the minimum order quantities (MOQ) for custom private-label runs?
For existing factory toolings (such as our spring-loaded cap or helmet series) featuring custom Pantone bottle color matching and single-color silk-screen branding, our typical MOQ starts at 1,000 to 3,000 units. For completely custom 3D blow-mold designs or bespoke lid tooling, our engineering MOQ is typically 5,000 to 10,000 units, structured to amortize steel tooling expenditures efficiently.
What is the standard turnaround time for sample prototyping and mass production?
Rapid functional prototypes (3D SLS printed samples with functional silicone seals) are dispatched within 5 to 7 working days. Physical injection color-strike samples require 10 to 14 days. Once pre-production samples receive client sign-off, full container production typically takes 25 to 38 calendar days depending on decoration complexity (e.g., gradient spraying or hand-applied rhinestone drill work).
Can your factory produce GRS Transaction Certificates (TC) for customs clearance?
Yes. As a compliant exporter headquartered in Wuyi, Zhejiang, we provide genuine GRS Transaction Certificates for each shipped consignment upon request. This documentation formally certifies the supply chain chain-of-custody from reclaimed post-consumer plastic collection through final molding, allowing our EU and US enterprise clients to legally defend green packaging claims.
What are the thermal and cleaning limitations for RPET juvenile drinkware?
Standard RPET is recommended for cold and lukewarm beverages up to 60°C - 70°C. Exceeding these temperatures during automatic high-heat commercial dishwashing cycles can cause deformation due to polymer relaxation. For programs requiring high-temperature sterilization or boiling liquid resistance, our engineering team recommends our Tritan™ or double-wall stainless steel core lines.
What testing standards are executed for child choke hazard prevention?
All juvenile cap assemblies comply with EN 14350, 16 CFR Part 1501 (Small Parts Regulations), and ASTM F963. Our QA laboratory subjects every bite valve, straw joint, and hinge pin to a continuous 90 N tensile pull test to guarantee that no small components can detach under aggressive biting or pulling by young children.
Initiate Your Custom OEM/ODM Drinkware Project
Partner directly with Wuyi Ronchine Industry & Trade Co., Ltd. Eliminate intermediary trading markups, verify factory audits via live streaming, and acquire certified circular juvenile drinkware designed for market leadership.