High-Efficiency OEM Circular Drinkware Solutions
Engineered for high durability, zero chemical leaching, and customized branding requirements.
Commercial & Industrial Realities of RPET Manufacturing
Navigating geopolitical regulatory shifts, post-consumer resin (PCR) sourcing volatility, and the industrial engineering shift from single-use plastics to certified multi-use circular vessels.
Stringent Regulatory Compliance
Global consumer markets are undergoing transformative legislative enforcement. Under the EU Packaging and Packaging Waste Regulation (PPWR) and California SB 54, enterprise procurement departments face aggressive mandatory post-consumer recycled content targets (25% to 65% by 2030). Verified food-safe decontamination processes via EFSA and US FDA Non-Objection Letters (NOL) have evolved from optional marketing claims into non-negotiable customs baseline requirements.
Traceability & Feedstock Integrity
Supply chain reliability in recycled polyethylene terephthalate (rPET) depends strictly on source clarity. Industrial converters must counter yellowing degradation, intrinsic viscosity (IV) drop, and volatile chemical contaminants common in unvetted flake lots. Ronchine solves this through end-to-end Global Recycled Standard (GRS 4.0) chain-of-custody protocols, ensuring complete resin traceability back to qualified mechanical recycling stations.
Technical Parity with Virgin Polymers
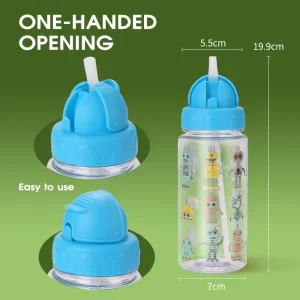
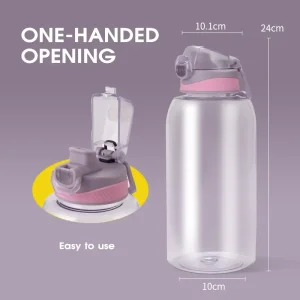
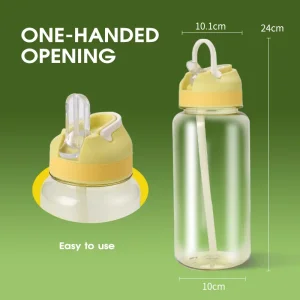
Advanced solid-state polycondensation (SSP) has enabled modern rPET pellets to achieve an Intrinsic Viscosity (IV) rating of 0.80–0.84 dL/g. This mechanical profile allows our blow-molding and injection-molding production lines to output reusable bottles, sports tumblers, and spring-loaded lids exhibiting optical clarity, drop impact resistance, and structural stability indistinguishable from pristine virgin PET resins.
Comparative Performance Matrix: RPET vs. Conventional Resins
Evaluating thermomechanical behavior, recyclability lifecycles, and export safety criteria for enterprise procurement decisions.
| Polymer Classification | Tensile Strength (MPa) | Thermal Deflection (°C) | Food-Contact Export Status | Carbon Cost (kg CO₂/kg) | Lifecycle Circularity |
|---|---|---|---|---|---|
| Post-Consumer RPET (SSP Treated) | 55 – 75 | 65 – 70°C | FDA NOL / EFSA Compliant | ~0.45 – 0.65 | High Closed-Loop Recyclability |
| Virgin Polypropylene (PP) | 30 – 40 | 100 – 110°C | Standard Food Contact | ~1.95 – 2.10 | Downcycled Mechanically |
| Acrylonitrile Styrene (AS / SAN) | 60 – 80 | 85 – 95°C | Cold Liquids Only | ~2.60 – 3.10 | Low Industrial Reclamation |
| Tritan™ Copolyester | 45 – 60 | 95 – 105°C | BPA/BPS Free Approved | ~3.20 – 4.50 | Specialized Circular Loops |
| Austenitic 304 Stainless Steel | 505 – 520 | 800+°C | Universal Safe Standard | ~4.80 – 6.20 | Infinitely Recyclable |
Localized Industry Scenarios & Market Dynamics
How wholesale OEM custom drinkware bridges regulatory frameworks and consumer behavior across distinct territorial channels.
Corporate ESG & Institutional Supply
Multinational organizations across North America and Western Europe have instituted strict procurement mandates eliminating single-use PET drinkware from campus environments. Our OEM division designs bespoke corporate hydration systems with integrated corporate identity (Pantone matching, silk-screening, and precision laser debossing), providing enterprise ESG directors with audited Scope 3 greenhouse gas avoidance calculations per unit delivered.
Omnichannel Retail & Private Label
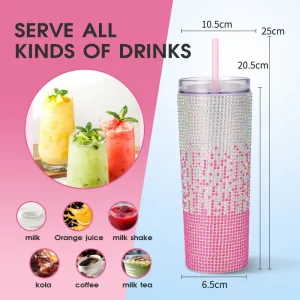
Modern lifestyle retail brands demand visually captivating drinkware that aligns with circular messaging without compromising aesthetic appeal. By combining gradient spray finishes, diamond-cut electroplating, and custom tactile spring-loaded cap mechanisms with food-grade rPET bodies, we deliver off-the-shelf commercial shelf presence engineered to perform both under retail lighting and across digital storefront algorithms.
High-Capacity HoReCa & Theme Parks
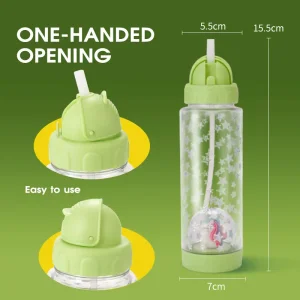
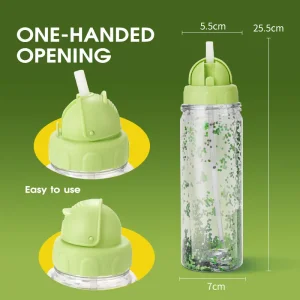
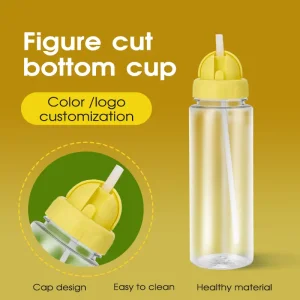
Fast-casual food operators, hospitality networks, and leisure parks are subject to extended producer responsibility (EPR) taxation on disposable packaging. Our multi-use straw-integrated cups, egg-shaped beverage containers, and high-impact helmet caps provide resilient drop resistance, leak-proof mechanical seals, and fully stackable geometry designed for high-turnover dishwashing workflows and commercial reuse cycles.
Technical Roadmap: Next-Gen Circular Manufacturing
Architecting industrial enhancements across raw material refinement, automated tooling, and intelligent quality verification.
Phase 1: Chemical Depolymerization
Expanding direct partnerships with glycolysis and enzymatic degradation facilities to break down post-industrial colored polyester scrap into pure BHET monomers, achieving absolute optical crystal transparency independent of original source color.
Phase 2: Ultra-Lightweighting
Deploying finite element analysis (FEA) to redistribute wall thicknesses across bottle bodies and screw-threads. Achieving 18% polymer mass reduction without sacrificing tensile drop resistance or compressive stacking thresholds.
Phase 3: Digital Product Passports
Integrating non-destructive micro-QR matrixes and NFC tags directly onto container bottoms, enabling automated sorting in European municipal waste streams and verifying real-time supply chain provenance for end consumers.
Phase 4: Mono-Material Caps
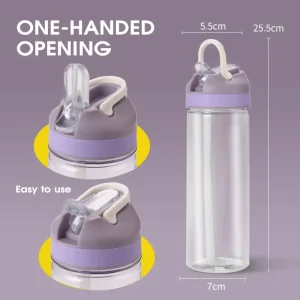
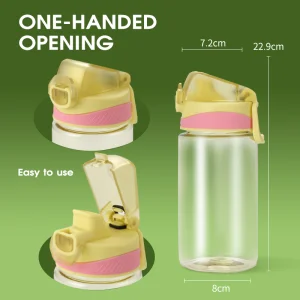
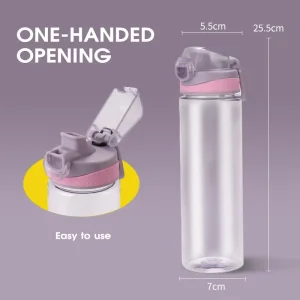
Transitioning spring-loaded and helmet-style closures away from mixed POM/metal spring mechanisms toward high-elasticity single-polymer rPET and rPP living hinges, ensuring 100% recycling without dismantling components.
Macro OEM/ODM Industrial Sourcing Architecture
Mitigating cross-border procurement vulnerabilities through integrated engineering, centralized tooling, and compliance rigor.
Consolidated Manufacturing & Logistics Hub
Operating directly out of Tongqin Industrial Park in Wuyi, Zhejiang, Ronchine leverages a mature industrial cluster dedicated to cup and drinkware fabrication. With immediate proximity to Ningbo and Shanghai maritime ports, container handling cycles, drayage bottlenecks, and customs clearing overheads are reduced by up to 35% compared to inland manufacturing regions.
Total Quality Management & AQL 1.0/2.5
Our quality control regimen integrates automated optoelectronic leak testing, hydraulic internal burst stress checks, high-temperature dishwasher stability cycles, and mechanical torque decay assessments for screw caps. Production batches undergo systematic AQL 1.0 Major / 2.5 Minor visual and dimensional verification before export shipping authorization.
Full-Spectrum Tooling & Surface Customization
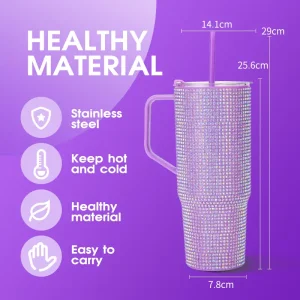
From initial rapid 3D SLA prototyping to 64-cavity high-precision injection molds, our in-house engineering team accommodates custom ergonomic grips, proprietary thread designs, and advanced multi-shot finish treatments. Surface engineering suites encompass automated vacuum electroplating, 360° gradient lacquer spraying, silk-screen and laser printing, and handmade rhinestone drill applications.
Frequently Asked Questions & Technical Inquiries
Essential guidance covering regulatory documentation, MOQ thresholds, mold lifecycle parameters, and material limitations.
How does your factory verify the chemical safety and food-grade compliance of RPET?
What is the standard production lead time and sample turnaround for custom OEM molds?
Can post-consumer RPET achieve identical optical transparency to virgin PET?
What Minimum Order Quantities (MOQs) apply to customized bottle and lid programs?
How do you navigate mechanical durability differences between RPET and Tritan™?
High-Aesthetic Decorative & Functional OEM Drinkware
Combining sustainable composite engineering with premium electroplating, drill stickers, and combo gift set styling.