Featured Precision Post-Consumer PE & Eco drinkware Assemblies
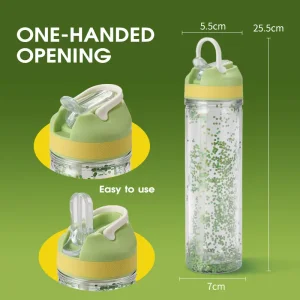
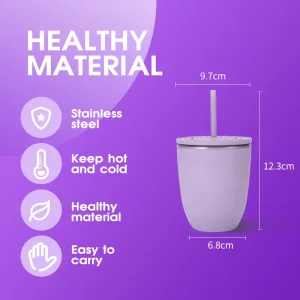
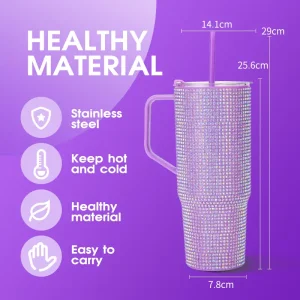
Direct-from-factory high-precision molded caps, thermoformed bodies, and circular polymer consumer units manufactured under stringent quality protocols.
Macro Industry Solutions: Overcoming Polyethylene Downgrading
Addressing mechanical degradation, organic volatiles, and stress-crack vulnerabilities in modern circular supply chains.
In modern industrial polymer recovery, Polyethylene (encompassing High-Density PE, Low-Density PE, and Linear Low-Density PE) presents unique chemical and thermodynamic challenges distinct from polyesters such as PET. While PET recycling relies largely on polycondensation and solid-state polymerization to recover intrinsic viscosity, PE recycling operates within branched and linear polyolefin chains that undergo chain scission and cross-linking during post-consumer thermal cycles.
Industrial brands face substantial structural bottlenecks when integrating high percentages of post-consumer recycled (PCR) PE into complex hardware, such as spring-loaded caps, drinkware lids, ergonomic flasks, and fluid conduits. The primary failure modes include environmental stress cracking (ESCR failure), degraded melt flow indexing (MFI), unstripped volatile organic compounds (VOCs) contributing to flavor transfer, and cross-contamination from polypropylene (PP) fractions. Our state-of-the-art manufacturing infrastructure directly solves these degradation mechanisms through closed-loop automated sorting, deep decontamination, and controlled melt re-stabilization.
Polyolefin Cross-Contamination
Polypropylene and Polyethylene have overlapping densities, making traditional hydro-cyclone sink-float separation inefficient for fine fraction separation, which compromises final tensile strength.
VOC and Odor Entrapment
Fatty acids, surfactant residues, and printing inks migrate deep into the amorphous matrices of PE, leading to persistent off-gassing and organoleptic failure if not stripped at molecular levels.
Thermal Chain Scission
Unstabilized reprocessing yields broad molecular weight distributions and thermal free radicals, radically shortening cycle durability and causing micro-fissuring in pressurized drinkware caps.
Technical Roadmap: Upcycling Chemistry & Processing
How our intelligent recovery lines convert post-consumer bales into high-grade injection engineering polymers.
| Processing Stage | Technological Mechanism | Monitored Tolerances | Output Quality Metric |
|---|---|---|---|
| 1. Hyper-Spectral NIR Sorting | Dual-band Shortwave Infrared (SWIR) spectroscopy separating HDPE, LDPE, PP, and multilayer barriers | Scanning latency < 2ms, Purity tracking | >99.5% Homopolymer Purity |
| 2. Friction Caustic Flotation | High-temperature alkaline dynamic scrubbing stripping water-based and UV curable flexographic inks | pH 11.5–12.5, 85°C thermal threshold | Zero residual surface adhesive agents |
| 3. Vacuum Solid-State Stripping | Multi-zone co-rotating twin-screw devolatilization with ultra-high vacuum extraction zones | Pressure down to < 5 mbar absolute | VOC levels < 0.05 ppm, odor neutral |
| 4. In-Situ Additivation | Compounding with phosphite processing stabilizers, sterically hindered phenols, and long-chain branching agents | MFI adjusted to target ±0.3 g/10min | Superior Environmental Stress Crack Resistance |
| 5. Micro-Laser Filtration | Continuous back-flush screen filtration down to micro-mesh thresholds to eliminate non-melting grit | Continuous melt pressure equilibrium | Zero particulate rupture in thin-wall molds |
Polymer Re-stabilization
By regenerating antioxidant networks within recycled PE, our formulations arrest the thermal oxidation cycle during high-speed injection operations, matching virgin baseline tensile performance.
ESCR Fortification
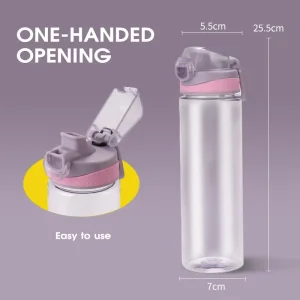
Our engineered blends prevent environmental stress cracking, allowing complex structures like spring-loaded mechanical closures to undergo over 20,000 continuous articulation cycles without micro-fissuring.
Colorimetric Consistency
Automated spectrophotometric tracking homogenizes baseline PCR flakes, providing consistent color fidelity across batch compounding for gradient, macaron, and electroplated exterior finishes.
China Factory 4.0: Supply Chain Resilience & Process Prowess
Wuyi Ronchine Industry & Trade Co., Ltd. (YAMI / Jass Life) bridges raw flake regeneration with finished drinkware mass assembly.
Vertical Upstream-to-Product Synthesis
Located in the heart of Zhejiang’s manufacturing cluster in Tongqin Industrial Park, Wuyi County, our infrastructure short-circuits traditional logistics. We manage resin refining, precision mold design, cleanroom injection, and surface finishing under a single integrated operation.
Micro-Cavity High-Speed Tooling
Our toolrooms build multi-cavity hot-runner molds engineered with sub-micron CNC tolerances. We calculate thermal shrinkage variances inherent to high-content PCR polyethylene, achieving tight dimensional tolerances for high-reliability spring mechanisms.
Deep Strategic Buffer Reserves
Our raw flake and virgin modifier staging silos stabilize input pricing against petrochemical volatility, ensuring long-term contractual pricing stability, predictable landed margins, and steady delivery schedules for our global retail partners.
Compliance Security & Localized Global Operations
Eliminating trade barriers through certified testing, documented chain-of-custody, and rigorous customs management.
Procuring recycled items demands absolute regulatory transparency. Major Western markets penalize ambiguous material lineage through strict EPR frameworks, plastic packaging taxes (such as the UK Plastic Packaging Tax and the EU Packaging Levy), and food-contact compliance audits. Partnering with Wuyi Ronchine guarantees uncompromised institutional security at every border.
Global Recycled Standard (GRS) Traceability
Every metric ton of reprocessed PE and eco-series material is backed by verified transaction certificates (TCs) and clear mass-balance ledgers, establishing defensible corporate sustainability reporting.
Food-Contact Safety Verification
We configure production matrices in full compliance with FDA 21 CFR 177.1520, LFGB, and EU 10/2011, conducting migration threshold tests via accredited third-party labs like SGS, TÜV, and Intertek.
Expedited Port Logistics (Ningbo Hub)
Our direct access to Ningbo and Shanghai ports enables agile container movement, pre-booked vessel allocations, bonded warehousing, and streamlined tariff compliance for volume global shippers.
Frequently Asked Technical & Strategic Inquiries
Clear answers to critical questions on technical specifications, polymer behavior, and procurement workflows.
How do you maintain structural integrity in spring-loaded caps using recycled PE?
What testing methodologies verify that your recycled components are free from VOCs and flavor transfer?
Can post-consumer recycled PE drinkware achieve smooth, high-gloss, or electroplated finishes?
What are the practical minimum order quantities (MOQs) and sampling timeframes for custom-tooled lines?
How do your facilities address corporate ESG mandates and carbon-border tax exposure?
Specialty Drinkware Collections, Closures & Functional Tumblers
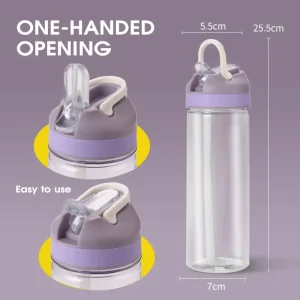
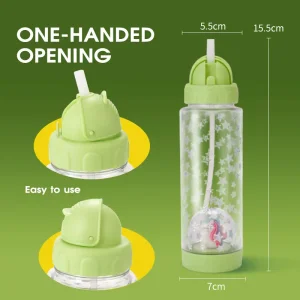
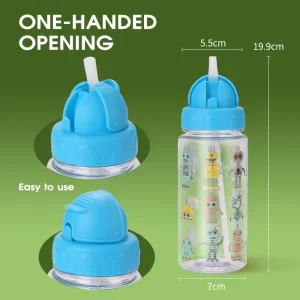
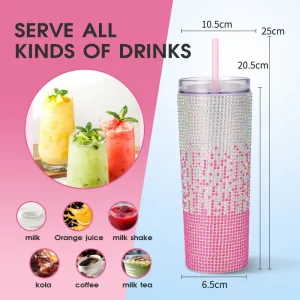
Explore our complete range of drill-sticker items, helmet caps, multi-layer sport bottles, and high-volume combination sets.
Accelerate Your Sustainable Polymer Line
Engage our polymer engineering team today to review your 3D CAD files, formulate custom post-consumer polymer blends, or request a complete OEM factory catalog.