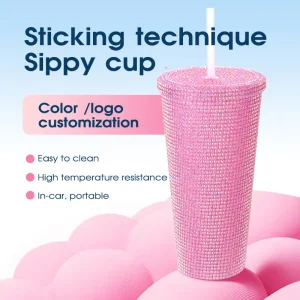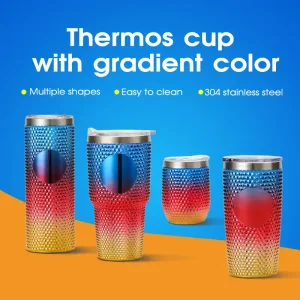
Precision Molded Eco-Tumblers & Spring-Loaded Caps
Explore high-performance eco cups, patented automatic push closures, and custom rhinestone hydration models direct from our ISO-certified Wuyi facility.
The Paradigm Shift: Recycled Cola Coffee Cups in Global Commerce
Analyzing structural industry changes across North America, Europe, and Asia-Pacific driven by EPR mandates, single-use bans, and commercial closed-loop recycling frameworks.
The global drinkware industry is undergoing its most profound structural transformation since the commercialization of consumer polymers. Driven by stringent sustainability legislation, such as the European Union Packaging and Packaging Waste Regulation (PPWR) and state-level minimum post-consumer recycled (PCR) content laws across North America (e.g., California SB 54 and Washington State mandates), global retail brands, quick-service restaurant (QSR) conglomerates, and promotional merchandisers are systematically decommissioning virgin single-use formats. The phrase "Recycled Cola Coffee Cup" has emerged not merely as a marketing nomenclature, but as an engineering classification representing high-clarity, food-contact safe, post-consumer recycled polyethylene terephthalate (RPET) and recycled polypropylene (rPP) extracted from beverage supply streams—most prominently discarded carbonated soft drink bottles—and re-engineered into durable, multi-use, insulated thermal coffee tumblers.
Sourcing from an authentic Chinese tier-one original equipment and original design manufacturer (OEM/ODM) like Wuyi Ronchine Industry & Trade Co., Ltd. (operating YAMI and Jass Life) bridges the gap between ambitious corporate sustainability targets and industrial commercial viability. Producing durable food-grade drinkware from recycled cola resins demands unprecedented mastery over solid-state polycondensation (SSP), intrinsic viscosity (IV) recovery, non-intentional added substances (NIAS) screening, and organoleptic stabilization (eliminating volatile off-gassing and residual taste profiles). Without a specialized manufacturing partner possessing on-site injection lines, in-house tooling workshops, and automated assembly bays, brands face severe exposure to supply volatility, non-compliance fines, and product recall liabilities.
Regulatory Pressure & PPWR
The EU PPWR requires 100% recyclable packaging and mandates minimum PCR quotas (ranging from 10% to 35% by 2030), shifting international retail chains away from single-use cups toward durable, trackable recycled travel tumblers.
- Mandatory recycled content audits
- Extended Producer Responsibility (EPR) fee mitigation
- Elimination of micro-plastic contamination risks
Brand Equity & ESG Valuations
Institutional consumers demand verifiable carbon accounting. Converting a company's coffee tumbler offerings to certified PCR cola plastics delivers measurable Scope 3 emission reductions of up to 67% compared to virgin petrochemical inputs.
- Third-party Global Recycled Standard (GRS) trail
- Documented chain of custody documentation
- Consumer buy-in via verified sustainability metrics
Material Circularity Engineering
Discarded cola bottles provide the highest density of consistent PET polymers. By utilizing mechanical and chemical recovery pathways, our factory re-crystallizes flakes into uniform resins capable of enduring 500+ commercial dishwasher cycles.
- Food-contact EFSA and FDA clearances
- Multi-layer co-injection wall structural barrier
- Superior optical brilliance and drop resistance
Localized Applications & Specialized B2B Usage Scenarios
Custom-engineered form factors tailored for quick-service coffee systems, institutional campus programs, retail private labeling, and high-conversion lifestyle merchandising.
Specialty Coffee & QSR Drive-Thru
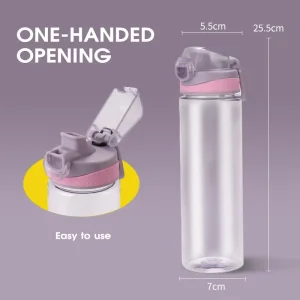
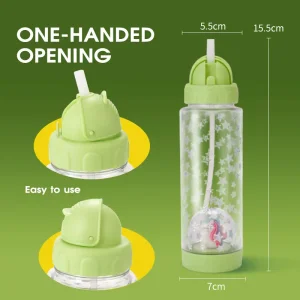
Commercial quick-service drive-thru environments require drinkware that fits standard automotive cup holders, allows rapid one-handed flip-action sipping, and maintains temperature integrity without exterior sweating.
Higher Education & Corporate Campus
Colleges and Fortune 500 campuses across North America and Europe deploy closed-loop hydration programs. These entities replace single-use disposables with branded recycled cola tumblers equipped with RFID tracking tags.
Trendsetter Retail & Glamour Drinkware
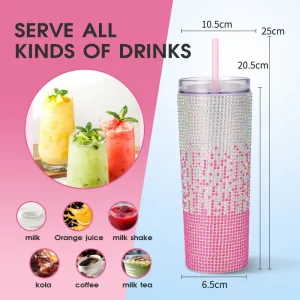
Gen Z and lifestyle retail consumers prioritize visual appeal and collectible identity. The intersection of eco-conscious engineering and viral TikTok aesthetic is where our decorative craft excels.
OEM/ODM Sourcing Directive: When engineering recycled cola coffee tumblers for hot beverage applications (exceeding 85°C / 185°F), RPET single-wall formats must either incorporate an internal food-grade virgin PP or 304 austenitic stainless-steel thermal vessel, or undergo proprietary molecular crystallization. Our engineering team calculates thermal deflection points to ensure the final product meets your exact operational requirements.
Material Engineering & Technical Manufacturing Roadmap
From contaminated post-consumer baled cola bottles to pristine, optical-clarity, food-contact approved reusable drinkware.
Intensive Flake Decontamination
Post-consumer cola bottles undergo friction de-labeling, optical color sorting, caustic washing at 85°C, and vacuum thermal stripping to extract volatile organic compounds (VOCs) and flavor residues.
Solid-State Polycondensation
Decontaminated flakes are fed into an SSP reactor under deep vacuum (less than 1 mbar) at 210°C. This elevates the Intrinsic Viscosity (IV) from 0.65 dl/g to an injection-grade 0.82 dl/g, restoring molecular tensile strength.
A-B-A Co-Injection Molding
Utilizing high-precision multi-cavity hot-runner tooling, the cup body is molded with an A-B-A sandwich architecture: virgin barrier layers (A) encapsulate the 100% recycled PCR cola plastic core (B), eliminating migration risks.
Hermetic Thermal Assembly
Double-wall air-insulated or vacuum-drawn outer shells are ultrasonic-welded or spin-fused to inner liners, followed by leak-integrity testing under 0.05 MPa pressurized air immersion to guarantee a zero-leak seal.
| Polymer / Substrate Class | PCR Content Ratio | Heat Distortion Temp (HDT) | Clarity / Visual Grade | Food-Contact Certifications | Primary Industrial Use-Case |
|---|---|---|---|---|---|
| Post-Consumer RPET (Cola Grade) | Up to 100% | 65°C – 72°C | Exceptional (Glass-Like) | FDA 21 CFR, EU 10/2011, LFGB | Cold brew cups, iced coffee tumblers, fruit-infusion bottles |
| Food-Contact PCR Polypropylene (rPP) | 30% – 100% | 100°C – 120°C | Translucent to Opaque | FDA GRAS, LFGB, REACH SVHC | Hot coffee mugs, spring lids (YS-2432), microwaveable bodies |
| Virgin Tritan™ Copolyester (TX1001) | 0% (Circular ISCC+ opt) | 99°C – 108°C | Diamond Clarity | NSF 51, FDA, LFGB, BPA-Free | Premium shatterproof sports bottles, luxury corporate lines |
| AS (Styrene-Acrylonitrile) | 0% – 20% | 75°C – 85°C | High Gloss Clarity | FDA Compliant (Cold only) | Double-wall studded tumblers, rhinestone drill stickered cups |
| Dual-Wall 304 Stainless Core + RPET Shell | Composite (Eco hybrid) | Exceeds 100°C (Boiling) | Opaque metallic inner | FDA, LFGB, DGCCRF | Stanley-style travel mugs, all-day thermal retention vessels |
China Factory Advantage: Supply Chain Resilience in Zhejiang
Why the Jinhua-Wuyi manufacturing cluster remains the world’s undisputed epicenter for cost efficiency, rapid tooling, and high-volume drinkware exports.
Unmatched Industrial Agglomeration
Wuyi County and surrounding Jinhua/Yongkang form the globally renowned "Hardware and Cup Capital". Within a 30-kilometer radius, our factory accesses precision mold fabrication houses, silicone vulcanization facilities, high-grade colorant masterbatch developers, and automated packaging plants.
In-House Tooling & Mold Mastery
Owning our mold workshops allows Wuyi Ronchine to turn customer 3D concepts into working production tools in 14 to 25 days. Our multi-cavity molds are engineered from hardened H13 and S136 stainless steel, delivering dimensional tolerances within ±0.02 mm.
Logistical Proximity to Ningbo Port
Our Tongqin Industrial Park operations are located near Ningbo-Zhoushan Port—the world’s largest port by cargo throughput—and Shanghai Port. This positioning enables real-time container dispatch, reduced drayage expenses, and seamless customs export execution.
Global Compliance, Quality Control & Food-Safety Protocol
Ensuring zero migration of contaminants, non-intentional added substances (NIAS), or heavy metals through accredited third-party laboratory verifications.
Food Contact Regulations: FDA, LFGB, & EU 10/2011
Recycled plastics intended for food and beverage contact are subject to stringent regulatory scrutiny worldwide. In the United States, PCR resins must possess an FDA No Objection Letter (NOL) confirming the recycling process effectively decontaminates post-consumer polymers to food-grade purity.
In the European Union, compliance with Commission Regulation (EU) 2022/1616 on recycled plastic materials and articles intended to come into contact with foods is mandatory. Our products undergo rigorous overall migration limit (OML) and specific migration limit (SML) testing using simulant fluids (3% acetic acid, 50% ethanol, and olive oil/Tenax) to verify zero transfer of toxic substances into coffee and cold beverages.
GRS Chain of Custody & Factory Auditing
Greenwashing concerns make verifiable provenance essential. Through the Global Recycled Standard (GRS), we track raw materials from post-consumer collection stations through flake conversion, compounding, molding, and packing.
For every bulk commercial delivery, we can provide authentic Transaction Certificates (TC) certifying the exact percentage of post-consumer cola bottle content utilized. Furthermore, our production facilities undergo regular independent social, environmental, and quality audits under ISO 9001 and ISO 14001 standards, ensuring our factory passes the strict vendor qualification scorecards of multinational enterprise buyers.
Factory Testing Laboratory Capabilities: Our on-site quality assurance lab subjects every production run to rigorous mechanical testing: vertical drop testing from 1.2 meters at full fluid capacity, automated lid open/close fatigue testing up to 20,000 continuous cycles, thermal shock exposure from -20°C to 100°C, and dishwasher adhesion peel tests for custom logos and electroplated finishes.
End-to-End OEM/ODM Procurement Workflow
A systematic, transparent process engineered to minimize risk, protect intellectual property, and deliver retail-ready custom drinkware on schedule.
Step 1: Specification Briefing
Buyer establishes target capacity, temperature usage (cold brew vs. boiling), PCR ratio requirements, Pantone colors, and decoration specifications (rhinestone, electroplate, silk screen, heat transfer, or UV print).
Step 2: Prototyping & Mold CAD
Our engineering division delivers 3D digital renderings within 48 hours. Following CAD sign-off, high-precision stereolithography (SLA) resin prototypes are generated for tactile ergonomic and volume confirmation.
Step 3: Tooling & Pilot Batch
Steel mold tooling is completed within 15-25 days. An initial T1 sample run is inspected for gate vestige, sink marks, wall thickness parity, and thermal seal integrity, then dispatched to the buyer for final approval.
Step 4: Mass Production & QC
Automated injection lines produce the order under ISO 9001 quality controls. In-line AQL 1.0/2.5 inspections are conducted, followed by final custom packaging, barcode labeling, pallet wrapping, and container dispatch.
Frequently Asked Questions for Sourcing Directors & Importers
Detailed engineering, regulatory, logistical, and commercial answers to resolve technical queries prior to formal quotation and mold sign-off.
What specific materials constitute a "Recycled Cola Coffee Cup", and how do you ensure food safety?
To ensure absolute safety, the collected flakes undergo caustic washing, high-temperature vacuum decontamination, and solid-state polycondensation (SSP). This process removes volatile compounds and restores the polymer chain length. For cups holding hot liquids above 80°C, we either utilize an A-B-A co-injection barrier (encapsulating the recycled material between virgin food-grade contact layers) or pair a certified RPET outer decorative shell with an inner liner made from 304 food-grade stainless steel or food-grade virgin PP. Every batch is certified free of BPA, phthalates, and heavy metals.
How do you eliminate residual odor or flavor transfer in recycled plastic drinkware?
- High-Temperature Stripping: Polymer flakes are subjected to hot-air circulation and deep-vacuum desiccation at temperatures exceeding 200°C, volatilizing residual flavor compounds.
- Solid-State Polycondensation: The vacuum SSP reactor removes trace contaminants down to parts-per-billion (ppb) thresholds, meeting FDA NOL standards.
- Organoleptic Sensory Testing: Randomly selected molded samples are filled with boiling deionized water and stored at 40°C for 24 hours. A certified testing panel then confirms zero organoleptic taint before mass production begins.
What third-party certifications and traceability documentation are provided with bulk shipments?
- North America: FDA 21 CFR 177.1630 (PET) / 177.1520 (PP) migration compliance reports, California Proposition 65 test certificates, and BPA-free lab reports from SGS, TÜV, or Intertek.
- European Union: Commission Regulation (EU) 10/2011, German LFGB food contact certificates, and REACH SVHC declarations.
- Traceability & Provenance: Global Recycled Standard (GRS) Transaction Certificates (TC) issued by accredited bodies (such as Control Union), tracking the material from recycling facility to final finished cartons.
What are your Minimum Order Quantities (MOQ) and lead times for custom tooling vs. existing molds?
- Existing Factory Molds with Custom Branding: For existing models in our catalog (such as the YS-2432 spring-loaded cap or YS-004 drill sticker straw cups), the standard MOQ is 1,000 to 3,000 units per colorway. Custom logo printing (silk screen, heat transfer, or UV print) and custom Pantone matching are available. Production lead time is typically 20 to 30 days after sample sign-off.
- Fully Custom OEM/ODM Tooling: For proprietary shapes, unique capacities, or patented closure mechanisms, the tooling MOQ is generally 10,000 to 20,000 units. Mold construction takes 15 to 25 days, with T1 pilot samples delivered within 7 days of tooling completion. Mass production follows in 30 to 40 days.
Can recycled cola cups withstand high temperatures and commercial dishwasher cleaning?
- Single-Wall RPET: Engineered primarily for iced coffee, cold brew, and room-temperature beverages. Maximum continuous liquid temperature should not exceed 65°C (149°F). Recommended for hand washing.
- Food-Contact PCR PP (rPP): Suitable for hot coffee, tea, and warm beverages up to 100°C–110°C (212°F–230°F). Fully safe for top-rack commercial dishwashers.
- Composite Dual-Wall Construction: Features a post-consumer recycled cola plastic outer shell paired with a 304 food-grade stainless steel or virgin PP inner liner. This architecture supports boiling water (100°C) without structural deflection or heat transfer to the user's hand, while retaining temperature for hours.
How does Wuyi Ronchine support international buyers with direct factory communication?
High-Conversion Decorative & Multi-Compartment Drinkware
Explore custom rhinestone sets, multi-functional gift bundles, electroplated finishes, and lightweight eco-caps engineered for global commercial distribution.