Primary Technical Components & Eco Hardware Solutions
Direct factory production lines integrating sustainable raw materials, ultra-precision sealing caps, and reinforced hardware engineered for heavy-duty outdoor and shelter applications.
Macro-Industry Solutions in Recycled Nylon Tent Engineering
Decarbonizing high-performance outdoor shelters requires moving past superficial recycling claims to establish true chemical depolymerization, rigorous closed-loop post-consumer recovery, and verified environmental accounting.
Post-Consumer Ocean & Industrial Waste Regeneration
China's state-of-the-art synthetic textile mills utilize recovered marine fishing nets, monofilament discards, and post-industrial spinning waste to produce virgin-grade recycled Polyamide 6 (rPA6) and 6.6 (rPA66). By reversing polymerization down to caprolactam monomers, the molecular chain length is renewed without thermal degradation.
Non-Fluorinated PFAS/PFC-Free Hydrophobic Membranes
Meeting strict EPA and EU zero-discharge regulations, our factories transition tent flies and shelter floors to advanced fluorine-free durable water repellent (C0 DWR) coatings. Paired with non-porous recycled polyurethane (rPU) and silicone elastomeric backings, this achieves hydrostatic head ratings surpassing 3,000mm to 10,000mm.
Full Monomaterial Circular Architecture
Conventional tents blend polyester flies, nylon tubs, PVC windows, and composite poles, making post-life recycling impossible. Our advanced manufacturing consortium pioneered 100% all-polyamide modular tent assemblies, utilizing recycled nylon for the canopy, mesh vents, seam binding tape, zippers, and reinforced guyline anchors.
Global Commercial Dynamics & Polymer Selection Architecture
International outdoor gear procurement is undergoing a paradigm shift driven by EU Corporate Sustainability Due Diligence (CSDDD), extended producer responsibility (EPR) mandates, and soaring consumer demand for carbon-audited equipment.
Mechanical vs. Chemical Recycling Realities
While mechanical shredding and melt-extrusion work for PET bottles, recycled nylon suffers from rapid thermal oxidative degradation and melt flow index (MFI) variance. Leading Chinese chemical plants utilize supercritical fluid depolymerization to synthesize recycled caprolactam with mechanical properties equivalent to petroleum-derived virgin resins.
High-Tenacity Denier Optimization (10D–70D)
Ultra-light backpacking canopies require fine-denier yarn (10D to 20D micro-ripstop) with high tenacity (≥7.5 g/denier). Overcoming lower molecular uniformity in secondary polymers requires strict molten filtration and vacuum solid-state polymerization (SSP) processes.
EU Product Environmental Footprint (PEF)
By enforcing full Life Cycle Assessments (LCA) from cradle to gate, Chinese supply chains offer verified Environmental Product Declarations (EPD). Brand clients gain ISO 14040/44 audited datasets showcasing substantial savings in primary energy demand (PED) and embodied carbon.
| Material Engineering Grade | Primary Feedstock Source | Tensile Strength (MPa) | Water Column (mm H₂O) | Embodied CO₂ (kg/kg) | Commercial Compliance Target |
|---|---|---|---|---|---|
| Chemically Regenerated rPA6 | Ocean Ghost Nets & Industrial Monofilament | 82 - 90 MPa | 3,000 - 5,000 mm (Sil/PU) | 2.15 kg CO₂e | GRS / bluesign® / EU Ecolabel |
| Post-Industrial Virgin-Blend PA66 | Yarn Extrusion & Airbag Salvage | 95 - 110 MPa | 5,000 - 10,000 mm (Multi-coat) | 3.40 kg CO₂e | ISO 14025 EPD / OEKO-TEX |
| Standard Mechanical rPET (Reference) | Clear Post-Consumer Beverage Bottles | 55 - 65 MPa | 1,500 - 3,000 mm (PU) | 1.80 kg CO₂e | General Consumer Grade |
| Traditional Virgin PA6 (Baseline) | Crude Oil Benzene-Cumene Cracking | 85 - 92 MPa | 3,000 - 5,000 mm (C6 DWR) | 6.85 kg CO₂e | Legacy Standard Non-Circular |
Institutional Quality Assurance & Export Compliance
International outdoor tent procurement demands verified compliance. Our facilities operate within audited chemical, structural, and social responsibility governance systems.
Global Recycled Standard (GRS 4.0)
Chain of Custody (Transaction Certificates - TC) issued batch by batch, verifying raw materials from input collection to final yarn spinning, weaving, and shelter fabrication.
EN ISO 5912 & CPAI-84 Structural Standards
Exhaustive testing for storm resilience, wind stability (wind tunnels up to 120 km/h), rain chamber water penetration, and CPAI-84 / ISO 6941 flame-retardant performance without toxic halogenated chemicals.
REACH Annex XVII & California Prop 65
Exhaustive mass spectrometry testing verifying absolute non-detection of perfluoroalkyl substances (PFOS/PFOA/PFHxA), heavy metal mordants, organotin compounds, and phthalate plasticizers.
Factory Audits: BSCI & SMETA 4-Pillar
Tier-1 manufacturing compliance assuring ethical manufacturing, safe working conditions, environmental water effluent management (ZDHC level 3), and fair labor practices.
Engineered Applications: From Sub-Zero Alpine to Tactical Tents
Recycled nylon formulations must be tuned to the specific physical, thermal, and mechanical stresses of target end-use environments.
Ultralight Backpacking & Thru-Hiking
Targeting weight-obsessed markets, our factories utilize 15D rPA6 ripstop silnylon weighing under 38 g/m². Dual silicone immersion coating prevents moisture absorption and maintains high elasticity under shifting thermal gradients.
Four-Season Alpine & Expedition Geodesic Shelters
Built using high-tenacity 40D/70D recycled nylon 6.6 with multi-layer cold-crack-resistant PU formulations, rated down to -40°C. Engineered to withstand heavy snow loading and hurricane-force alpine winds without catastrophic fabric sheer.
Modular Luxury Glamping & Eco-Resorts
Heavy-weight (210D to 420D) textured recycled Oxford nylon with durable matte finishes, offering superior UV 50+ solar block, anti-mildew antimicrobial coatings, and architectural-grade breathability.
Disaster Relief & Tactical Deployments
Rapid-deployment tactical shelters with near-infrared (NIR) spectral reflectance camouflaging, fire retardancy conforming to NFPA 701, and long-term UV-stabilized recycled polymer weaves designed for multi-month field operations.
Advanced Technology Roadmap & Future Outlook
Leading Chinese tent manufacturers are investing in next-generation material science to solve nylon's historical hydro-expansion vulnerabilities and enhance circularity.
01
Solvent-Free Plasma Hydrophobic Surface Grafting
Moving beyond liquid chemical dips, next-generation lines employ cold atmospheric plasma polymerization. Nanoscale silicon compounds are cross-linked directly to the outer surface of recycled polyamide fibers, yielding exceptional water contact angles (>130°) with zero chemical run-off and reduced processing water demand.
02
Bio-Attributed Mass Balance & Enzymatic Depolymerization
Integrating bio-attributed monomers derived from non-food castor oil feedstocks (bio-PA410/bio-PA610) with chemically regenerated post-consumer polyamide. Biological enzymatic depolymerization breaks down low-grade discarded shelter fabrics under low heat and neutral pH, producing pure monomers with minimal energetic burden.
03
AI-Assisted Ultrasonic Micro-Seam Bonding & Smart Traceability
Replacing polyurethane seam-sealing tapes—the primary failure point in recycled tents—with automated ultrasonic fusion welding. This bonds monomaterial fabrics together at the molecular level, creating weld seams that are stronger than the base fabric and eliminating delamination. Embedded RFID/QR thread weaves support lifetime digital product passports (DPP).
Frequently Asked Technical & Sourcing Questions
Direct answers to core queries regarding recycled nylon tent design, minimum order volumes, material performance metrics, and testing certifications.
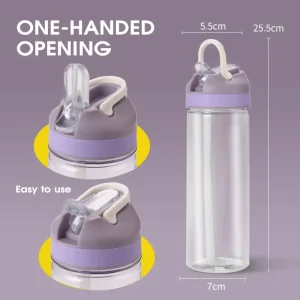
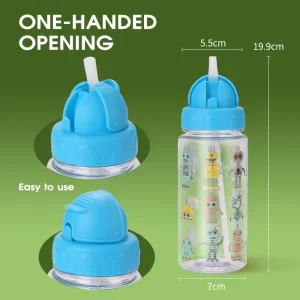
High-Efficiency Outdoor & Hydration Accessories
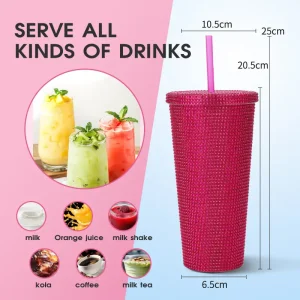
Expanding circular factory integration with eco-engineered spring-loaded caps, drinkware components, and specialized protective fittings supporting your brand's accessories lineup.