Featured Manufacturing Lineup: Precision Injection & Foam Innovations
Explore our flagship high-performance injection tooling, vacuum insulation drinkware, and sustainable co-molded polymer solutions direct from our modern Zhejiang manufacturing facilities.
The Paradigm Shift in Balance & Proprioceptive Equipment Sourcing
As health clubs, physical therapy chains, and consumer fitness lifestyle brands navigate tightening Scope 3 carbon mandates and extended producer responsibility (EPR) legislation, the market demand for yoga balance pads has shifted radically from disposable, virgin petrochemical foams to fully traceable, closed-cell circular elastomers.
The Demise of Virgin PVC & XLPE
Traditional balance pads manufactured from cross-linked polyethylene (XLPE) or chlorinated polyvinyl chloride (PVC) are facing systemic phase-outs across tier-1 European and North American retail networks. Non-recyclable thermoset cross-linking structures and lingering chlorinated plasticizers create severe disposal liabilities, toxic combustion off-gassing, and elevated VOC emissions that fail green public procurement (GPP) audits.
Proprioceptive Hysteresis Demands
Unlike ordinary static yoga mats, a professional yoga balance pad serves as an unstable kinematic platform. It requires precise viscoelastic hysteresis: enough dynamic deformation to trigger continuous sensorimotor feedback (muscle spindle and Golgi tendon organ activation), paired with instant elastic rebound that prevents total mechanical bottoming-out under heavy localized loads (up to 150 kg).
Global ESG Sourcing Mandates
Enterprise procurement departments at major sports conglomerates, corporate health providers, and boutique rehabilitation chains now demand validated circularity. Certified Global Recycled Standard (GRS v4.0) chain of custody, third-party Life Cycle Assessments (LCA), and verified cradle-to-gate carbon savings of >45% are non-negotiable prerequisites for primary vendor qualification.
Engineering Circular Closed-Cell Elastomer Matrices
The challenge of manufacturing high-density balance pads from post-consumer (PCR) and post-industrial (PIR) polymer waste lies in molecular weight degradation. Learn how our polymer engineers solve mechanical shear degradation through advanced block-copolymer grafting.
Polyolefin Elastomer (POE) Core Grafting
Recycled EVA and TPE feedstocks undergo secondary transesterification and compatibilization with maleic anhydride-grafted polyolefin elastomers (POE-g-MAH). This restores molecular entanglement across phase boundaries, dramatically reducing tear propagation and guaranteeing dynamic elastic recovery even after tens of thousands of intense loading cycles.
Supercritical N₂ & CO₂ Microcellular Foaming
By transitioning from chemical azodicarbonamide (ADC) blowing agents to supercritical physical foaming (sc-CO₂ and sc-N₂), our facility produces closed-cell pore structures with diameter tolerances constrained between 25 and 45 microns. This eliminates formamide odor, removes heavy metal residues, and forms an impervious, impermeable skin layer that repels sweat, moisture, and microbial colonies.
| Performance Characteristic | Test Standard | Virgin High-End EVA | Standard Recycled Pad | Our Advanced Circular Matrix (Factory 4.0) |
|---|---|---|---|---|
| Shore C Durometer Hardness | ASTM D2240 | 35° ± 3° | 28° ± 5° (Inconsistent) | 36° ± 2° (Precision Homogeneity) |
| Compression Set (22h @ 50°C, 50% Deflection) | ASTM D395 Method B | 18.4% | 34.2% (Rapid Collapse) | 14.1% (Superior Dynamic Resilience) |
| Tensile Strength (MPa) | ASTM D412 | 1.85 MPa | 1.10 MPa | 2.15 MPa (Molecularly Re-Engineered) |
| Dynamic Slip Resistance (Dry/Wet) | DIN 51130 | R10 | R9 (Prone to slipping) | R11+ (Laser Micro-Textured Prism Skin) |
| VOC & Formamide Content | EN 71-3 / REACH SVHC | < 200 mg/kg | > 500 mg/kg (Pungent) | Non-Detectable / Zero Residue |
| Traceable Recycled Polymer Content | GRS Scope Certificate | 0% | 15% - 25% (Unverified) | 65% - 100% Certified Post-Industrial/Consumer |
China Factory 4.0: Automated Precision & Coastal Resilience
Operating from the epicenters of precision polymer processing in Wuyi and Jinhua, Zhejiang, our production lines combine algorithmic digital control with deep local supply cluster economies. Here is how our automated plant de-risks global brand supply chains.
Automated Continuous Compounding
Volumetric blending is obsolete. Our lines employ 16-channel gravimetric loss-in-weight feeders that dynamically synchronize PCR polymer granules, elastomeric modifiers, and bio-based non-phthalate pigments. Real-time ultrasonic melt-flow sensors eliminate batch-to-batch density variance, guaranteeing consistent tactile firmness across millions of units.
High-Tonnage Multi-Cavity Tooling
Our press rooms leverage 1,200-ton CNC thermo-compression molding presses outfitted with multi-cavity vacuum-assisted tool steel dies. Integrated conformal cooling channels reduce thermal stabilization cycles by 38%, preventing edge shrinkage and warpage while yielding an immaculate 500mm x 400mm x 60mm dimensional envelope.
Port-Centric Logistics Cluster
Located within immediate trucking corridors to Ningbo-Zhoushan and Shanghai international container ports, our hub minimizes domestic drayage expenses and intermodal delays. Automated carton-palletizing robotics maximize container cubic volume utilization by 18%, sharply lowering landed unit freight costs for overseas importers.
Engineered for Human Movement, Clinical Care & Ergonomics
Yoga balance pads are no longer confined to casual stretching. Our specialized durometer ranges (25 Shore C to 50 Shore C) cater to targeted commercial domains across athletic performance and musculoskeletal rehabilitation.
Clinical Neuro-Rehabilitation
Crucial for post-operative ACL reconstruction, chronic ankle instability rehab, and stroke gait re-education. Soft-response formulation (28° Shore C) forces rapid micro-adjustments in deep stabilizers without straining weakened ligaments.
Athletic Kinetic Conditioning
Used by elite sports academies for plyometric prep and single-leg deceleration drills. The dual-density hybrid pad absorbs explosive impact vectors while activating dormant intrinsic foot muscles and peroneal stabilizing chains.
Mind-Body & Studio Pilates
Delivers targeted joint cushioning during kneeling postures (Camel, Low Lunge) and seated spinal articulation. The textured, skin-friendly anti-slip surface guarantees zero tactile slippage during heavy thermal yoga sweat sessions.
Ergonomic Standing Stations
Integrated into forward-thinking corporate workplaces as active standing desk mats. Encourages subtle plantar muscle firing that stimulates venous blood return, alleviating lumbar spinal compression during long working hours.
From Polymer Pellet to Global Retail Container
Our standardized OEM/ODM engineering workflow reduces design-to-production cycles down to 25 business days, guaranteeing complete batch reproducibility and auditable GRS chain of custody.
Polymer Formulation & Compounding
High-grade PIR/PCR polymer chips are dried, magnetically scrubbed of impurities, and compounded with custom POE elastomeric stabilizers and non-toxic mineral blowing concentrates.
Precision Tooling & Mold Machining
In-house 5-axis CNC vertical machining centers cut aircraft-grade aluminum mold blanks with laser-textured traction topographies, eliminating manual mold release coatings.
High-Pressure Supercritical Expansion
Automated compression presses heat the compound under 180°C at 15 MPa. Supercritical nitrogen gas induces clean cell nucleations, causing instantaneous elastic expansion upon mold de-clamping.
Robotic Trimming & Thermal Beveling
6-axis robotic arms guide ultra-high-pressure cold water-jets to trim peripheral flashing, followed by high-speed thermal beveling heads to create ergonomic, splinter-free perimeter edges.
Laser Surface Branding & UV Curing
Custom private label logos, alignment crosshairs, and functional graphic grids are applied via non-contact CO₂ laser etching or high-adhesion, eco-certified UV-cured flexible inks.
AQL 1.0 Laboratory Quality Release
Batches are pulled for strict durometer testing, 100,000-cycle cyclic fatigue compression, tear-shear assessment, chemical migration screening, and barcoded FSC carton packout.
Frequently Asked Questions for B2B Sourcing Directors
Get immediate, technically rigorous answers regarding compliance certificates, custom tool amortizations, MOQ structures, and ocean freight logistics directly from our factory engineering desk.
How is the exact percentage of recycled polymer certified and audited?
Every batch of our recycled yoga balance pads is accompanied by official Global Recycled Standard (GRS v4.0) Transaction Certificates (TCs). These documents trace the polymer provenance directly from certified recycling compounders through our manufacturing plants, auditing exact input-to-output mass balances in accordance with ISO 14021 Environmental Claims guidelines.
Do recycled pads suffer from chemical odor or high formamide levels?
No. Conventional low-cost EVA pads smell strongly due to azodicarbonamide (ADC) thermal decomposition yielding formamide and ammonia gas. Our supercritical physical foaming process (sc-CO₂/sc-N₂) operates completely free of ADC chemical foaming agents, guaranteeing non-detectable formamide levels (<5 mg/kg) under rigorous French Décret n° 2010-1664 and EU REACH standards.
What is the minimum order quantity (MOQ) for custom Pantone and branding?
For standard baseline colorways using our existing mold dimensions (e.g., 400x330x50mm, 500x400x60mm), our flexible MOQ begins at 500 units per color. For entirely custom custom-molded sizes, bespoke textured surface dies, or dual-density co-molded laminations, the MOQ is 1,000 units, with initial mold engineering tooling amortized across the opening production run.
How do recycled balance pads perform under prolonged cyclic compression?
Thanks to our proprietary POE elastomer grafting, our circular balance pads outperform lower-grade virgin EVA. In standardized ASTM D395 compression set testing (22 hours under 50% deflection at 50°C), our material rebounds with less than 14.5% permanent deformation, ensuring that pads in high-traffic commercial gym or clinic environments maintain their kinematic instability for years.
What surface textures are available for maximum anti-slip traction?
We supply three standard laser-machined traction patterns: micro-hexagonal honeycomb, inverted diamond prism, and organic fine-leather grain. Each pattern is engineered directly into the steel mold cavity to prevent sweat accumulation via capillary micro-channels, achieving a high wet slip resistance rating of R11 according to DIN 51130.
What is the typical sampling and mass production lead time?
Rapid 3D CAD modeling and custom color lab dips are delivered within 3 to 5 business days. Rapid physical prototyping via CNC foam slicing takes 7 business days. Full tooling for custom compression molds takes 15 calendar days. Mass contract production runs are completed within 20 to 30 days post-sample approval, supported by rolling ocean container vessel bookings from Ningbo Port.
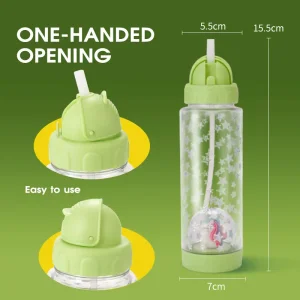
Extended Drinkware & Eco Series Precision Manufacturing
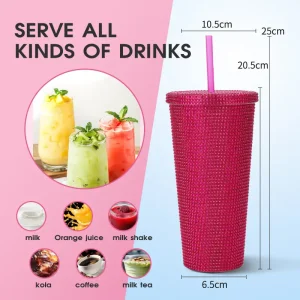
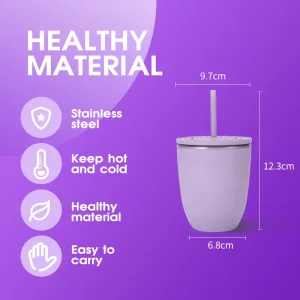
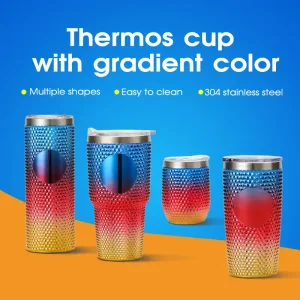
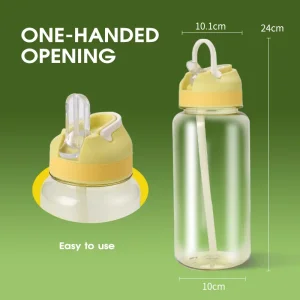
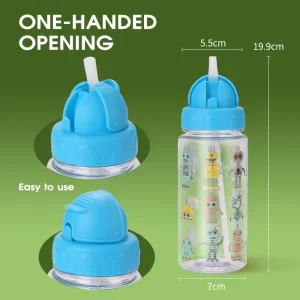
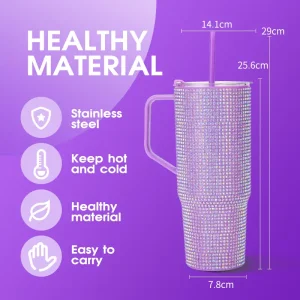
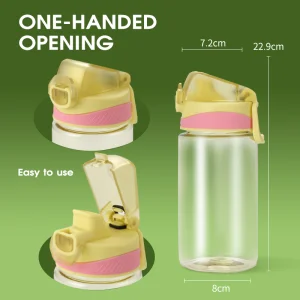
Review additional models from our multi-line manufacturing facilities in Wuyi, Zhejiang. All models offer comprehensive OEM/ODM customization, private label branding, and food-grade/consumer-safe certifications.
Accelerate Your Circular Product Strategy with Factory Direct Control
Whether you require GRS-certified recycled material documentation, custom 3D mold tooling development, or a full factory video audit of our Wuyi production lines, our bilingual engineering team is at your service.