Next-Generation Circular Drinkware Systems
China RPET Cup Recycle Manufacturers & Suppliers
Industrial-grade food contact RPET thermoforming, closed-loop post-consumer resin engineering, and certified sustainable manufacturing for global wholesale volume distributors.
Precision Engineering · Production Series A
Featured Recycled Polymer & Eco Lid Solutions
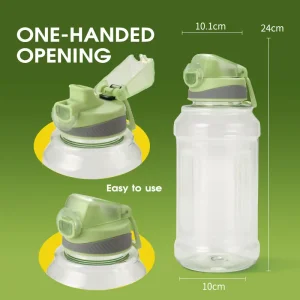
Direct OEM/ODM catalog selections produced in our Zhejiang facility, featuring spring-loaded automation, diamond electroplating accents, and food-grade recycled resins.
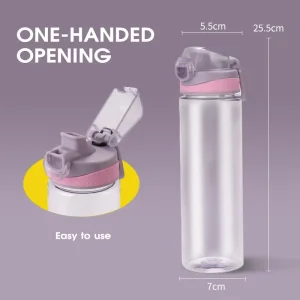
China Eco - Spring Loaded Cap YS-2432
Inquire Specifications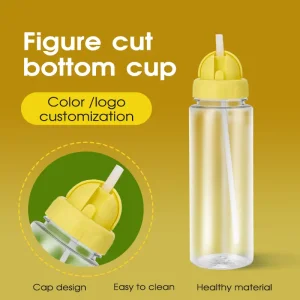
China Eco - Helmet Cap YS-2314B
Inquire Specifications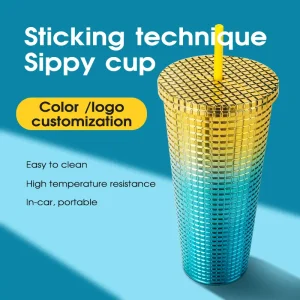
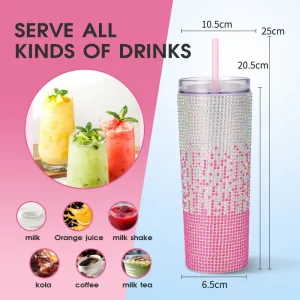
Wholesale Straw Cup - Grid Electroplating
Inquire Specifications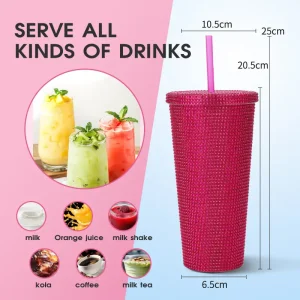
Wholesale Drill Sticker - Straw Cup YS-004
Inquire Specifications
China Combination - 3-in-1 Set Dol
Inquire Specifications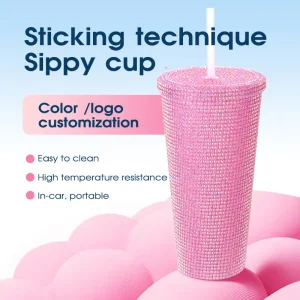
China Straw Cup - Drill Sticker Line
Inquire Specifications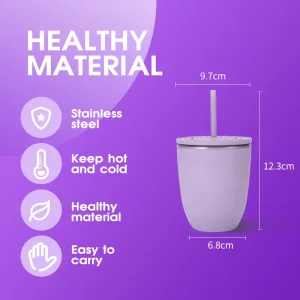
Wholesale Straw Cup Egg-Shaped YS-188
Inquire Specifications
Industry Macro Intelligence
The Paradigm Shift in Recycled RPET Cup Manufacturing
As regulatory pressures such as the EU Packaging and Packaging Waste Regulation (PPWR) and US State-level Extended Producer Responsibility (EPR) mandates tighten, wholesale drinkware sourcing faces an structural turning point.
The Post-Consumer Resin (PCR) Hurdle
Traditional RPET processing suffered from thermal degradation, intrinsic viscosity (IV) drop, and acetaldehyde contamination, rendering cups yellowed or brittle. Ronchine's advanced solid-state polycondensation (SSP) remediation maintains target IV levels between 0.80 and 0.84 dL/g.
This technical threshold gives thin-walled thermoformed and injection-molded cups shatter resistance, crystal-clear optical clarity, and uniform rim bead retention comparable to virgin polymers.
Multi-Tier Closed Loop Decontamination
Mechanical recycling requires multi-stage optical sorting (NIR spectroscopy) to remove non-PET polymers down to parts-per-million levels. Washed flakes undergo dynamic high-vacuum thermal treatment, volatizing organic solvents and migration molecules.
This achieves non-detectable non-intentionally added substances (NIAS), enabling compliance with international safety protocols without relying on toxic virgin stabilizing additives.
Decarbonization at Global Scale
Life Cycle Assessments (LCA) demonstrate that switching from petroleum-based virgin PET to certified recycled RPET reduces greenhouse gas emissions by up to 67%. Supply chain decarbonization is no longer a corporate talking point—it's tied to import tariffs and packaging taxes.
We provide buyers with end-to-end carbon accounting data, streamlining ESG disclosure reporting for retailers and major international supply chains.
Material Performance & Integrity
RPET Engineering Parameters vs. Competitive Polymers
Choosing the correct polymer matrix determines operational shelf life, structural drop impact limits, and chemical barrier properties across cold beverage systems.
100%
Traceable Post-Consumer PCR
0.82
Target Intrinsic Viscosity (dL/g)
< 1.0
Acetaldehyde Residual (ppm)
-20 to 65
Thermal Threshold Range (°C)
| Polymer Designation | Tensile Strength (MPa) | Haze Value (%) | CO2 / O2 Barrier Index | Circular Recyclability Index | Primary Industrial Use Case |
|---|---|---|---|---|---|
| Ronchine High-Purity RPET | 58 - 65 | < 2.2% (Super Clear) | High (Optimal gas barrier) | Class 1 Closed Loop (GRS) | Cold brew cups, iced beverage tumblers, retail display cups |
| Virgin Polypropylene (PP) | 30 - 38 | 8.0 - 15.0% (Translucent) | Moderate (Moisture resistant) | Downcycled mechanically | Hot drink lids, soup containers, flexible straw sets |
| Polylactic Acid (PLA) | 45 - 55 | 3.0 - 4.5% (Clear) | Low (Sensitive to moisture) | Industrial Composting Only | Biodegradable promotional events (limited shelf life) |
| Virgin AS / SAN Resin | 65 - 72 | < 1.5% (Glass-like) | High (Rigid structure) | Low (Difficult stream) | Double-wall tumblers, electroplated luxury giftware |
Audit Protocols & Regulatory Defensibility
Comprehensive Global Compliance & Traceability
Importing recycled food contact items into North America, the European Union, and Asia-Pacific territories requires verifiable, multi-point chemical testing and unbroken chain-of-custody documentation.
FDA 21 CFR 177.1630 & NOL
Our RPET resin source systems are supported by US FDA No Objection Letters (NOL) verifying decontamination efficiency for conditions of use E through G, enabling compliant distribution across all US states.
EFSA & EU Regulation 2022/1616
Complying with the latest European Commission criteria for recycled plastics in food contact, we document batch challenge tests and migration testing verified by accredited laboratories (SGS, TÜV, Intertek).
GRS (Global Recycled Standard)
We provide complete transaction certificates (TCs) covering resin collection to shipping container loading. This provides retail clients with verifiable chain-of-custody documentation to substantiate green claims.
BPA-Free, LFGB & REACH SVHC
Zero bisphenol substances, ortho-phthalates, or restricted heavy metals. Formulations pass stringent European LFGB organoleptic tests, ensuring zero odor or taste transfer to sensitive cold brew drinks.
Market Realities & Execution Scenarios
Engineered Drinkware for Global Commercial Channels
Different markets demand distinct engineering tolerances, barrier configurations, and aesthetic customizations. We tailor formulations and tooling to these precise operational environments.
Tier-1 Specialty Coffee & QSR Franchises
High-speed automated cup-dispensing machines require strict rim tolerance (±0.25mm) and non-stick de-nesting lugs. Our thermoformed RPET cups prevent double-dispenses, reduce operational delays, and support high-speed sealing film operations.
Volume Profiles: 12oz, 16oz, 20oz, 24oz Standard Calibration
Large-Scale Sports Arenas & Festivals
Major stadium operators face strict single-use bans alongside stadium safety restrictions that prohibit glass or heavy metals. Shatter-resistant RPET cups with in-mold customized labeling (IML) offer high-clarity event branding that collects easily for on-site recycling loops.
Acoustic & Impact Resilience: High Drop Safety Class
Omnichannel Retail & Promotional Private Labels
Consumer drinkware brands require retail-ready shelf presence. We integrate sustainable RPET bodies with specialty decorative lids, drill rhinestone sticker appliques, and electroplated accents—pairing circular materials with modern aesthetic trends.
Customization: CMYK Offset, UV Screen Printing, Custom Packaging
Next Horizon R&D
Engineering Roadmap: Circular RPET 2026–2030
We invest continuously in molding technology, chemical upcycling processes, and material sciences to expand what recycled polymers can achieve.
Phase 1: Chemical Glycolysis Integration
Moving beyond purely mechanical flaking, our pilot program incorporates glycolysis chemical depolymerization. This returns heavily tinted and decorated scrap to pristine monomer states (BHET), unlocking closed-loop recycling for previously hard-to-process retail drinkware.
Phase 2: Ultra-Thinwall High-Speed Tooling
Our tooling division is developing next-generation multi-cavity injection-compression systems. By cutting wall cross-sections by 18% while matching top-load crush force, we reduce raw resin use and freight costs per carton.
Phase 3: Digital Product Passports (DPP)
Ahead of European digital product passport requirements, our team is testing laser-etched 2D data-matrix codes on cup bases. This links end-users and sorting facilities directly to batch-specific recycling history and resin content data.
Procurement Due Diligence
Frequently Answered Technical & Sourcing Inquiries
Clear answers to common questions about recycled resin specifications, minimum orders, test reports, and factory workflows.
Are you a direct manufacturer or an export intermediary?
Wuyi Ronchine Industry & Trade Co., Ltd. operates as the export organization for our affiliated drinkware production facilities in Wuyi, Jinhua, Zhejiang. Sourcing directors work directly with an on-site, English-speaking engineering team coordinating molds, raw polymer procurement, automated injection molding, decorating, and AQL 1.5/4.0 inspections under one roof. We welcome on-site audits and live video walk-throughs.
Can RPET cups handle warm or boiling beverages safely?
Standard RPET cups are engineered specifically for cold and ambient beverages with a thermal deflection threshold of approximately 60°C to 65°C (140°F–149°F). Pouring boiling liquids into standard RPET can cause cup warping or deformation. For hot drinks, we recommend our specialized high-heat PP lines or double-walled vacuum stainless steel tumblers with food-grade polypropylene lids.
What is your minimum order quantity (MOQ) for custom branding?
MOQ depends on tooling and customization depth. Existing catalog profiles using standard stock colors allow lower quantities (often starting from 1,000 to 3,000 units with silkscreen or UV printing). Completely custom molded shapes or specific pantone-matched tinted resin runs generally start at 10,000 to 30,000 units to support efficient injection cycling and mold changeovers.
How do you guarantee batch-to-batch color clarity and avoid yellowing?
Lower-grade RPET flakes can tint yellow or gray due to repeated thermal cycles and label impurities. We use high-purity optical flakes combined with solid-state polycondensation (SSP) and spectrophotometer-measured toner balance (CIE L*a*b* coordinate controls). This keeps our L* value above 85 and b* yellow index below 1.5, matching virgin clarity.
What documentation accompanies each export shipment?
Each volume production run includes full QC inspection records, Global Recycled Standard (GRS) Transaction Certificates, Certificates of Analysis (COA) for resin parameters, and third-party food contact test reports (FDA 21 CFR or EU 10/2011/EC) performed by laboratories such as SGS or Intertek.
What are your typical sampling and production lead times?
Rapid 3D prototypes and color samples are completed in 7 to 15 business days. Once final pre-production samples are approved in writing, standard container mass production runs in 25 to 45 calendar days, depending on decoration methods like electroplating or rhinestone drill stickers. Our close proximity to Ningbo and Shanghai ports keeps export logistics smooth.
Extended OEM / ODM Production Series B
Comprehensive Drinkware Catalog & Specialty Lines
Browse our extended product lines, including specialized helmet cap designs, multi-layer rhinestone combinations, and spring-loaded eco travel drinkware.
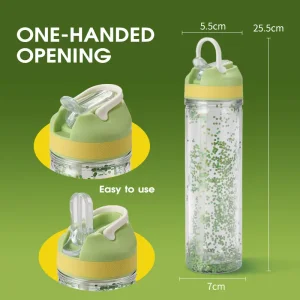
Wholesale Eco - Spring Loaded Cap YS-2096
Inquire Specifications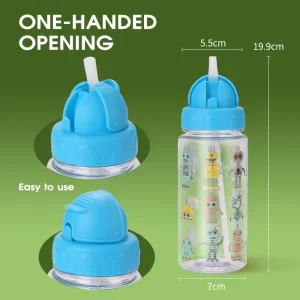
Wholesale Eco - Helmet Cap YS-2093
Inquire Specifications
China Eco - Helmet Cap YS-087A
Inquire Specifications
Wholesale Rhinestone Electroplating Gradient
Inquire Specifications
China Eco - Spring Loaded Cap YS-2434
Inquire Specifications
China Eco - Spring Loaded Cap YS-2431
Inquire Specifications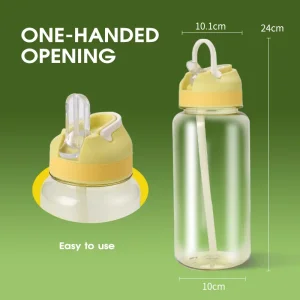
Wholesale Eco - Spring Loaded Cap YS-151A
Inquire Specifications