Integrated Eco-System Hardware & Hydration Components
Precision-molded accessories, eco-polymer caps, and insulated portable hydration vessels supporting global outdoor gear configurations, camp shelter kits, and circular retail lines.
The Circular Evolution in Commercial Camping Shelter Engineering
Strategic Transition from Virgin Petrochemicals to GRS-Certified Recycled PET: Lifecycle Decarbonization, Regulatory Frameworks, and Global Buyer Mandates.
The outdoor recreational and tactical shelter manufacturing sectors are undergoing a transformative paradigm shift. For decades, conventional tent architecture depended strictly on virgin nylon (polyamide) and virgin polyester (PET) woven fabrics derived from fossil fuel feedstocks. However, under escalating international climate governance—including the European Union’s Corporate Sustainability Due Diligence Directive (CSDDD), the EU Green Claims Directive, and North American Extended Producer Responsibility (EPR) mandates—importers, outdoor retail chains, and commercial camp operators are re-engineering their procurement supply chains.
The deployment of RPET (Recycled Polyethylene Terephthalate) in camping tents and modular shelters is not merely an eco-conscious branding exercise; it is an industrial imperative. By converting post-consumer PET bottles and discarded synthetic textiles into high-tenacity, yarn-spun filament fabrics (such as 75D, 150D, 210D, and 600D ripstop polyester), Chinese precision factories have bridged the historical performance gap between recycled and virgin polymers. Modern mechanical and chemical extrusion processes now deliver equivalent tensile, tear, and hydrostatic burst strengths while reducing greenhouse gas (GHG) emissions by up to 75% per metric ton of polymer compared to virgin PET production.
Life-cycle greenhouse gas reduction vs. virgin synthetic filaments.
Complete supply chain chain-of-custody transaction certifications (TC).
Advanced water column resistance via solvent-free aqueous coatings.
UV-resistant compounding preventing photodegradation and embrittlement.
Material Matrix: RPET Camping Fabric vs. Traditional Synthetics
Engineering specifications, yarn counts, polyurethane coatings, and lifecycle metrics across industrial tent substrates.
| Performance Parameter | 75D/190T RPET Ripstop | 210D RPET Oxford Fabric | Standard Virgin 75D Polyester | Standard Virgin 70D Nylon (PA66) |
|---|---|---|---|---|
| Raw Material Origin | 100% GRS Recycled Post-Consumer PET | 100% GRS Recycled Post-Consumer PET | Virgin Crude-Oil Petrochemical PET | Virgin Caprolactam Synthesis |
| Tensile Strength (Warp / Weft) | 780 N / 710 N | 1,420 N / 1,280 N | 800 N / 720 N | 860 N / 780 N |
| Tear Resistance (Elmendorf) | 18.5 N | 38.0 N | 19.0 N | 22.5 N |
| Hydrostatic Head (Waterproof) | 3,000mm – 5,000mm H₂O | 4,000mm – 8,000mm H₂O | 3,000mm – 5,000mm H₂O | 1,500mm – 3,000mm H₂O |
| Wet-Sag Coefficient | < 1.2% (Minimal sag in storm) | < 1.0% (Zero sag load) | < 1.2% | 4.5% – 7.0% (Heavy stretch when wet) |
| UV Degradation Half-Life | 450 UV Hours (UPF 50+) | 650 UV Hours (UPF 50+) | 420 UV Hours | 280 UV Hours (Prone to chalking) |
| Environmental Compliance | OEKO-TEX 100, GRS 4.0, PFC-Free DWR | OEKO-TEX 100, REACH, GRS 4.0 | Standard REACH only | Standard REACH only |
A persistent engineering myth held that recycled fibers suffer from brittle mechanical properties or inconsistent dye acceptance. At our Zhejiang manufacturing clusters, we resolve this through Solid State Polymerization (SSP), which restores intrinsic viscosity (IV levels to ≥0.84 dL/g) in recycled PET flakes prior to melt spinning. The resultant DTY (Drawn Textured Yarn) filaments exhibit high structural elongation and thermal resistance, outperforming virgin nylon in wet tensile stability. Unlike nylon, which absorbs water and elongates by 5% to 7% in continuous downpours, RPET maintaining structural tension across guylines, preventing water pooling and wind-induced frame collapse.
Supply Chain Resilience & Digital Manufacturing Efficiency
How vertically integrated clusters in Zhejiang combine raw material polymerization, automated laser cutting, and robotic seam sealing to protect client margins and lead times.
Automated CNC Nesting & Laser Cutting
Computerized layout algorithms achieve 94.2% fabric utilization across complex multi-panel flysheet patterns. High-precision laser cutting heads simultaneously seal edge fibers, eliminating fraying and enhancing downstream seam welding strength.
Automated Hot-Air Seam Taping
Critical failure in outdoor shelters occurs at needle penetrations. Programmable hot-air sealing stations apply multi-layer recycled PU tape at continuous calibrated temperature and feed rates, ensuring zero delamination under hydrostatic pressures exceeding 50 kPa.
MES-Driven Traceability & QC
From yarn lot tracking to needle-count monitoring on double-needle flatbed machines, our Manufacturing Execution System (MES) maps every production roll back to specific GRS batch certificates, giving brand owners complete audit confidence.
Field Applications: Engineering for Diverse Operational Climates
Customized RPET shelter architectures developed for commercial outfitting, hospitality glamping, tactical expeditions, and humanitarian logistics.
Alpine & 4-Season Expedition
Configured with 75D Ripstop RPET flysheets, silicone/PU hybrid coatings, and 7001-T6 aerospace aluminum poles. Rated for 60-knot gale winds, heavy sub-zero snow-load accumulation, and continuous UV exposure.
Luxury Eco-Glamping & Safari Domes
Utilizing heavyweight 300D to 600D recycled Oxford poly-canvas with breathable membrane backings, CPAI-84 fire-retardancy chemistry, anti-mildew finishes, and high thermal insulation for year-round eco-resorts.
Festival & High-Volume Family Camping
Engineered for rapid deployment via pre-assembled hubbed fiberglass or air-beam poles. High interior volume, dual-door cross-ventilation, integrated bug-mesh panels, and compact packability for retail channels.
Emergency & Humanitarian Disaster Relief
Rapid-deployment modular emergency shelters designed for high durability under harsh displaced-person camp conditions. Cost-efficient, mold-proof, rainproof, and 100% recyclable after decommissioning.
From Concept CAD to Global Container Delivery
A standardized 5-stage quality-assured engineering pipeline protecting buyer intellectual property and product specifications.
Structural R&D & Digital CAD
Aerodynamic wind modeling, Finite Element Analysis (FEA) on stress corners, and CAD panel digitizing based on customer volume targets.
Raw Material Lab Testing
Yarn denier verification, spectrophotometric Pantone lab-dip matching, GRS certificate auditing, and hydrostatic burst-pressure pre-checks.
Rapid Prototyping & Rain-Room
7-to-10 day prototype creation followed by an intensive 48-hour artificial monsoon deluge test to confirm total seam watertightness.
Automated Assembly Lines
Laser cut panels, multi-needle synchronized stitching, automated seam welding, and bar-tack reinforcement at every guyline tension vector.
Carton Packaging & Seaport Export
Custom compression carry bags, eco-cardboard master cartons, pallet strapping, and direct drayage to Ningbo or Shanghai deep-water ports.
Audited Compliance Standards: Eliminating Greenwashing Risk
Comprehensive laboratory documentation, chemical restriction protocols, and international environmental certifications.
Corporate buyers face severe reputational and legal risks from unverified environmental claims. Our factories maintain third-party audited compliance protocols, ensuring every square meter of RPET tent fabric and accompanying injection hardware can withstand rigorous customs inspection and retail consumer audits:
- Global Recycled Standard (GRS 4.0): Validates the exact percentage of post-consumer recycled content through Transaction Certificates (TCs) generated for each batch shipment.
- OEKO-TEX® Standard 100 (Class I/II): Certifies that textiles, coatings, zippers, and hook-and-loop fasteners are free from carcinogenic amines, formaldehyde, heavy metals, and banned plasticizers.
- Zero Fluorocarbons (PFC-Free C0 DWR): State-of-the-art organosilicon and plant-based hydrophobic barrier technologies that eliminate per- and polyfluoroalkyl substances (PFAS) without compromising water beading.
- Flame Retardancy Norms: Formulations engineered to satisfy US CPAI-84, NFPA 701, and European BS 7837 / EN ISO 6941 flame-spread standards without using toxic halogenated PBDE chemicals.
- ISO 9001 & ISO 14001: Fully audited quality and environmental management systems in our Wuyi, Zhejiang production hubs.
Frequently Asked Questions: RPET Tent & Gear Procurement
Clear, definitive answers to commercial inquiries regarding MOQs, testing protocols, coating durability, and factory auditing.
How do you verify that the tent fabric is genuinely made from recycled plastic (RPET)?
We supply official Global Recycled Standard (GRS) Transaction Certificates (TC) issued by accredited third-party certifiers (such as Control Union or Intertek) with every order. The TC documents the complete custody chain from collected bottle bales and re-polymerized flakes to the final woven and coated tent roll numbers.
What is the typical Minimum Order Quantity (MOQ) for custom RPET camping tents?
For standardized frame designs utilizing in-stock custom-dyed RPET fabric colors, our MOQ starts at 300 to 500 units. For fully bespoke geometric designs requiring custom tooling, specialized pole hub moldings, or exclusive Pantone fabric mill runs, the standard production threshold is 1,000 units. Trial batches can be arranged under strategic development agreements.
Does RPET fabric degrade or become brittle under prolonged solar UV exposure?
No. The chemical structure of recycled PET is identical to virgin PET. Furthermore, our extrusion yarn formulation introduces Hindered Amine Light Stabilizers (HALS) and nano-titanium dioxide UV-blockers. In accelerated xenon-arc weathering tests (ISO 4892-2), our 75D and 210D RPET fabrics maintain over 85% of their original tensile strength after 500 continuous hours of intense radiation.
How does your waterproof coating withstand hydrostatic pressure without peeling?
We use a multi-pass aqueous polyurethane (PU) knife-over-roll coating method coupled with plasma corona surface pretreatment on the woven fabric. This creates a deep molecular bond between the polymer coating and the yarn matrix, preventing hydrolytic breakdown, milky chalking, and seam tape peel even after years of humid storage.
What are your sampling timelines and mass production lead times?
Digital 3D CAD modeling and pattern grading take 3 to 5 business days. Physical pre-production samples are completed within 7 to 14 days. Following sample sign-off and lab-dip approval, mass container-load production generally requires 30 to 45 days, depending on frame complexity, seasonal factory scheduling, and customized retail packaging configurations.
Can you provide matching eco-friendly tent hardware, stakes, and carry bags?
Yes. We offer an integrated, circular packaging solution. Carry bags are stitched from identical RPET yardage with recycled webbings. Structural stakes are manufactured from recyclable 7001 aluminum alloy or biodegradable polymer compounds, and individual packaging utilizes GRS-certified recycled polybags or FSC-certified unbleached kraft paper cartons.
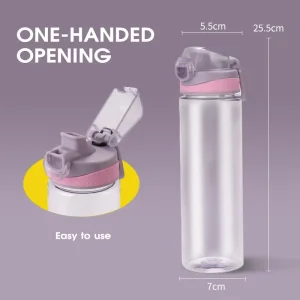
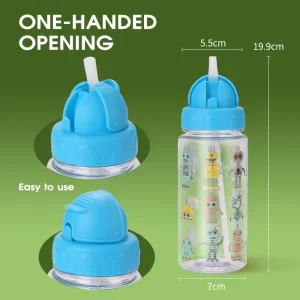
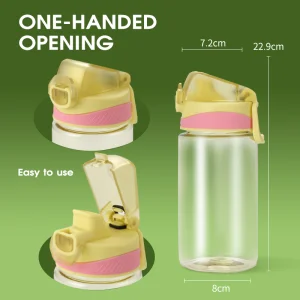
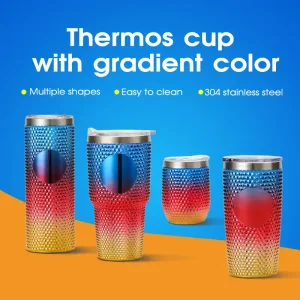
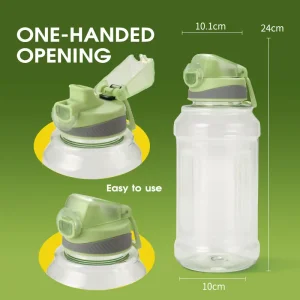
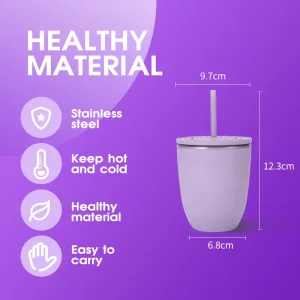
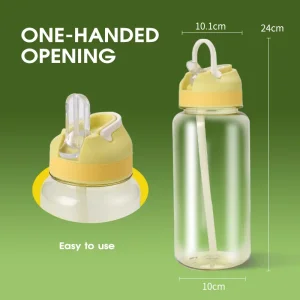
Engineered Eco Accessories & Precision Closures
Spring-loaded caps, impact-resistant helmet closures, and specialized hydration bodies manufactured under ISO 9001 and food-contact compliance.
Initiate Your Custom RPET Tent & Gear Program
Connect directly with our senior polymer engineering and shelter architecture teams in Wuyi, Zhejiang. Receive comprehensive material swatches, GRS scope certificates, and turnkey DFM (Design for Manufacturing) cost estimates within 24 hours.