Certified Recycled & High-Performance Drinkware
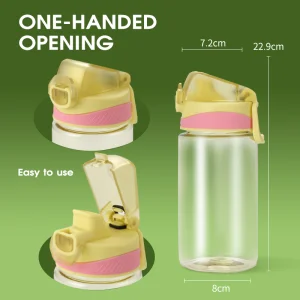
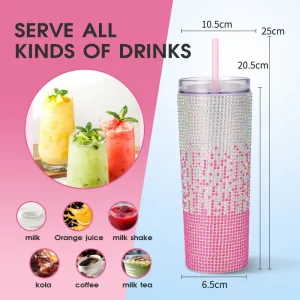
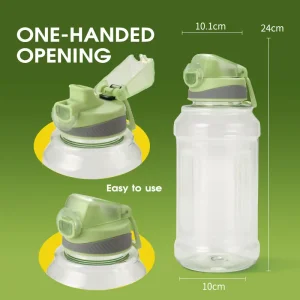
Factory-direct drinkware lines engineered with high-impact food-grade resins, innovative spring-loaded closure mechanics, and precision rhinestone drill aesthetics for global brands.
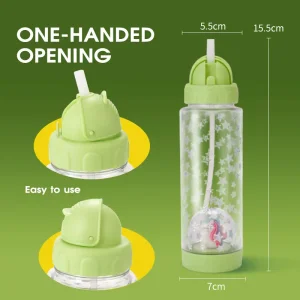
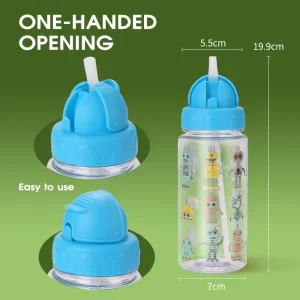
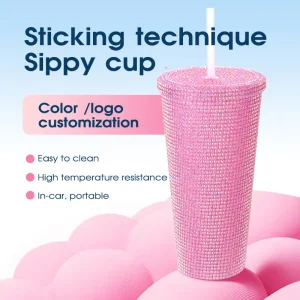
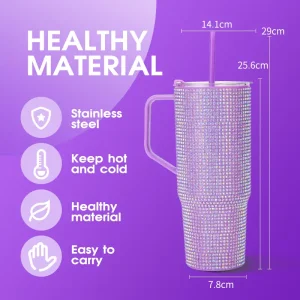
Decarbonizing Consumer Drinkware via Recycled Black Resins
Addressing the high-demand aesthetic of modern matte and obsidian drinkware while solving the classic optical sortability bottleneck in municipal recycling infrastructure.
Carbon Black Problematic
Conventional black masterbatches employ carbon black pigments that absorb Near-Infrared (NIR) spectrums entirely. Consequently, automated Material Recovery Facilities (MRFs) fail to detect polymer signatures, channeling millions of recyclable bottles straight to landfills or thermal incineration. Our technical formulations bypass this through infrared-transparent chromophores.
Food-Grade PCR Purity
Transitioning recycled polyolefins (rPP) and recycled polyesters (rPET) into direct food-contact containers demands meticulous thermal degassing, vacuum stripping, and continuous decontamination. Our factory processes utilize certified decontamination systems compliant with FDA Non-Objection Letters (NOL) and EFSA food-contact safety standards.
Scope 3 Emission Cuts
Virgin resin production is a carbon-intensive petrochemical operation. Switching institutional procurement to 100% Post-Consumer Recycled (PCR) black bottles provides documented reductions of up to 67% in Life Cycle greenhouse gas (GHG) emissions, enabling Fortune 500 corporations and global retailers to hit verified Science Based Targets (SBTi).
Technical Roadmap: Polymer Engineering & Circularity Milestones
A multi-generational roadmap addressing structural rheology, colorant detectability, odor volatilization, and the convergence of mechanical and chemical recycling.
NIR-Reflective Black Spinels
By adopting complex inorganic color pigments (CICPs) and proprietary organic perylene black dyes, our bottles transmit or reflect light within the 700nm–1100nm infrared spectrum. High-speed optical sorters equipped with hyperspectral cameras identify the base rPP or rPET resin in under 15 milliseconds, achieving automated sortation accuracy exceeding 98.4%.
Devolatilization & VOC Stripping
Recycled resins often retain residual post-consumer volatile compounds. Our extrusion lines incorporate twin-screw co-rotating extruders paired with triple-zone high-vacuum degassing ports operating at 5 mbar. This thermal-vacuum cascade expels volatile organic compounds (VOCs), aldehydes, and residual monomers, completely removing off-flavors and off-odors.
Solid State Polycondensation
Repeated thermal cycles degrade the intrinsic viscosity (IV) of recycled PET. Our raw polymer suppliers utilize continuous Solid State Polycondensation (SSP) reactors under inert nitrogen atmospheric control. This increases IV from 0.68 dL/g up to 0.84 dL/g, restoring virgin-grade tensile strength, shatter resistance, and top-load mechanical performance.
Future: Chemical Depolymerization
By 2027, our factory technical lines are partnering with enzymatic and glycolysis chemical recycling refineries. This breakthrough enables infinitely recyclable black polymers, breaking down complex mixed post-industrial waste streams into base monomers (BHET/PTA/MEG) without polymer chain shortening, closing the loop on pristine, medical-grade black drinkware.
Macro Industry Solutions: Regulatory Mandates & Traceability
Navigating global EPR taxation, stringent food contact migration safety, and chain-of-custody documentation across North America and the European Union.
| Target Region | Legislation / Framework | Enforcement Mandate | Our Engineering & Audit Compliance |
|---|---|---|---|
| European Union | EU PPWR (Packaging & Packaging Waste Reg) | Minimum 35% PCR in contact-sensitive plastics by 2030; 65% by 2040. | EFSA Verified GRS 4.0 Chain of Custody + Batch Traceable Certificates of Analysis (COA). |
| United States | State PCR Laws (CA AB 793, WA, NJ) + FDA 21 CFR | Graduated PCR quotas (up to 50%) with heavy civil non-compliance penalties. | FDA NOL Grade Raw materials backed by FDA Non-Objection Letters for Condition of Use C–G. |
| United Kingdom | UK Plastic Packaging Tax (PPT) | £217.85/tonne tax on packaging containing less than 30% recycled content. | PPT Exempt Guaranteed >30% to 100% PCR content verified via mass-balance accounting. |
| Germany / Europe | LFGB & EU Regulation 10/2011 (Migration Limits) | Overall Migration Limit (OML) < 10 mg/dm²; zero NIAS toxic leaching. | TÜV / SGS Tested Routine gas chromatography-mass spectrometry (GC-MS) screening. |
Non-Intentionally Added Substances (NIAS)
Recycling processes introduce potential risks of cross-contamination from printing inks, legacy flame retardants, or oligomer degradation. Our dedicated laboratory validates every batch using GC-MS and ICP-MS testing to guarantee total absence of prohibited phthalates, bisphenols (BPA/BPS/BPF), and heavy metals (lead, cadmium, mercury, chromium VI).
Global Recycled Standard (GRS)
Greenwashing liabilities can devastate consumer brand equity. Wuyi Ronchine enforces strict GRS 4.0 Transaction Certificates (TCs) for every production run. From the post-consumer collection bale, through flake sorting and compounding, to injection molding, our clients receive an unalterable paper trail verifying post-consumer authenticity.
Localized Compliance Support
Our dedicated regulatory affairs team directly coordinates with multinational compliance officers. Whether your distribution requires French AGEC Triman labeling compliance, German VerpackG registration validation, or California Proposition 65 settlement exemptions, we prepare full technical dossiers ready for legal customs release.
China Factory 4.0: Supply Chain Resilience in Zhejiang
Harnessing the world's most concentrated hardware and drinkware industrial cluster in Wuyi County, Jinhua, backed by Industry 4.0 automation and direct maritime shipping.
Integrated Tooling & Mold Precision
Our in-house CNC mold engineering center utilizes Swiss-machined EDM and high-speed milling to cut production cycle times. We operate multi-cavity hot-runner systems delivering micrometer-level gate precision. Molds are balanced to guarantee uniform wall thickness, critical for eliminating sink marks and stress-cracking in recycled polymers.
Robotic Automation & Vision Systems
From single-step Injection Stretch Blow Molding (ISBM) to automated cap sub-assembly and robotic leak-testing, human handling is minimized. High-resolution CCD visual inspection machines verify dimensional threading, mouth burrs, and color consistency on 100% of finished bottles at line speeds of up to 120 units per minute.
Ningbo Port Logistics Efficiency
Situated in Wuyi County, our manufacturing facilities benefit from mature freight arteries connecting directly to Ningbo-Zhoushan Port—the world's largest cargo throughput port. Containerized drayage reaches container freight stations (CFS) within 3 hours, offering resilient shipping schedules, lower drayage costs, and expedited FOB/CIF dispatch.
Robust Dual-Brand Portfolio
Operating our signature YAMI and Jass Life brands gives our engineering teams first-hand consumer feedback on durability, thermal retention, and cap ergonomics. This retail-grounded expertise transfers directly into OEM/ODM contract manufacturing, de-risking your investment before commercial mass-market rollout.
Global Procurement Matrix: QA Vetting & Physical Specifications
Standardized quality control parameters, AQL inspection levels, and mechanical tolerance benchmarking for procurement directors and sourcing managers.
| Performance Characteristic | Testing Protocol | Acceptance Criteria | Engineering Significance |
|---|---|---|---|
| Hydrostatic Leak Resistance | ASTM D4991 / Vacuum Chamber Test | -40 kPa for 5 minutes; zero bubble emission | Guarantees 100% seal integrity during air freight and dynamic transport. |
| Drop Impact Resistance | ASTM D2463 (Drop Dart Procedure) | 1.5m drop onto polished concrete, 5 angles at 4°C | Prevents brittle shattering common in unformulated recycled plastic grades. |
| Color Variance & Delta E | Spectrophotometer CIELAB (D65 light source) | ΔE < 0.8 across lot-to-lot runs | Eliminates the blotchy, muddy tones typical of inconsistent scrap PCR sorting. |
| Torque & Cap Thread Life | Digital Torque Meter (ASTM D2063) | Removal torque > 1.2 Nm; 1,000 cycle open/close | Maintains consumer ergonomic feel without stripping or stress cracking threads. |
| Thermal Shock Resistance | Cyclic Water Immersion (0°C to 85°C) | 5 complete cycles without micro-fissuring | Validates resilience for dishwasher cleaning and temperature transitions. |
Rigorous AQL Level II Inspection
Every production run adheres strictly to ANSI/ASQ Z1.4 (ISO 2859-1) sampling plans. We execute 0 Critical, 1.0 Major, and 2.5 Minor defect classification cut-offs. Comprehensive pre-shipment inspection (PSI) reports—complete with dimensional scans, torque measurements, and bar-code scannability tests—are archived and shared prior to balance payments.
Pantone & Surface Mastery
Achieving a deep piano black, stealth matte satin, or textured carbon finish on recycled plastic demands custom surface treatment. Our post-finishing workshop offers UV curable coating, soft-touch polyurethane spraying, gradient vacuum metallization, and laser engraving that preserve PCR integrity without compromising recyclability.
Tier-1 Retail Social Compliance
Our manufacturing partner sites in Wuyi regularly undergo independent Sedex SMETA 4-Pillar and BSCI audits. We maintain absolute compliance with fair labor regulations, health and safety, zero-child-labor mandates, and environmentally responsible wastewater and VOC discharge practices, ensuring seamless integration into Walmart, Target, and Costco supply chains.
Advanced Finishes, Electroplated & Combination Drinkware
Expand your consumer offerings with multifaceted rhinestone electroplating, gradient finishes, multi-piece gifting combinations, and proprietary cap molds engineered for peak durability.
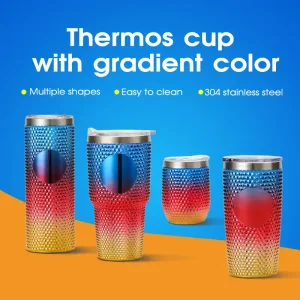
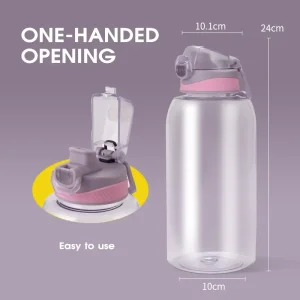
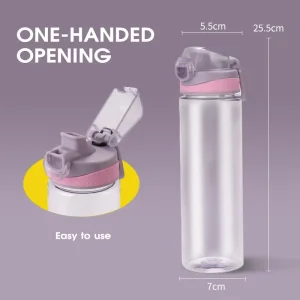
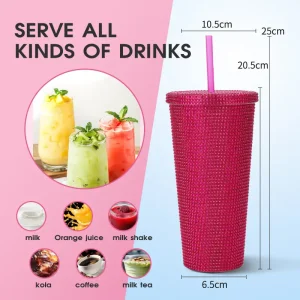
Wholesale Combination - Rhinestone Electroplating Gradient Manufacturers, Manufacturer
View Specifications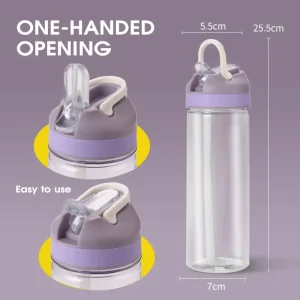
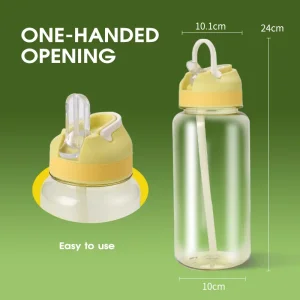
Engineering, Sourcing & Compliance Q&A
Addressing the most critical technical, commercial, and operational questions posed by institutional buyers and supply chain executives.
How do your black recycled bottles overcome optical sorting rejection at municipal recycling facilities?
Traditional black plastics use furnace-produced carbon black, which absorbs light uniformly across the visible and Near-Infrared (NIR) spectrum (700nm to 1100nm). Because standard optical sorters rely on NIR reflectance to identify the polymer's spectral molecular fingerprint, traditional black items appear as void spaces on the conveyor belt and are rejected into residue bins for incineration or landfill.
Our factory formulates custom masterbatches using non-carbon NIR-reflective black colorants (such as mixed metal oxide spinels and specialized perylene organic dyes). These additives allow the NIR beam to penetrate the bottle wall and reflect back to the sensor, correctly categorizing the container as rPP, rPET, or rHDPE with an automated classification success rate exceeding 98%. We provide third-party sorting validation certificates (e.g., COTREP, RecyClass protocols) upon request.
What food-safety documentation accompanies your recycled plastic drinkware?
Direct food-contact drinkware made from post-consumer recyclate must satisfy stringent migration protocols. We supply comprehensive documentation dossiers including:
- US FDA Non-Objection Letters (NOL): Confirming that the recycling decontamination process cleans post-consumer flake to food-contact purity under 21 CFR 177.
- European Union Declarations of Compliance (DoC): Under Regulation (EU) No 10/2011 and (EC) No 1935/2004, including overall migration testing (OML) and specific migration limits (SML) for heavy metals and primary aromatic amines.
- Global Recycled Standard (GRS) 4.0: Formal Transaction Certificates (TC) verifying the precise percentage of genuine post-consumer vs. post-industrial feedstock.
- NIAS Risk Assessments: Gas chromatography screening validating that Non-Intentionally Added Substances remain below toxicological thresholds of concern.
What are your minimum order quantities (MOQ) and lead times for custom-molded black recycled bottles?
Our standard production thresholds are structured around operational efficiency:
- Existing Private Label Molds: MOQs start at 1,000 to 3,000 units when selecting standard body geometries with custom PMS color matching, silk-screen, heat transfer, or UV-cure pad printing.
- Fully Custom Tooling (OEM): MOQs typically begin at 5,000 to 10,000 units to amortize dedicated blow mold tooling and injection preform tooling.
- Tooling Timelines: 3D CAD modeling and photorealistic renderings are delivered within 48 hours; functional SLA/CNC prototypes take 5–7 days; multi-cavity hardened steel production molds take 20–25 days.
- Mass Production: Standard order fulfillment spans 25 to 35 calendar days from golden sample sign-off, coordinated directly with Ningbo port dispatch.
How do you manage mechanical strength and color variations inherent to recycled plastics?
Post-consumer feedstock varies naturally depending on regional collection sources. Left unmanaged, this yields brittle bottles with visible flow streaks, gel spots, and color drift. We mitigate this through three engineering safeguards:
1. Melt Flow Index (MFI) Homogenization: Raw flake lots are blended in 20-ton silo homogenizers to ensure uniform rheology prior to injection.
2. Impact Modification: Where high drop resistance is required, we cross-compound food-approved elastomeric impact modifiers that boost notched Izod impact strength by up to 40% without compromising stiffness.
3. Spectrophotometric Dosing: Gravimetric color dosers continuously meter our non-carbon black masterbatch to compensate for baseline grey/green PCR tint, keeping overall Delta E color variation under 0.8 across multiple production shifts.
Are you a direct manufacturing plant or an export trading entity?
Wuyi Ronchine Industry & Trade Co., Ltd. operates as the direct international sales, engineering coordination, and export gateway for our integrated drinkware manufacturing facilities in Wuyi County, Jinhua, Zhejiang. By consolidating molding, decorating (rhinestone application, electroplating, spray coating), quality control, and export logistics under one unified structure, we eliminate trading company markups and miscommunications.
Buyers interface directly with dedicated bilingual mechanical engineers and supply specialists. We invite clients to conduct physical plant tours or live remote video audits of our injection halls, cleanrooms, and automated testing labs at any time.
Can recycled black plastics handle hot liquids or microwave heating safely?
Thermal capabilities depend entirely on the base polymer selection:
- Recycled Polypropylene (rPP): Suitable for warm beverages, dishwasher cycles, and moderate hot-fill applications up to 100°C (212°F). However, microwave heating of recycled polymers is generally not recommended unless specific virgin-barrier co-injection techniques are utilized.
- Recycled PET (rPET): Best reserved for cold to ambient liquids (up to 60°C / 140°F). Exceeding this threshold causes thermal distortion and glass transition softening.
- Double-Wall Hybrid Construction: For high-temperature coffee and tea applications, we manufacture insulated drinkware featuring food-grade 304 (18/8) stainless steel interior liners paired with an external recycled black plastic structural shell, merging thermal insulation with circular packaging aesthetics.
Initiate Your Custom Sustainable Packaging Program
Whether you require custom NIR-detectable black bottles, GRS-certified post-consumer tumblers, or patented spring-loaded closures, our engineering team in Wuyi is prepared to review your 2D/3D CAD drawings, provide DFM analysis, and issue detailed cost estimates within 24 hours.