China Eco - Helmet Cap YS-2314B
View Factory SpecificationsIntegrated manufacturing ecosystems combine recycled polyester architecture with durable eco-polymer drinkware and protective hardware, verified through strict factory-direct quality control.
China Eco - Helmet Cap YS-2314B
View Factory Specifications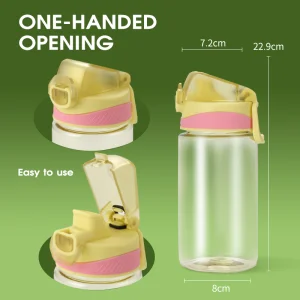
China Eco - Spring Loaded Cap YS-2431
View Factory Specifications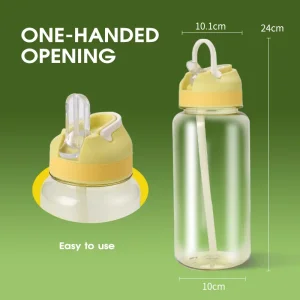
Wholesale Eco - Spring Loaded Cap YS-151A
View Factory Specifications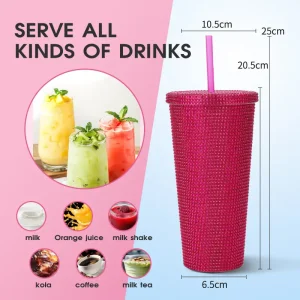
Wholesale Drill Sticker Straw Cup YS-004
View Factory Specifications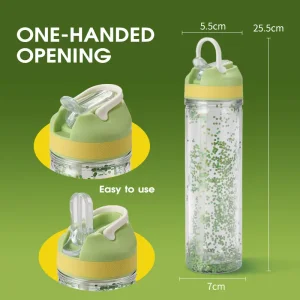
Wholesale Eco - Spring Loaded Cap YS-2096
View Factory Specifications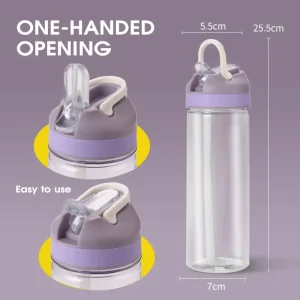
Wholesale Eco - Spring Loaded Cap YS-151B
View Factory Specifications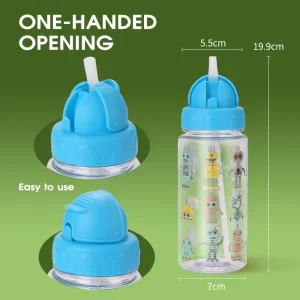
Wholesale Eco - Helmet Cap YS-2093
View Factory Specifications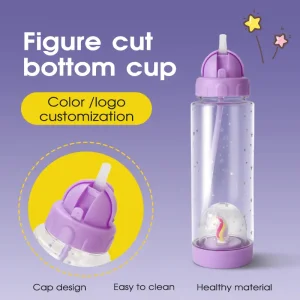
China Eco - Helmet Cap YS-087A
View Factory SpecificationsCamping tunnel tents require superior longitudinal tension stability, rigorous wind-shear deflection profiles, and continuous weatherproofing. Recycled Polyethylene Terephthalate (RPET) woven textiles, derived from post-consumer recycled plastic bottles, have transitioned from an ecological alternative to an engineering benchmark.
Tunnel tents feature large, aerodynamic hoops subjected to sustained aerodynamic drag and dynamic wind turbulence. Virgin polyester historically dominated this application due to molecular yarn consistency. However, high-tenacity RPET filaments now achieve tensile ratings exceeding 950 N in warp and 820 N in weft (ISO 13934-1 testing), matching virgin polymers through continuous solid-state polycondensation (SSP).
Waterproofing large tunnel tent envelopes requires micro-porous or monolithic barrier coatings that do not delaminate under cyclic thermal expansion. Our manufacturing partners utilize multi-pass solvent-free Polyurethane (PU) and silicone formulations that anchor to the textured RPET fibers, yielding hydrostatic pressure resistance from 3,000mm up to 10,000mm H2O (AATCC 127/DIN EN ISO 811).
Tunnel tents often remain pitched for extended family holidays or commercial glamping, exposing outer flysheets to aggressive ultraviolet degradation. By introducing organic benzotriazole UV stabilizers directly into the RPET masterbatch melt prior to filament spinning, our factories ensure UV protection factors of UPF 50+, limiting loss of tensile strength to under 8% over 300 hours continuous Xenon-arc exposure.
The production of technical camping tunnel tent fabric requires vertical synchronization across polymer recycling, chemical fiber extrusion, water-jet weaving, multi-layer coating, and dynamic environmental testing.
Located within Zhejiang's industrial corridors (Wuyi, Shaoxing, Huzhou), our partnered manufacturing network eliminates intermediary transport bottlenecks. The geographic proximity between bottle flake processing, masterbatch compounding, high-speed Toyota air-jet looms, and coating lines reduces supply-chain lead times by 35% compared to fragmented international suppliers.
Tunnel tents experience continuous shear stress along pole sleeve channels. China’s premier coating plants deploy computer-controlled knife-over-roll micro-applicators. This maintains uniform dry-film PU thickness down to ±1.5 microns across rolls up to 2.4 meters wide, preventing micro-pinholes that cause localized water ingress in heavy storms.
To safeguard international brands against greenwashing liabilities, Chinese manufacturers utilize ERP-driven serial identification systems. Every roll of RPET tent fabric includes a unique digital identifier linked directly to incoming Transaction Certificates (TCs), certifying the exact batch of recycled post-consumer PET bottles utilized in production.
Through mega-scale weaving operations running 24/7 on waterless dope-dyeing lines and automated grey-fabric inspection, Chinese facilities yield a 20% to 30% production cost economy compared to European or domestic converters, allowing brands to maintain strong margins even under tight retail price ceilings.
International outdoor gear procurement must comply with evolving eco-design regulations across North America, the European Union, and the Asia-Pacific region. Sustainable procurement is no longer just a marketing advantage—it is a legal necessity.
With the European Chemicals Agency (ECHA) and United States state legislations (California AB 1817, Maine, New York) banning per- and polyfluoroalkyl substances (PFAS/PFOS/PFOA), tent fabrics must utilize non-fluorinated Durable Water Repellent (C0 DWR) finishes. Our Chinese factories formulate bio-based silicone and branched hydrocarbon finishes that maintain a 90+ spray rating (AATCC 22) after 20 heavy home launderings without eco-toxic run-off.
European tent retailers must trace upstream carbon footprints and human rights compliance under the CSDDD and EU Extended Producer Responsibility (EPR) laws. Wuyi Ronchine and partner textile facilities deploy transparent tracking covering spinning mills, water treatment plants recycling up to 85% of industrial water, and Higg FEM/FSLM verified facility footprints to guarantee compliance.
Historically, tent flammability standards required halogenated flame retardants. Stricter health guidelines now restrict toxic brominated additives. We apply phosphorus-nitrogen halogen-free eco fire retardants directly within the RPET PU coating matrix, ensuring compliance with CPAI-84 Section 6, NFPA 701, and EN ISO 6941 without harmful chemical leaching.
From windy coastal plains to high-humidity sub-tropical campgrounds, camping tunnel tents rely on specialized denier, weave density, and coating combinations tailored to distinct environmental loads.
Large family tunnel architectures require broad fabric coverage without excess weight. We recommend 150D to 210D RPET Oxford with 4,000mm PU coating. This configuration offers high tear resistance for expansive door spans, balanced breathability, and integrated blackout PU pigments for restful sleep cycles.
In sub-zero alpine conditions where wind shears and heavy snow accumulation test structural resilience, 40D to 70D high-tenacity RPET Ripstop fabric coated with dual-sided silicone-elastomer (Sil/Sil) provides crack-resistant flexibility down to -40°C, shedding ice easily without coating failure.
Semi-permanent glamping tunnel structures remain exposed outdoors year-round. This operational profile demands heavy-duty 300D to 600D solution-dyed RPET canvas infused with anti-fungal biocide inhibitors, achieving ISO 846 resistance to mould alongside CPAI-84 continuous flame retardancy.
Minimalist fast-packing shelters require sub-50g/m² weight envelopes. Our ultra-fine 20D RPET micro-filament yarns are woven with double grid ripstop patterns, delivering puncture deflection and 3,000mm waterproofing while compressing to pocket-sized pack volumes.
Compare mechanical properties, chemical resistance, and sustainability metrics across typical tent fabric options used in wholesale production.
| Material Engineering Grade | Base Polymer Weight | Tensile Strength (Warp/Weft) | Hydrostatic Rating | Flame Retardancy | CO2 Footprint (kg/kg) | Target Sourcing Use |
|---|---|---|---|---|---|---|
| 150D RPET Ripstop (PU 4000) | 110 g/m² ± 5% | 880 N / 760 N | 4,000mm H2O | CPAI-84 Pass | 1.82 (45% vs Virgin) | Standard Family Tunnel Flysheet |
| 210D RPET Oxford (PU 5000) | 145 g/m² ± 5% | 1,150 N / 980 N | 5,000mm H2O | ISO 6941 / CPAI-84 | 1.95 (42% vs Virgin) | Heavy-Duty High-Wind Tunnel Shells |
| 70D RPET High-Tenacity (Sil/PU) | 68 g/m² ± 4% | 720 N / 690 N | 3,500mm H2O | Halogen-Free Pass | 1.64 (48% vs Virgin) | 4-Season Trekking Tunnel Tents |
| 300D Dope-Dyed RPET Canvas | 190 g/m² ± 5% | 1,420 N / 1,280 N | 6,000mm H2O | NFPA 701 Compliant | 1.38 (Waterless Dyeing) | Semi-Permanent Glamping Tents |
| Standard Virgin 190T Polyester | 72 g/m² ± 5% | 610 N / 520 N | 2,000mm H2O | Optional Chemical Add | 3.40 (Conventional Baseline) | Entry-Level Budget Shelters |
Wholesale sourcing of RPET technical fabrics requires a disciplined supplier auditing framework. Global brands must systematically verify mechanical tolerances, compliance documentation, and order fulfillment workflows.
Procurement begins with spectrophotometer color matching (Pantone TPX/TCX) and yarn denier verification. Factories provide 5-meter strike-off yardage for mechanical tensile testing, C0 DWR contact angle evaluation, and differential scanning calorimetry (DSC) to confirm 100% recycled PET polymer purity prior to loom setup.
During high-speed water-jet weaving and knife coating, automated optical inspection (AOI) cameras scan continuous roll surfaces at up to 60 meters per minute. The system detects yarn slubs, broken ends, coating micro-bubbles, and pinholes, flagging flaws immediately under the 4-point fabric inspection standard (ASTM D5430).
Before dispatch from Ningbo or Shanghai ports, independent third-party laboratories (SGS, TÜV, Intertek) conduct AQL 1.5 checks. Official GRS Transaction Certificates are issued via Textile Exchange accredited certification bodies (Control Union, IDFL), guaranteeing consumer marketing integrity.
Wholesale catalog solutions engineered to complement sustainable outdoor expeditions, manufactured with food-grade eco-plastics, custom surface finishes, and rigorous seal technologies.
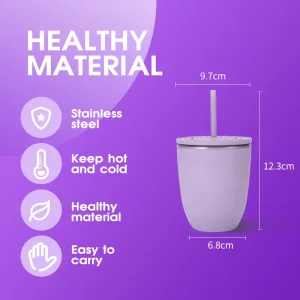
Wholesale Straw Cup Egg-Shaped YS-188
View Factory Specifications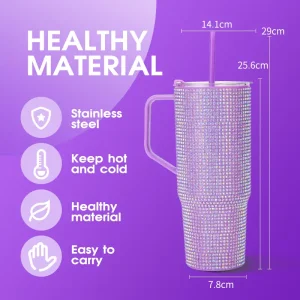
China Drill Sticker Single-Layer YS-2442
View Factory Specifications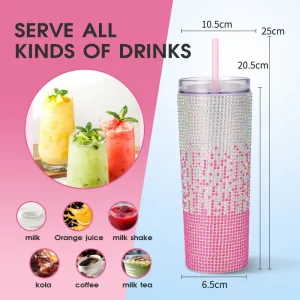
Wholesale Tall & Straight Tumbler YS-2045D
View Factory Specifications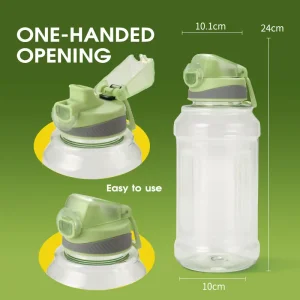
Wholesale Eco - Spring Loaded Cap YS-2433
View Factory Specifications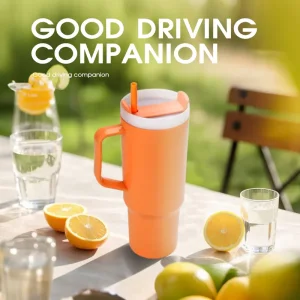
China Combination 3-in-1 Set Dol
View Factory Specifications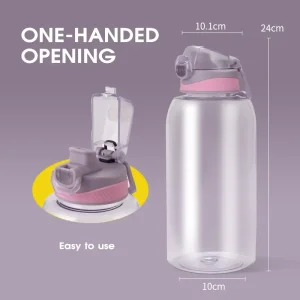
China Eco - Spring Loaded Cap YS-2434
View Factory Specifications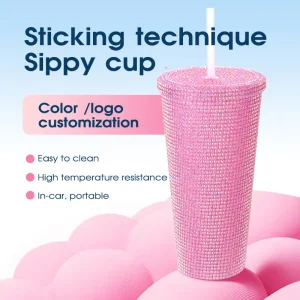
China Straw Cup Drill Sticker Series
View Factory Specifications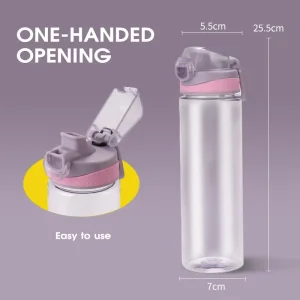
China Eco - Spring Loaded Cap YS-2432
View Factory SpecificationsDetailed answers addressing polymer chemistry, minimum order thresholds, cold-crack resistance, regulatory certifications, and overseas freight logistics.
Partner directly with leading Zhejiang technical manufacturing facilities. Request certified GRS swatches, complete technical data sheets (TDS), lab-dip color strike-offs, and custom OEM/ODM production schedules for your upcoming season.