Direct-from-Factory Catalog
High-Performance Eco Enclosures & Precision Packaging
Integrate certified food-contact compliant, biogenic, and barrier-enhanced solutions engineered across automated clean-room facilities.
Industry Intelligence Report
Global State of Recycled & Regenerated Cellophane Packaging
A macroeconomic and polymer science review evaluating bio-derived regenerated cellulose films versus fossil-based flexible plastics.
68.4%
Lower Scope 1-3 Carbon Footprint
180 Days
Full Soil Mineralization Rate
99.2%
Optical Transparency Factor
Zero
Microplastic Persistent Residues
Global Regulatory Pressures & EPR Mandates
With the intensification of Extended Producer Responsibility (EPR) programs in the European Union (Packaging and Packaging Waste Regulation - PPWR) and multiple North American states (e.g., California SB 54), manufacturers are legally compelled to source materials with verified post-consumer recycled (PCR) cellulose or industrial compostability.
- Elimination of petroleum-based Single-Use Plastics (SUPs)
- Stringent virgin plastic packaging surcharges ($800/ton EU benchmark)
- Mandatory recycled or biogenic content quotas
Regenerated Cellulose Matrix Mechanics
Unlike standard oriented polypropylene (BOPP) or low-density polyethylene (LDPE), engineered recycled cellophane bags utilize regenerated cellulose sourced from certified FSC managed post-industrial wood pulp and pre-consumer textile waste streams, subjected to an advanced closed-loop solvent spinning cycle.
- Superior dead-fold and static-free handling on high-speed VFFS lines
- Natural breathability balancing moisture and oxygen transit
- Inherent oil, aroma, and grease barrier integrity
Total Landed Cost & Supply Chain Resilience
High crude oil volatility directly affects polyolefin barrier film margins. Establishing a diversified wholesale procurement framework through specialized Chinese precision manufacturers offers stable unit economics, scalable container-load capacity, and reduced vulnerability to petroleum feedstock embargoes.
- Direct container loading through Ningbo port infrastructure
- Tiered volume economics with reduced MOQ barriers
- Integrated quality audits under verified ISO 9001 and ISO 14001 lines
Empirical Data Comparison
Polymers & Cellulose Film Specification Matrix
Benchmark engineering data validating tensile resistance, barrier efficiency, and regulatory compliance.
| Material Classification | Feedstock Provenance | WVTR (g/m²/24h) | OTR (cc/m²/24h) | End-of-Life Lifecycle | Compliance Standards |
|---|---|---|---|---|---|
| Recycled Cellophane Film (RCF-01) | Pre/Post-Consumer Cellulose Waste | 15 – 35 (Coated) | < 5.0 | Home Compostable / Marine Safe | EN 13432, ASTM D6400, FDA 21 CFR |
| Virgin Cellulose (Cellophane) | Certified Plantation Wood Pulp | 20 – 45 | < 8.0 | Industrial Compostable | FSC, PEFC, EU 10/2011 |
| BOPP (Fossil Standard) | Refined Petroleum Propylene | 4.0 – 6.5 | > 1,200 | Mechanical Recycled (Low Rate) | Standard Global Resins |
| RPET Recycled Film | Post-Consumer PET Bottles | 18 – 25 | 60 – 80 | Circular Mechanical Loop | GRS (Global Recycled Standard) |
| PLA (Polylactic Acid) | Fermented Plant Starch (Corn) | 150 – 200 | > 400 | Industrial Facility Only | BPI Certified, ISO 17088 |
Cross-Sector Deployment
Specialized Industrial Application Scenarios
Engineered flexibility designed to seamlessly integrate into automated converting lines and high-end retail displays.
Specialty Food & Confectionery
Micro-permeable, anti-static recycled cellophane wraps preserve aroma in gourmet chocolates, roasted coffees, and organic teas without inducing sweaty condensations typical of poly bags.
- High clarity high-gloss display surface
- Heat-sealable low-temperature coatings
- Zero chemical migration into food lipids
Luxury Apparel & Fashion Master-Bags
Replaces disposable LDPE apparel polybags. Breathable anti-moisture profiles shield sensitive silk, cashmere, and high-performance athletic textiles from mold proliferation during oceanic freight.
- Anti-static properties reduce dust attraction
- Re-sealable peel-and-stick adhesive flaps
- High-definition flexographic branding prints
Stationery, Greeting Cards & Collectibles
Optically neutral, crystal-clear archival protection. Unlike synthetic bags, recycled cellophane does not degrade, yellow, or leach plasticizers over decades of storage.
- True glass-like 99%+ optical transparency
- Rigid crinkle touch emphasizing prestige
- Acid-free neutral pH surface chemistry
Cosmetics, Soaps & Botanical Hygiene
Exceptional retention of volatile essential oils. Recycled cellophane bags act as an impermeable vapor barrier to fragrance loss while shielding botanical formulations from environmental humidity.
- High vapor retention for artisan cold-process soaps
- Greaseproof barrier prevents oily staining
- Certified bio-assimilable packaging credentials
Engineering Roadmap
Strategic Technical Milestones (2025–2030)
Pioneering nanocellulose synthesis, green chemistry solvent recovery, and barrier metallization to supersede petroleum films.
Phase I: Industrialization (Current)
Closed-Loop Lyocell Solvent Recovery
Eliminating carbon disulfide through advanced N-Methylmorpholine N-oxide (NMMO) solvent cycles, achieving a 99.6% closed solvent recovery loop with near-zero chemical effluents.
Phase II: Next-Gen Coating
Alu-Free Bio-Metallization Barriers
Applying vacuum-deposited nanocellulose crystalline coatings to deliver high oxygen barrier (OTR < 0.5) equivalent to metalized foil, keeping the film 100% industrially compostable.
Phase III: Automation Integration
High-Speed VFFS Heat-Sealing Window
Formulating bio-wax sealing layers with ultra-wide sealing windows (90°C–160°C), matching the run speeds of conventional fossil BOPP packaging machines (400 units/min).
Phase IV: Total Circularity
Post-Consumer Textile Upcycling
Deploying enzymatic fractionation to break down blended post-consumer cotton and denim waste into pure alpha-cellulose for endless industrial film extrusion cycles.
Factory Integration
Full-Scale OEM/ODM Manufacturing Capabilities
Bridging bespoke material formulation, custom printing specifications, and multi-tier quality assurance.
Custom Tooling & Bag Formatting
Precision converter architecture supporting flat satchel bags, square bottom gusseted bags, self-adhesive lip bags, perforated tear-notches, and micro-perforated aeration patterns tailored to product moisture release profiles.
Eco-Friendly Inks & Gravure Printing
High-precision 8-color water-based or algae-derived flexographic printing systems ensuring vibrant packaging aesthetics without releasing toxic volatile organic compounds (VOCs) or impairing compostability qualifications.
Stringent Lab Batch Validation (AQL 1.0)
Every extrusion run undergoes comprehensive tensile tear analysis, seal strength verification, differential scanning calorimetry (DSC), and spectrophotometer optical clarity tests before palletization and international export.
Wholesale Order Center
Featured Commercial Collections Ready for Export
Order direct from source facilities with custom brand configurations, multi-spec finishes, and global shipping logistics.
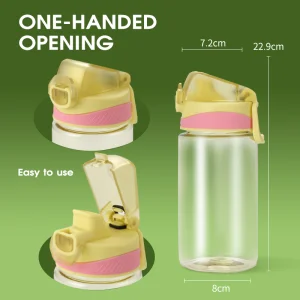
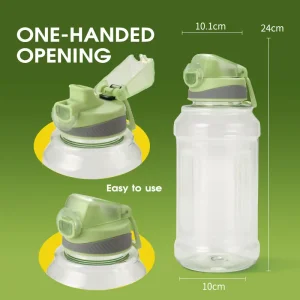
China Eco - Spring Loaded Cap YS-2431 Manufacturers, Manufacturer
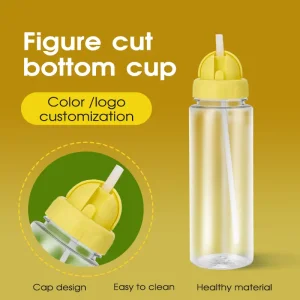
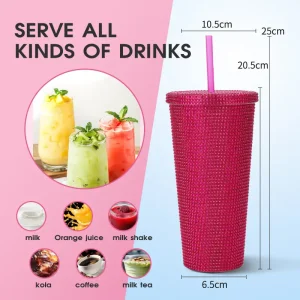
Wholesale Drill Sticker - Straw Cup YS-004 Manufacturer, Factories
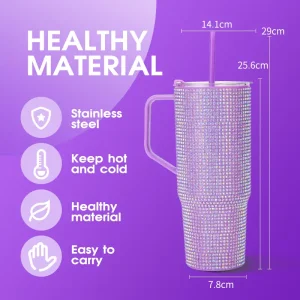
China Drill Sticker - 40 Single-layer YS-2442 Manufacturer, Factories
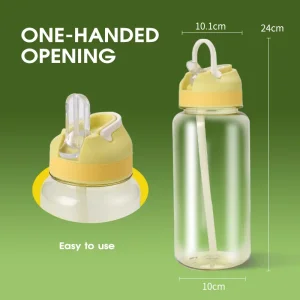
Wholesale Eco - Spring Loaded Cap YS-151A Manufacturer, Suppliers
Wholesale Drill Sticker - Tall and Straight YS-2045D Manufacturer, Factory
Technical & Procurement FAQ
Wholesale Recycled Cellophane Bags: Practical Guide
Comprehensive engineering clarity to support procurement directors, packaging engineers, and supply chain leads.
What fundamentally distinguishes recycled cellophane from conventional polypropylene (BOPP) bags?
Recycled cellophane is derived from regenerable alpha-cellulose polymers sourced from forestry side-streams and reclaimed plant fibers rather than petrochemical cracking. Cellophane possesses a natural static-free property, distinct crisp hand-feel, memory folding capability (dead-fold), and complete organic degradability. Polypropylene (BOPP) remains a fossil polymer that persists indefinitely in ecosystems unless collected for energy recovery or mechanical regrinding.
Are recycled cellophane bags certified food-safe under FDA and EU directives?
Yes. Our recycled cellophane formulations comply fully with FDA 21 CFR 177.1210 and European Commission Regulation (EU) No 10/2011 for direct food contact. Because our purification facilities utilize advanced chemical bleaching without chlorine gas (TCF processes) and food-grade heat-seal coatings, the resulting films exhibit zero harmful leachables or organoleptic cross-contamination, making them ideal for chocolates, nuts, baked goods, and dry foods.
What heat-sealing parameters are needed on standard packaging equipment?
Standard pure cellulose does not melt; it requires an applied heat-seal coating (such as water-based polyvinyl alcohol or bioplastic PVdC-free dispersions). Our bags feature an engineered sealing window between 105°C and 145°C. They can be smoothly utilized on horizontal flow wrappers (HFFS) and vertical form-fill-seal (VFFS) systems with minimal tension adjustments and Teflon-coated sealing jaws.
What are the minimum order quantities (MOQ) and production lead times?
For standard unprinted cellophane bags from stock film rolls, MOQs start as low as 10,000 units. For fully customized bag formats with multi-color branded rotogravure or flexographic printing, standard minimums are typically 30,000 to 50,000 units depending on bag surface area. Prototyping and custom cylinder engraving require 7–10 days, while mass container runs are fulfilled within 25–35 days from approved press proofs.
How do recycled cellophane bags perform under high relative humidity?
Because raw cellulose is intrinsically hydrophilic, moisture barrier attributes are dictated by the applied barrier formulation. Our high-barrier grade cellophane incorporates bio-based sealants delivering a water vapor transmission rate (WVTR) as low as 15–25 g/m²/24hr. This provides sufficient moisture protection for most shelf-stable foodstuffs (6–18 months) while preventing dry items from becoming soft or sticky under normal retail environments.