High-Velocity Sustainable Drinkware Inventory
Engineered for high-retention corporate merchandising, dynamic retail programs, and certified circular supply requirements.
The Global Commercial Landscape for Recycled Thermos Cups
Decarbonization pressures, changing polymer mandates, and the transformation of double-wall vacuum engineering across international markets.
Escalating Circular Demands
The global reusable drinkware sector is undergoing a tectonic transition. Projections place the worldwide insulated thermos and tumbler industry at upwards of $21.8 billion by 2032, with recycled-content items outpacing standard virgin items by nearly 3 to 1 in compound growth.
Retail buyers from big-box chains, promotional distributors, and premium DTC lifestyle brands are no longer treating circular materials as an optional SKU variant. Instead, strict corporate sustainability reporting standards (CSRD) in Europe and Scope 3 supply chain reduction requirements in North America have transformed recycled stainless steel (90% post-consumer content) and certified post-consumer resin (PCR) into non-negotiable procurement baseline metrics.
Evolving Regulatory Frameworks
Import compliance is no longer limited to basic food-contact hygiene tests like FDA 21 CFR or European LFGB. Modern procurement managers face a matrix of strict regional mandates:
- EU PPWR (Packaging and Packaging Waste Regulation): Minimum PCR percentages required across consumer containers with verifiable mass-balance tracking.
- CBAM (Carbon Border Adjustment Mechanism): Embedded carbon footprints in imported steel goods are subject to border taxation without verified factory green power offsets.
- GRS (Global Recycled Standard): Demands complete chain of custody validation from feedstock collection to warehouse arrival.
Industrial Scale at Wuyi Ronchine
Located in the heart of Zhejiang’s premium hardware manufacturing cluster in Wuyi County, Jinhua, Wuyi Ronchine Industry & Trade Co., Ltd. (YAMI / Jass Life) bridges advanced circular material science with automated OEM/ODM factory capacity.
Operating beyond traditional trading intermediaries, our integrated facilities execute precision hydroforming, automated vacuum brazing, electrostatic powder deposition, and cleanroom plastic molding under unified digital control. This guarantees that wholesale buyers receive verified sustainable products without compromising thermal insulation or surface tactile refinement.
Material Metallurgy & Polymer Integrity Matrix
Evaluating chemical safety, thermal conductivity, tensile performance, and environmental lifecycle impacts of primary cup materials.
| Material Classification | Feedstock Provenance | Thermal Degradation & Limit | Food-Contact Compliance | Lifecycle Carbon Offset | Engineering Suitability |
|---|---|---|---|---|---|
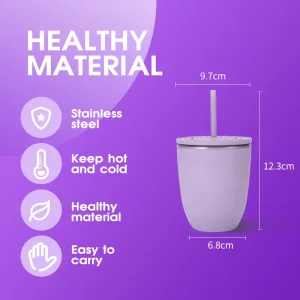
| Recycled SUS304 / SUS316 Stainless Steel | Industrial off-cuts & GRS-certified post-consumer household hardware melt pools | Stable up to 800°C; vacuum integrity maintained under thermal shocks (-20°C to 120°C) | FDA 21 CFR 175.300 / LFGB Section 30/31 | 72% reduction in CO₂ equivalent emissions vs. blast-furnace virgin iron ore | Inner and outer shells of double-wall vacuum thermos cups, Stanley-style tumblers, heavy-duty insulated bottles. |
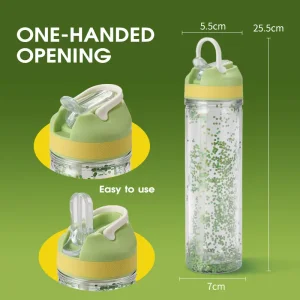
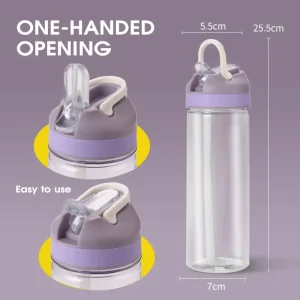
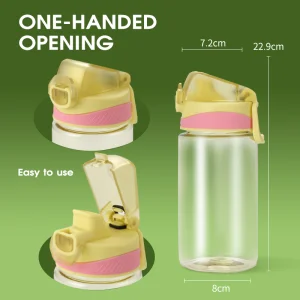
| Post-Consumer Recycled PP (Polypropylene) | Sterilized sorting of post-consumer food packaging and caps (rPP) | Heat deflection up to 105°C; resistant to boiling water extraction | EU 10/2011 Non-Intentionally Added Substances (NIAS) Cleared | 58% lower cumulative energy demand compared to petroleum-derived PP | Spring-loaded caps (e.g. YS-2096, YS-151A), threaded lid inserts, flip lids, travel handles. |
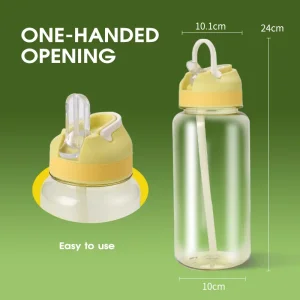
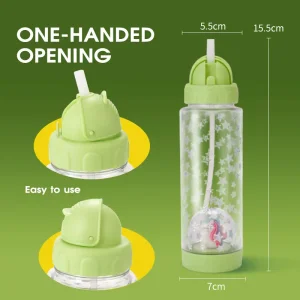
| Tritan™ Renew Copolyester | Molecular chemical recycling of mixed waste plastic polyesters | Continuous operating limits from -10°C to 95°C; extreme impact toughness | 100% BPA, BPS, and Bisphenol-Free Certified | Calculated up to 50% recycled monomer substitution via mass balance | Crystal-clear outer shells, premium transparent straw cups, shatterproof children's drinkware. |
| RPET (Recycled Polyethylene Terephthalate) | Mechanical sorting, washing, and re-pelletizing of post-consumer beverage bottles | Max operating ceiling: 65°C; unsuitable for hot boiling fluids without secondary blending | Cold/Ambient Liquid Certified Only | 67% carbon reduction over virgin PET resin pellets | Single-layer iced beverage tumblers, aesthetic outer sleeves, cold brew bottles. |
| Bio-Composite Wheat Straw Polymers | Agricultural waste chaff coupled with bio-based binding resin matrix | Operating thresholds: -20°C to 100°C; low thermal conductivity | Natural fiber extraction; non-toxic binder resin | Carbon neutral agricultural capture; rapid industrial biodegradation | Matte-finish exterior shells, helmet-style protective caps (YS-2314B, YS-087), eco tumbler bodies. |
Eliminating Secondary Degradation
A frequent challenge when running high PCR ratios through standard injection or stamping lines is molecular chain scission. This can cause micro-porosity, surface haze, or weakened tensile limits.
Our Wuyi engineering laboratory implements continuous melt-flow index (MFI) monitoring and nitrogen-shielded re-extrusion. This ensures that every metric ton of recycled polymer retains the structural elongation, drop resistance, and stress crack resistance identical to prime virgin polymers.
Lead-Free Vacuum Glass Sealing
Traditional mass-market insulated flasks historically relied on lead-solder beads to seal the inner vacuum chamber exhaust hole at the base. While insulated from direct drink contact, this creates end-of-life recycling hazards.
At YAMI / Ronchine, 100% of our premium recycled stainless steel thermos lines leverage automated lead-free vacuum brazing furnaces at 1050°C using safe copper-silicon alloys. This produces a safe, circular product compliant with Prop 65 and European REACH SVHC thresholds.
Macro Manufacturing Solutions for Global Brands
Comprehensive turnkey engineering from 3D CAD rapid prototyping to Ningbo port sea freight dispatch.
1. Custom Mold Tooling & Prototyping
Our in-house tool and die fabrication center converts conceptual sketches and industrial CAD files into hardened H13 steel injection molds within 14 to 21 working days.
We optimize gate locations, cooling lines, and ejection points specifically for PCR resin contraction behaviors. This eliminates sink marks on contoured travel mugs and ensures high dimensional stability across multi-cavity production runs.
2. Advanced Surface Decoration
Balancing sustainable materials with eye-catching retail appeal requires specialized surface treatment expertise:
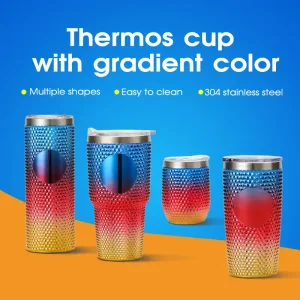
- Automated Electroplating: High-vacuum PVD sputtering for chrome, mirror, and gradient metallic sheens (YS-2433, grid electroplating models).
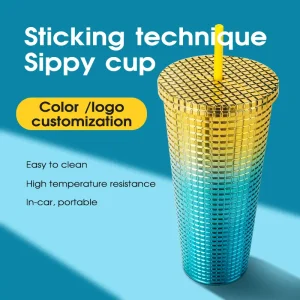
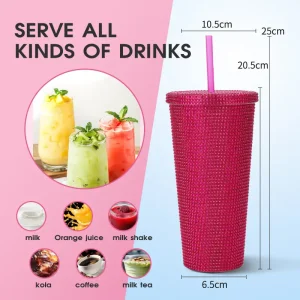
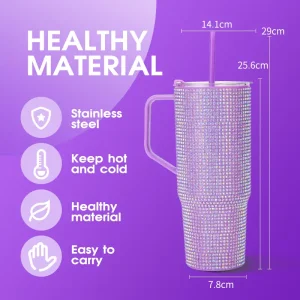
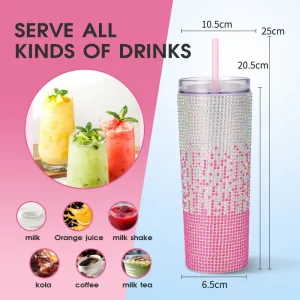
- Precision Drill-Sticker Inlay: Mechanical rhinestone application utilizing zero-VOC hot melt adhesives tested against 100+ commercial dishwashing cycles.
- Electrostatic Powder Coating: Solvent-free textured finishes providing scratch resistance, tactile grip, and customized Pantone color matching.
3. Zero-Defect Quality Assurance (AQL 0.65/1.5)
Every production lot at our Wuyi facility undergoes a standardized 7-stage quality control protocol:
- 100% Thermal Infrared Vacuum Verification: Cups are filled with pressurized hot air; robotic infrared sensors detect thermal leakage within 0.1°C tolerance.
- Positive Pressure Leak Testing: Caps and seals (including spring-loaded YS-2096/YS-151A assemblies) are submerged under 0.05 MPa pneumatic pressure.
- Drop & Centrifugal Adhesion Testing: Finished cups undergo 1.5-meter concrete drops and 3M cross-hatch tape tests on all logos and decorations.
Regional Drinkware Application Scenarios
Adapting insulation parameters, dimensional profiles, and lid ergonomics to match target regional usage patterns.
North American Commuter & Outdoor Culture
The US and Canadian markets require large capacity drinkware (30oz to 40oz) engineered with a narrow, tapered lower base to fit standard vehicle cup holders (diameter ≤ 75mm).
Consumers prioritize dual-function lids that allow open straw sipping for iced beverages alongside a leak-proof splash closure for hot coffee. Our Stanley-style insulated tumblers integrate heavy-duty ergonomic injection-molded handles built from reinforced PCR PP, tested to withstand 15kg tensile pull forces.
Western & Northern European Urban ESG
European retail channels (particularly Germany, France, and the Nordics) demand sleek, minimalist aesthetics (350ml to 500ml) paired with rigorous material traceability.
Drinkware in this segment must provide certified dishwasher durability (>100 cycles at 65°C without coating delamination) and complete single-material packaging using unbleached FSC-certified kraft paper with soy-based ink printing. Our helmet cap series (YS-2314B, YS-087) provides compact, secure closures popular with urban bicycle commuters.
East Asian Ultra-Light Commuter Requirements
In Japan, South Korea, and domestic metropolitan centers, consumer preference leans toward ultra-lightweight thermal flasks (150g to 220g total empty weight).
Our factory utilizes internal spinning and hydroforming technologies to reduce inner wall thickness down to 0.4mm without compromising 6-hour thermal retention (maintaining >68°C from an initial 95°C boiling fill). Aesthetic demands center around pastel gradients, antibacterial silver-ion interior liners, and compact spring-loaded flip caps (YS-151B, YS-2431).
Technical Roadmap & Sustainable Horizon (2025–2035)
Pioneering the next decade of double-wall thermal dynamics and closed-loop material engineering.
Circular Standardization & Traceability
Scaling up 90% post-consumer recycled austenitic stainless steel across all automated deep-draw stamping lines. Implementation of individual laser-etched QR code Digital Product Passports (DPP) on flask bases, providing buyers with batch-level mill test reports and GRS audit tracking.
Monomaterial Disassembly Engineering
Eliminating multi-material composite bonding that complicates post-consumer recycling. Developing modular friction-fit snap rings and separable threaded collars that allow end users to easily segregate silicone gaskets, PCR polypropylene lids, and steel vacuum bodies in domestic recycling streams.
Self-Powered Micro-Thermal Smart Drinkware
Integrating ultra-thin flexible thermoelectric generators (Seebeck effect) into the double-wall vacuum gap. This harvests waste heat from hot beverages to power integrated lid UV-C sterilization LEDs and digital OLED temperature monitoring without requiring external lithium-ion battery replacements.
Frequently Asked Technical & Sourcing Questions
Essential guidance for supply chain directors, category managers, and private label importers.
How does your factory authenticate recycled material content claims?
We provide comprehensive Global Recycled Standard (GRS 4.0) Transaction Certificates (TC) issued by accredited third-party inspection agencies (such as SGS or Intertek) with every commercial shipping lot. This documentation traces recycled stainless steel scrap and PCR plastic resin pellets directly back to the reclamation origin, validating chain-of-custody compliance for customs and environmental audits.
Does recycled stainless steel compromise vacuum insulation longevity?
Not at all. In our metallurgy lab, re-melted SUS304 undergoes secondary vacuum induction melting (VIM) and spectral composition verification to ensure chromium (18-20%) and nickel (8-10.5%) ratios are identical to virgin alloys. Vacuum integrity relies on molecular density and automated brazing at 10⁻⁴ Pa negative pressure, retaining hot liquids (>65°C) and iced drinks (<5°C) for 12 to 24 hours.
What are your standard Minimum Order Quantities (MOQ) and production lead times?
For existing open tooling using catalog Pantone shades with custom silk-screen or laser-engraved logos, our standard baseline starts at 1,000 to 2,000 units. Completely bespoke molds, proprietary cap designs, or custom rhinestone drill-sticker arrangements typically require a 3,000 to 5,000 unit opening run. Prototyping takes 7–12 days, with mass production completing within 25–35 days prior to Ningbo port export.
How do rhinestone and drill-sticker tumblers withstand commercial dishwashing?
Our hand-laid and automated drill-sticker tumblers (e.g., YS-004, YS-2045D, YS-2442) employ a proprietary heat-curing epoxy formulation that bonds individual faceted crystals to pre-treated, silane-primed cup walls. When dishwashing resistance is specified, items undergo cyclic thermal chamber tests (-10°C to 70°C water spray) to guarantee that adhesives do not soften or cloud over extended retail life.
Can you manufacture custom colorways and surface finishes using recycled materials?
Yes. Our automated coating lines execute electrostatic powder coating, multi-tone gradient lacquers, vacuum PVD electroplating, and hydro-dipped patterns across recycled substrates. We match physical Pantone formulas within a Delta-E color variance under 0.8, ensuring strict cosmetic consistency between production lots across all seasonal drinkware collections.
What testing certifications can be provided prior to ocean shipping?
We routinely supply batch testing reports for US FDA 21 CFR 175.300 / 177.1520, California Proposition 65 (lead and cadmium free), German LFGB Section 30 & 31, and European Union Regulation (EU) No 10/2011. Testing is performed in conjunction with ISO 17025 accredited global laboratories including TÜV Rheinland, SGS, and Bureau Veritas.
Wholesale Precision Drinkware Toolings
Explore additional popular molds ready for private labeling, customized surface coatings, and branded retail gift packaging.
Engineer Your Next Recycled Drinkware Collection
Connect directly with our engineering and export team in Wuyi, Zhejiang. Obtain physical production samples, complete material safety compliance reports, and factory-direct volume pricing.