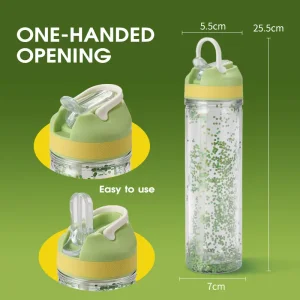
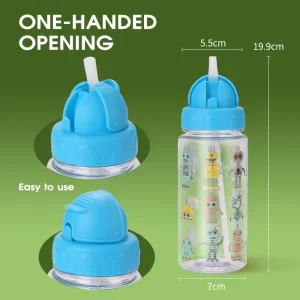
Featured Commercial Form Factors
Engineered Sublimation Drinkware & Eco Cap Series
High-performance cylindrical and ergonomic geometry designed for high-density dye-sublimation heat transfer, equipped with proprietary leak-proof caps and sustainable material configurations.
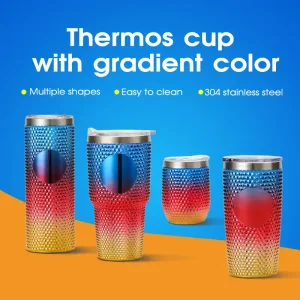
Wholesale Combination - Rhinestone Electroplating Gradient Manufacturers, Manufacturer
View Product Details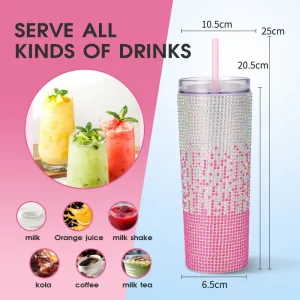
Wholesale Drill Sticker - Tall and Straight YS-2045D Manufacturer, Factory
View Product Details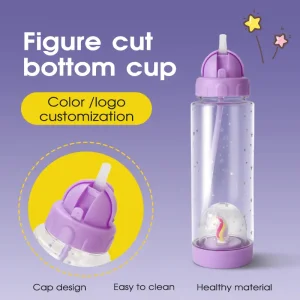
China Eco - Helmet Cap YS-087A Suppliers, Factory
View Product Details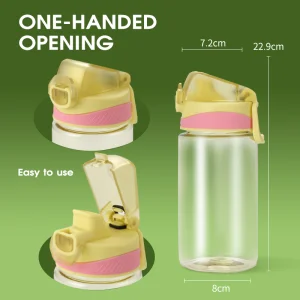
China Eco - Spring Loaded Cap YS-2431 Manufacturers, Manufacturer
View Product Details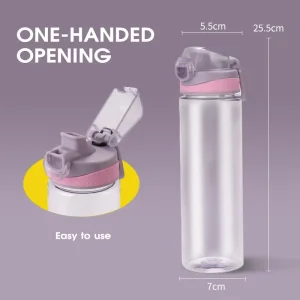
China Eco - Spring Loaded Cap YS-2432 Suppliers, Factories
View Product Details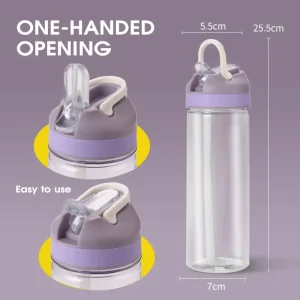
Wholesale Eco - Spring Loaded Cap YS-151B Manufacturer, Supplier
View Product Details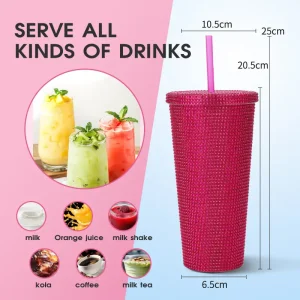
Wholesale Drill Sticker - Straw Cup YS-004 Manufacturer, Factories
View Product Details90%
Certified PCR Content Available
68%
Scope 3 Carbon Footprint Reduct.
≥50+
Commercial Dishwasher Cycles
±0.05mm
Wall Concentricity Tolerance
Industrial Paradigm Shift
The Circular Economy Revolution in Thermal Transfer Drinkware
How international regulatory pressures (EU CBAM, EPR directives, and corporate Scope 3 decarbonization mandates) are accelerating the transition from virgin stainless steel to traceable, Global Recycled Standard (GRS) certified sublimation blanks.
Circular Material Sovereignty
Conventional promotional drinkware has long depended on carbon-intensive primary austenitic smelting. Modern procurement now mandates verified closed-loop steel processing. By implementing certified post-consumer recycled (PCR) 304 (18/8) stainless steel, manufacturers eliminate the resource footprint of virgin iron ore extraction while slashing embodied energy requirements by up to 74% per metric ton.
GRS Chain-of-Custody
ISO 14021 Verification
Embodied Carbon Parity
Sublimation Polymer Engineering
Dye sublimation onto metallic substrates requires molecular receptivity that bare alloy cannot provide. The technical breakthrough lies in applying cross-linked, modified polyaspartic or organosilicon-modified polyester clear coats. These coatings accept disperse dye molecules during the thermal dwell phase (190°C–210°C) without blistering, yellowing, or compromising food-contact inertness.
Cross-Link Density
Non-Yellowing Matrix
High Chromatic Depth
Omnichannel Sourcing Demands
Global brand aggregators, corporate gifting consortia, and print-on-demand (POD) platforms face surging consumer demand for personalized aesthetic drinkware that performs reliably in commercial dishwashers. The modern sublimation blank must accommodate full-bleed photographic graphics, withstand aggressive cleaning chemistries, and pass strict heavy metal leach testing simultaneously.
POD Print Automation
Dishwasher Mechanical ASTM
Batch Consistency
Enterprise Strategic Sourcing Notice
Procurement teams should note that raw material recycled claims without third-party Global Recycled Standard (GRS) v4.0 Transaction Certificates (TC) represent substantial greenwashing compliance liabilities under both the EU Green Claims Directive and the FTC Green Guides. Wuyi Ronchine Industry & Trade Co., Ltd. provides batch-specific traceability verification across every heat of steel utilized in our Tongqin Industrial Park facilities.
Quantitative Engineering Benchmarks
Metallurgical & Coating Performance Comparison Matrix
Rigorous testing metrics comparing virgin alloys versus premium PCR 304 formulations, analyzing thermal insulation retention, tensile properties, coating adhesion, and lifecycle impact.
| Evaluation Parameter | Standard Virgin 304 SS | Certified Recycled PCR 304 SS | Certified PCR 316 Marine SS | Sublimation Coated Aluminum |
|---|---|---|---|---|
| Scrap/Recycled Content Rate | 0% – 15% (Unverified Mill Scrap) | 75% – 90% Verified PCR | 80% – 95% Verified PCR | 50% – 100% Recycled Scrap |
| Sublimation Coating System | Standard Epoxy-Polyester | Advanced Polyaspartic Hydro-Shield | Silica-Hybrid Polyaspartic | Standard Polyurethane Lacquer |
| Coating Adhesion (ASTM D3359) | Class 4B (Minor Flaking) | Class 5B (Zero Lattice Loss) | Class 5B (Zero Lattice Loss) | Class 3B – 4B |
| Thermal Heat Retention (24h) | > 58°C (Vacuum Double Wall) | > 62°C (Braze Welded Double Wall) | > 64°C (Getter Assisted Vacuum) | Single Wall (No Insulation) |
| Tensile Yield Strength (MPa) | 205 – 240 MPa | 215 – 250 MPa (Refined Grain) | 290 – 320 MPa (Molybdenum Add) | 90 – 130 MPa |
| Dishwasher Thermal Shock Resist | 20 – 30 Domestic Cycles | ≥ 60 Commercial Cycles | ≥ 100 Commercial Cycles | < 15 Cycles (Delamination Risk) |
| Heavy Metal Extraction (EU 10/2011) | Compliant (Virgin Control) | Fully Non-Detectable (ND) | Fully Non-Detectable (ND) | Requires Internal Barrier Liner |
Uniform Outer Diameter (OD) Control
Thermal transfer wrappers and vacuum 3D heat presses require strict cylindrical run-out tolerances. Our CNC rotary sizing dies guarantee bottle body concentricity within ±0.05 mm, ensuring complete, ghost-free peripheral ink saturation during heat pressing.
Active Degassing & Getter Brazing
To prevent sublimation coating blistering during high-temperature printing, steel shells undergo 1050°C vacuum degassing. Internal zirconium-aluminum chemical getters absorb residual hydrogen and nitrogen, preserving thermal vacuum efficiency indefinitely.
Optical White Polymeric Basecoat
Engineered with microscopic titanium dioxide (TiO2) particles embedded in high-clarity resin. This provides a clean CIE Lab L* brightness index exceeding 96.5, delivering true-to-life Pantone matching without metallic gray bleed-through.
Automated Precision Production
Integrated Production Architecture: From Scrap Ingot to Sublimation Master
Wuyi Ronchine Industry & Trade Co., Ltd. operates state-of-the-art manufacturing facilities in Wuyi, Zhejiang. Through vertically integrated stamping, multi-stage deep drawing, automated ultrasonic degreasing, and cleanroom robotic coating, we eliminate cross-contamination and guarantee consistent surface tension across every manufacturing run.
- Spectrographic Alloy Verification: In-house X-ray fluorescence (XRF) and spark emission testing on every steel coil to verify nickel (8.0%–10.5%) and chromium (18.0%–20.0%) chemistry before line feeding.
- Class 10,000 Spray Cleanrooms: Electrostatic disc application of sublimation coatings within positive-pressure HEPA-filtered environments eliminates airborne particulate defects.
- Multi-Zone Infrared Curing: Synchronized 4-stage thermal curing tunnels polymerize the coating without embrittlement, ensuring flexible elongation during thermal expansion cycles.
5-Stage QA Certification Pipeline
1
Deep Drawing & Ultrasonic Degreasing
Cold hydroforming of inner/outer walls followed by multi-bath alkaline degreasing to purge drawing lubricants.
2
10⁻⁵ Pa Vacuum Furnace Braze
Copper-braze high-vacuum seal maintained in multi-chamber continuous furnaces with real-time temperature logging.
3
Automated Laser Trimming & Necking
Burr-free laser edge processing ensuring precision lip-seal engagement for PP, AS, and Tritan closure lids.
4
Robotic Sublimation Basecoating
Automated dual-axis electrostatic bell applicators achieving continuous 35–45 micron dry-film coating thickness.
5
Full-Lot Thermal & Adhesion Inspection
100% online thermal camera vacuum validation plus destructive cross-hatch tape pull tests per ISO 2409.
Audit-Ready Global Governance
International Compliance & Import Safeguards
Mitigating regulatory exposure across North American, European, and Asia-Pacific customs regimes through rigorous third-party certifications, material test reports, and transparent supply chain documentation.
FDA 21 CFR & Prop 65 Assurances
Formulated specifically for the North American market, our sublimation polymer layers and food-contact accessories (silicone gaskets, food-grade PP/Tritan caps) undergo stringent extraction testing. Total lead content complies with California Proposition 65 thresholds (<90 ppm substrate, <10 ppm surface coating), eliminating port detention risks.
FDA 21 CFR 175.300
CPCS Lead Safety
BPA/BPS Free
LFGB & EU Regulation 10/2011
European Union markets enforce the strictest organoleptic and volatile organic matter migration protocols. Our bottles satisfy German LFGB Section 30 & 31 sensory odor/taste transfer evaluations, as well as EU 2020/1245 overall migration limit (OML) guidelines under 3% acetic acid, 10% ethanol, and 50% ethanol food-simulant exposures.
Sensory Neutrality
OML Migration <10mg/dm²
REACH SVHC Compliant
Port Logistics & Ningbo Proximity
Located in Wuyi County, Jinhua, Zhejiang, our production hub enjoys strategic proximity to Ningbo-Zhoushan Port (190 km) and Shanghai Port (310 km). This logistical positioning minimizes inland freight costs, provides direct container drayage access, and ensures dependable sailing schedules even during peak international retail cycles.
FOB Ningbo Direct
Consolidated FCL/LCL
FSC Carton Packaging
Innovation Trajectory 2026–2030
Technical Roadmap: Next-Generation Circular Hydration Platforms
Pioneering developments in plasma-enhanced chemical vapor deposition (PECVD), ultra-thin wall weight reduction, and closed-loop scrap recycling systems to advance commercial hydration engineering.
Phase 1: Bio-Derived Polymeric Clearcoats
Transitioning synthesis chemistries away from petroleum-derived polyester cross-linkers toward plant-based, renewable succinic acid polymers. These novel bio-coats match the thermal transfer clarity and dye absorption rate of conventional finishes while lowering non-renewable chemical dependence by 35%.
Phase 2: Hydro-Formed 0.3mm Thin Wall
Leveraging computer-controlled multi-stage hydropneumatic tooling to reduce outer bottle wall thickness from 0.50 mm to 0.38 mm without sacrificing drop-test deformation strength. This weight optimization reduces transport fuel emissions across bulk ocean shipments by approximately 18%.
Phase 3: Digital Product Passports (DPP)
Embedding laser-etched 2D data-matrix codes and NFC micro-nodes within the base boot cavity. This supports emerging EU Digital Product Passport mandates, giving enterprise buyers and consumers instant smartphone verification of alloy chemistry, recycled content percentage, and total product lifecycle data.
Technical Clarifications
Frequently Asked Questions for Enterprise Procurement
Detailed engineering answers regarding minimum order volumes, sublimation heating profiles, coating shelf lives, and custom OEM mold creation.
What chemical difference exists between sublimation coatings on recycled vs. virgin steel?
The external polymeric sublimation coating itself remains functionally identical across both metal types. However, recycled steel substrates require an extra step: our proprietary automated ultrasonic alkaline wash and micro-grit blast pre-treatment. This neutralizes scrap micro-impurities, achieving an optimal surface roughness (Ra 0.4–0.6 µm) that ensures strong mechanical interlocking and prevents thermal delamination under industrial heat pressing.
What are the recommended time, temperature, and pressure parameters for dye sublimation printing?
For rotary tumbler heat presses, we recommend 180°C to 190°C (356°F–374°F) for 50–60 seconds, followed by a 180-degree rotation and an additional 30-second dwell under medium-to-firm pneumatic pressure. For forced-convection 3D vacuum shrink-film ovens, we recommend 195°C (383°F) for 5.5 to 6 minutes. Detailed ICC color profiles tailored to our coating refractive index are provided upon contract execution.
How do you document and substantiate the Post-Consumer Recycled (PCR) percentage?
Every shipment includes a verifiable chain-of-custody dossier containing the primary melting mill's spectrometer assay, certified scrap sorting manifests, and Global Recycled Standard (GRS) v4.0 Transaction Certificates (TC) issued by accredited bodies such as Intertek or SGS. This documentation guarantees regulatory compliance against anti-greenwashing enforcement.
What Minimum Order Quantity (MOQ) applies to custom shapes versus stock blanks?
For standardized blanks in stock dimensions (e.g., 20 oz skinny, 30 oz curved, 40 oz handle tumbler), the MOQ begins at 1,000 units with standard white or shimmer clear coat. For custom proprietary geometries requiring new hydroforming and necking tooling, the initial pilot tooling batch is generally 3,000 to 5,000 units, with tooling amortization rebates available for volume commitments.
Can these sublimation bottles withstand industrial dishwasher cleaning?
Yes. Our high-adhesion polyaspartic and silane-functionalized basecoats resist over 50 commercial dishwasher cycles (operating at 65°C wash and 85°C rinse stages with alkaline detergents) without chalking, color fading, or edge peel. We rigorously validate production lots using continuous boiling-water immersion tests for 4 hours followed by an immediate cross-hatch peel test.
What are the standard production lead times from initial deposit to FOB dispatch?
Standard OEM sampling and rapid 3D-printed prototyping take 7 to 10 working days. Mass production of standard sublimation catalog SKUs requires 25 to 35 calendar days after pre-production sample sign-off. Bespoke tooling projects need approximately 40 to 45 days to account for pilot mold commissioning, vacuum pressure validation, and pilot production runs.
Partner With Our Wuyi Engineering Facility
Direct communication with technical account directors. Custom mold development, rapid testing samples, and volume quotes.
Comprehensive Collection Range
Specialty Drinkware, Straw Mugs & Spring-Loaded Caps
Browse additional high-demand drinkware models, specialty rhinestone finishes, and patented ergonomic cap accessories manufactured at our Zhejiang plant.
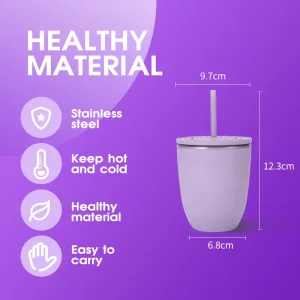
Wholesale Straw Cup - Egg-shaped Cup YS-188 Suppliers, Factories
View Product Details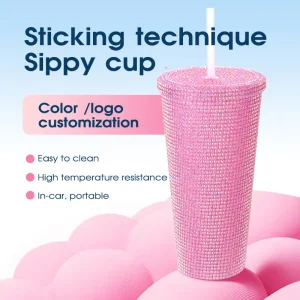
China Straw Cup - Drill Sticker Supplier, Factories
View Product Details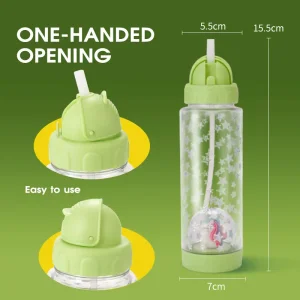
China Eco - Helmet Cap YS-087B Manufacturer, Supplier
View Product Details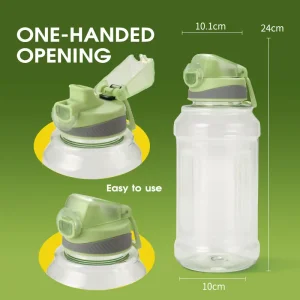
Wholesale Eco - Spring Loaded Cap YS-2433 Manufacturer, Factory
View Product Details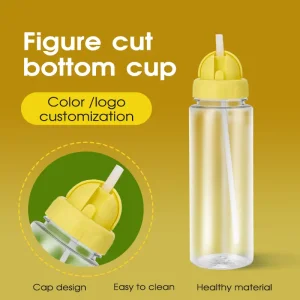
China Eco - Helmet Cap YS-2314B Manufacturers, Factories
View Product Details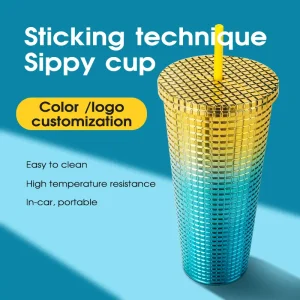
Wholesale Straw Cup - Grid Electroplating Manufacturer, Factories
View Product Details
Wholesale Eco - Spring Loaded Cap YS-151A Manufacturer, Suppliers
View Product Details