Featured Commercial Collections: Phase I
Explore high-velocity SKUs engineered from certified post-consumer recycled polymer matrices and food-grade resins, ready for enterprise customization.
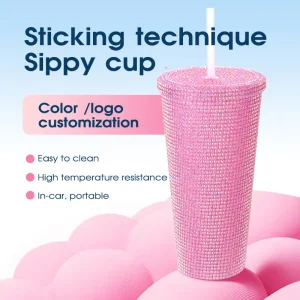
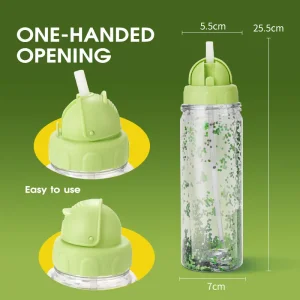
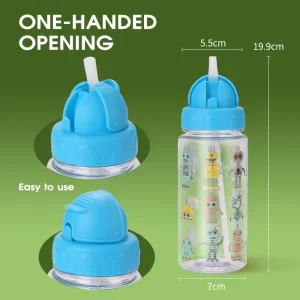
Engineering RPET: Material Physics & Closed-Loop Integrity
Navigating the transition from virgin polyethylene terephthalate to food-grade recycled matrices requires precise thermal profiling, solid-state polycondensation, and ultra-low monomer migration.
Intrinsic Viscosity Maintenance
RPET often suffers polymer chain scission during initial melt compounding. Our facilities utilize Solid-State Polycondensation (SSP) reactors to restore Intrinsic Viscosity (IV) levels back to 0.80–0.84 dL/g, ensuring structural tensile strength equivalent to virgin polymers without bottle collapse.
Optical Clarity & Color Rectification
Post-consumer recycling can induce yellowish-gray hazing from thermal cycles. We integrate precision optical sorting of post-consumer bales alongside trace toner balances to neutralize chromatic shift, resulting in glass-like transparency above 90% Light Transmission values.
Volatile Organic Compound Stripping
Through deep multi-stage vacuum thermal desorption at 210°C, volatile compounds, acetaldehyde, and potential non-intentionally added substances (NIAS) are extracted down to undetectable levels (<1.0 ppm), passing stringent migration thresholds under FDA 21 CFR 177.1630.
Macro-Level Solutions for Institutional Sourcing Leaders
Addressing regulatory friction, Extended Producer Responsibility (EPR), and margin pressures across enterprise drinkware distribution.
EPR & Single-Use Directive Mitigation
Navigating strict plastic packaging directives in the UK and European Union. Supplying institutional clients with audited chain-of-custody documentation (TCs), ensuring corporate compliance with plastic packaging taxes and international carbon baseline audits.
Omnichannel Dropship & Retail Readiness
High-cube utilization packaging design reduces logistics wastage. Products arrive certified for ISTA-3A/6-Amazon drop-test criteria, preventing transit ruptures on retail shipments and dynamic eCommerce distribution networks.
Custom Industrial Tooling & Rapid Scalability
Our rapid in-house mold facility turns CAD/CAM prototypes into hardened P20 or S136 stainless steel high-cavity tooling in 21 days, providing fast time-to-market for proprietary silhouettes and customized structural designs.
China Factory 4.0: Supply Chain Agility & Infrastructure
Based in Wuyi, Zhejiang—the epicentre of global drinkware industrial clusters. We combine upstream chemical purity with high-throughput automated robotics.
Automated Injection Stretch Blow Molding (ISBM)
Our clean-room manufacturing footprint houses automated single-stage and two-stage ISBM lines. Robotic end-of-arm tooling handles preforms and finished blown vessels, minimizing surface micro-scratches and human contact contamination. In-line machine vision cameras perform real-time neck finish, thread integrity, and particulate inspections at 120 units per minute.
Vertical Cluster Integration: Ningbo Export Gateway
Operating inside the Jinhua-Wuyi hardware-polymer manufacturing corridor allows us to procure raw food-safe color masterbatches, silicon gaskets, and custom carton packaging within a 30-mile operational radius. With direct intermodal connectivity to Ningbo and Shanghai deep-water container ports, we mitigate ocean logistics lead times and optimize supply continuity.
Technical Material Matrix: RPET vs. Conventional Polymers
A reference guide for engineering teams selecting appropriate substrates for sports hydration, hot tumblers, and promotional eco-campaigns.
| Resin Matrix | Structural Rigidity & Clarity | Thermal Deflection Point | PCR Carbon Offset | Optimal Application Scenario |
|---|---|---|---|---|
| RPET (Food-Grade PCR) | High transparency (>90%), balanced impact resilience | 65°C – 70°C (Cold/Chilled applications) | Up to 70% Scope 1-3 reduction | Aqua bottles, eco athletic bottles, corporate green initiatives. |
| Tritan™ (Copolyester) | Crystal-clear, near indestructible shatter resistance | 95°C – 100°C (Dishwasher safe) | Low (unless Tritan Renew certified) | Premium outdoor hydration, harsh institutional environments. |
| PP (Polypropylene) | Semi-translucent, flexible fatigue resistance | 105°C – 120°C (Microwave & Hot Fill) | Moderate (via bio-mass allocation) | Spring-loaded caps, shaker vessels, functional kids drinkware. |
| AS (Acrylonitrile Styrene) | Exceptional acoustic "clink", glass-like surface hardness | 75°C – 80°C (Cold beverage design) | Minimal commercial PCR availability | Double-wall insulated tumblers, rhinestone drill sticker vessels. |
Technology Roadmap: Sustainable Drinkware Systems
Continuous R&D allocations targeted at eliminating virgin fossil fractions and minimizing long-term cradle-to-grave footprint.
Mechanical PCR Purification
Deployment of high-vacuum, solid-state deodorization technology yielding 100% rPET bottles free from organoleptic defects or chemical off-gassing.
Enzymatic Chemical Upcycling
Collaborating with polymer depolymerization pioneers to utilize low-grade colored textile and oceanic plastic waste back into virgin-grade monomer feeds.
Monomaterial Barrier Coatings
Nano-silica (SiOx) plasma vapor deposition inside RPET bottles to double gas barrier resistance against oxygen ingress without impairing standard recycling streams.
Bio-Synthetic Functional Hybrids
Integrating non-food crop PEF (polyethylene furanoate) matrices with rPET compounds to elevate thermal tolerances beyond boiling point for universal hot-fill capability.
Enterprise Drinkware Offerings: Phase II
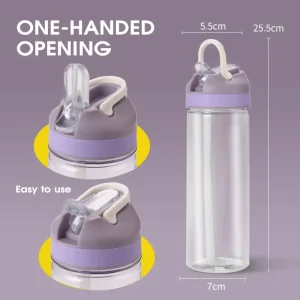
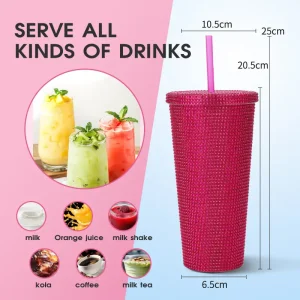
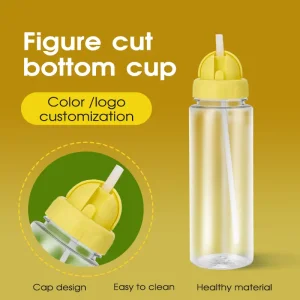
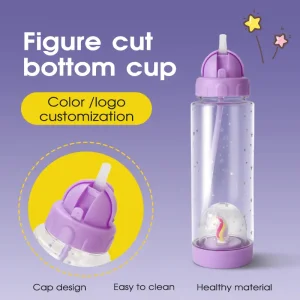
Precision engineered closures, electroplated multi-wall constructions, and trend-focused drinkware available for wholesale distribution.
Technical & Commercial FAQ
Common engineering and trade queries regarding food-contact rPET bottles and custom drinkware production.
What regulatory documentation confirms food-contact safety for RPET aqua bottles?
We supply accredited laboratory reports (SGS, TÜV, Intertek) verifying compliance with US FDA 21 CFR 177.1630, EU Regulation 10/2011, and German LFGB food contact standards. Every batch includes a Global Recycled Standard (GRS 4.0) Transaction Certificate (TC) tracking batch traceability back to source recovery plants.
Can RPET bottles handle carbonated water or hot liquids?
Standard RPET Aqua bottles possess a glass transition temperature (Tg) around 68°C–72°C, making them engineered for cold, ambient, or chilled hydration beverages (not boiling liquids). For carbonated beverages, we engineer thickened base petaloid designs capable of withstanding internal expansion pressure up to 4.5 bar.
What are the lead times for custom injection blow tooling versus OEM catalog models?
Catalog items with custom screen-print branding or customized Pantone color masterbatches require approximately 20–28 business days. For entirely new structural container geometries, mold engineering, 3D pilot sampling, and steel tooling fabrication typically complete within 25–35 days.
How do you prevent color shift and haze across large RPET production lots?
We purchase PCR resin batches with tightly specified Intrinsic Viscosity (IV) thresholds and low Hunter-b yellowness indexes. Our lines utilize gravimetric multi-component dosing systems that automatically introduce optical brighteners and blue-violet toners, ensuring strict delta-E color consistency across multi-container purchase orders.