Certified RPET & Precision Eco Systems (Primary Run)
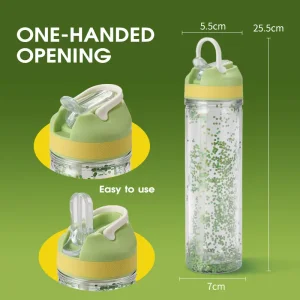
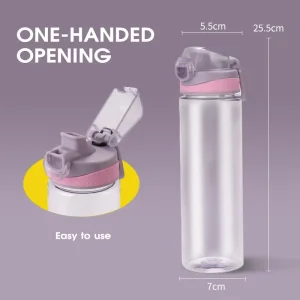
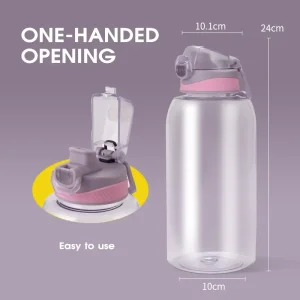
Direct factory-manufactured drinkware combinations, ergonomic safety lids, and certified food-contact compliant components engineered from high-grade recycled resins.
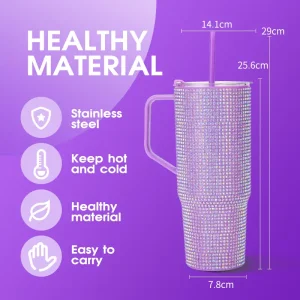
The Global Procurement Shift: Strategic RPET Integration
Enterprise procurement executives face escalating pressure to eliminate virgin petroleum polymers, achieve Scope 3 decarbonization, and navigate stringent extended producer responsibility (EPR) mandates.
Modern procurement officers operate in a drastically transformed regulatory ecosystem. Sourcing wholesale recycled polyethylene terephthalate (RPET) drinkware and structural beverage packaging is no longer merely a green branding endeavor; it is an industrial imperative dictated by strict transnational legislative policies. Corporations expanding into the European Union, the United Kingdom, North America, and Australasia must align with stringent circular economy metrics, including the EU Packaging and Packaging Waste Regulation (PPWR), which mandates progressive minimum recycled content thresholds of 25% by 2025 and upwards of 30% to 50% by 2030 across food-contact and non-food polymers.
At Wuyi Ronchine (YAMI Drinkware), our industrial ecosystem eliminates the common bottlenecks that multinational brand managers encounter when procuring recycled drinkware: polymer brittleness, thermal degradation, visual haze, and volatile organic compound (VOC) migration. By establishing an audited supply chain encompassing post-consumer bottle collection, optical flaking, hot-wash decontamination, and specialized solid-state polycondensation (SSP), our facility delivers RPET drinkware that meets the rigorous mechanical and optical tolerances traditionally exclusive to virgin petrochemical plastics.
Scope 3 Decarbonization
Quantifiable lifecycle emission reduction verified via third-party Life Cycle Assessments (LCA). Switching from petrochemical virgin PET to our mechanical RPET pellets yields an embodied carbon offset exceeding 65%, directly supporting corporate Science Based Targets (SBTi).
Tax Exemption & EPR Mitigation
Exempt your product lines from national plastic packaging levies such as the UK Plastic Packaging Tax (£217.85/tonne for <30% recycled content) and Spanish non-reusable plastic excise taxes through authenticated GRS 4.0 Transaction Certificates.
Retail-Grade Aesthetics
Overcoming the classical gray-yellow discoloration of degraded post-consumer material. Our proprietary filtration and spectrophotometric optical grading guarantee crystal clarity matching conventional AS and pure virgin copolyesters.
Technical Roadmap: Polymer Physics & Decontamination
A rigorous examination of polymer chain rebuilding, intrinsic viscosity control, and solid-state polycondensation in high-volume injection molding.
Linear polyethylene terephthalate undergoes severe hydrolytic and thermal scission when subjected to repeated heating and processing cycles. This intrinsic polymer degradation cuts ester bonds, increases carboxylic end-groups (-COOH), elevates acetaldehyde (AA) generation, and reduces the material's Intrinsic Viscosity (IV) from standard virgin levels of 0.80–0.84 dl/g down to structurally unusable thresholds below 0.60 dl/g. Sourcing from non-specialized wholesale vendors routinely results in stress-cracking under carbonation, brittle wall failure, or severe chemical leeching into beverages.
Solid-State Polycondensation (SSP) & Chain Restoration
To guarantee drop-test durability and structural integrity equivalent to premium virgin copolyesters, our production floor utilizes high-vacuum SSP reactor technology. By heating decontaminated post-consumer PET chips to temperatures between 200°C and 220°C below their melting point under a continuous inert nitrogen (N2) flush or vacuum (<1 mbar), esterification and transesterification reactions are re-initiated.
This thermodynamic treatment eliminates ethylene glycol byproducts, rebuilds fractured molecular weight distributions, stabilizes intrinsic viscosity back to target values of 0.82–0.86 dl/g, and purges volatile contaminants down to non-detectable sub-parts-per-billion levels.
| Performance Vector | Standard Recycled Flake | Wuyi Ronchine Purified RPET | Virgin Food-Grade PET |
|---|---|---|---|
| Intrinsic Viscosity (IV) | 0.60 - 0.68 dl/g (Brittle) | 0.80 - 0.84 dl/g (Tough) | 0.80 - 0.85 dl/g |
| Acetaldehyde (AA) Content | > 4.0 ppm (Sensory Flaw) | < 1.0 ppm (Zero Off-Taste) | < 1.0 ppm |
| L* Clarity / Color Value | L* 68 - 74 (Noticeable Tint) | L* 85 - 90 (Glass-Clear) | L* 88 - 92 |
| Tensile Yield Strength | 42 - 50 MPa | 58 - 65 MPa | 60 - 65 MPa |
| Heavy Metal Limits (RoHS) | Unregulated / Variable | Non-Detectable (<5 ppm) | Non-Detectable |
Closed-Loop Circular Solutions: From Flake to Shelf
An industrialized, transparent 5-stage chain of custody ensuring maximum regulatory compliance and uncompromising structural performance.
Optical Flake Sorting
Multi-spectral near-infrared (NIR) and camera sensors segregate clear bottles from uncolored or multilayer polymers, eliminating PVC, nylon, and non-PET contaminants down to <10 ppm.
Caustic Decontamination
High-temperature hot washing utilizing customized caustic soda solutions, detergents, and anti-foaming agents strips post-consumer adhesives, residues, labels, and exterior ink coatings.
Precision Melt Filtration
Vacuum-vented twin-screw extruders force molten polymer through ultra-fine 40-micron continuous backflush screen-changers, purging micro-particulates, crosslinked gels, and infusible matter.
Controlled Clean Molding
Pelletized RPET is processed on clean injection molding machines equipped with internal hot runner manifolds, ensuring constant cycle times and elimination of localized polymer degradation.
Cross-Border Regulatory Compliance & Food-Safety Verification
Safeguarding global brands with verifiable lab data, non-objection documentation, and certified export protocols for all key global markets.
Importing recycled drinkware requires stringent adherence to health, food contact, and heavy metal restriction frameworks. Non-compliant resins can release phthalate plasticizers, cyclic oligomers, or antimony trioxide catalysts into consumables, triggering customs seizures, heavy punitive fines, and severe brand damage.
FDA 21 CFR & CVM Nol Protocols
Resins employed meet criteria under US Food & Drug Administration 21 CFR §177.1630. Super-clean secondary recycling processes are backed by comprehensive challenge testing validating surrogate contaminant elimination.
EU 10/2011 & (EU) 2022/1616
Full compliance with European Food Safety Authority (EFSA) opinions and EU Regulation (EU) 2022/1616 on recycled plastic materials intended to come into contact with foods, confirming Overall Migration Limits (OML <10 mg/dm²).
GRS 4.0 & ISO 14021 Verification
Every shipment provides authentic Global Recycled Standard (GRS) Transaction Certificates (TC), validating exact chain-of-custody tracking from municipal waste collectors directly to the finished, packed carton.
Frequently Asked Technical & Sourcing Questions
Actionable answers to complex engineering, chemical certification, and minimum order queries directly from our production floor.
Visual hazing in RPET originates from inorganic fillers, moisture absorption, and thermal degradation during melt processing. We employ dual dehumidifying desiccant dryers operating at -40°C dew point prior to injection. Furthermore, we dose food-safe optical brighteners and blue-violet toner matrices that neutralize chromatic shifts (b* values) to deliver crystalline clarity comparable to virgin AS and Tritan.
Amorphous standard RPET exhibits a Glass Transition Temperature (Tg) of approximately 67°C to 78°C, making single-wall RPET unsuitable for piping-hot liquids above 80°C. For thermal endurance, we engineer dual-wall configurations (utilizing an inner 304 food-grade stainless steel vacuum vessel paired with an exterior RPET aesthetic housing) or offer modified CPET/Tritan-blend formulations for elevated thermal thresholds.
Every export shipment includes: (1) Official GRS 4.0 Transaction Certificate verified by accredited bodies like Control Union or Intertek, (2) Third-party testing reports confirming non-detectable heavy metals (RoHS/REACH SVHC), (3) FDA 21 CFR §177.1630 or EU 10/2011 Migration Test Certificates, and (4) In-house AQL 1.5/4.0 dimensional and mechanical inspection records.
For existing catalog tooling and standardized color runs, our MOQ starts at 1,000 to 3,000 units. For fully customized tooling, proprietary pantone matching, or custom injection blow molding, MOQs range between 5,000 and 10,000 units. Digital rendering and 3D prototype samples are completed in 3 to 5 business days, while fully functional production-run samples require 10 to 14 days.
Precision Eco Engineering & Custom Tumblers (Secondary Run)
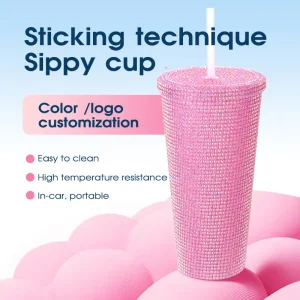
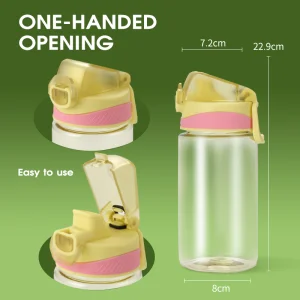
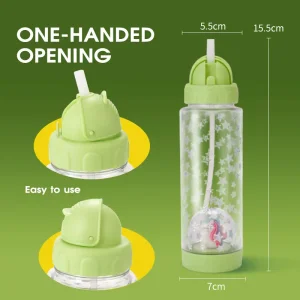
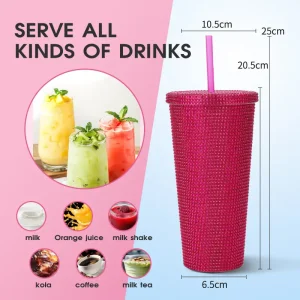
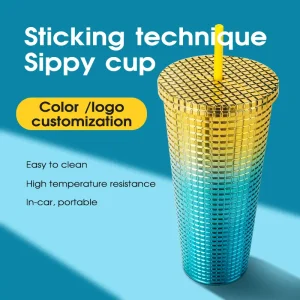
Complete product run featuring rhinestone drill finishes, vacuum spring-loaded sealing caps, and durable sports drinkware architectures.
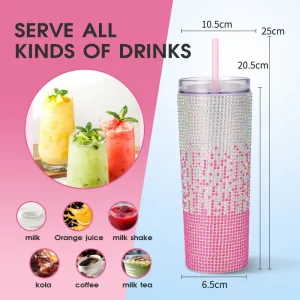
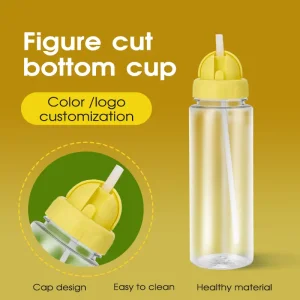
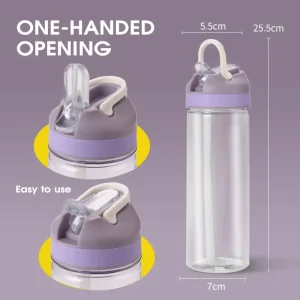
Partner Directly with Wuyi Ronchine Factory Engineers
Eliminate intermediary markups, mitigate compliance liabilities, and fast-track your enterprise drinkware pipeline with certified RPET injection manufacturing.
Located in Tongqin Industrial Park, Wuyi County, Zhejiang, China, our advanced facility operates more than 100 core manufacturing processes, employing 200+ experienced personnel and serving 5,000+ satisfied clients across North America, Europe, and Asia-Pacific. From tooling inception and 3D prototyping to multi-color gradient electroplating and automated packaging, our integrated factory delivers reliability at scale.