Featured Commercial Production Series (Batch A)
Direct factory manufacturing for global outdoor retail conglomerates, lifestyle labels, and sustainability-focused corporate distributors.
Circular Transition in Outdoor Hardware: The Recycled Steel Paradigm
Strategic shift toward certified circular supply chains, decarbonized manufacturing, and technical lightweighting across the global outdoor sector.
Closed-Loop Secondary Metallurgy
The global shift from virgin ore smelting to Electric Arc Furnace (EAF) processing using certified post-consumer scrap (PCR) reduces embodied energy consumption by up to 72% per unit.
- Traceable scrap sorting via optical and magnetic induction
- GRS (Global Recycled Standard) melt batch allocation
- Zero loss in tensile elasticity and yield strength during cold draw
Corporate Scope 3 Decarbonization
Global consumer retail brands require verifiable greenhouse gas audits across tier-1 and tier-2 vendor supply chains to comply with the EU Corporate Sustainability Due Diligence Directive (CSDDD).
- Product Carbon Footprint (PCF) certified down to Grams-CO2e
- Elimination of petroleum-based internal plastic liners
- Fully recyclable monomaterial construction for bushcraft systems
Ultra-Compact Bushcraft Kinematics
Consumer demand prioritizes compact nesting profiles, folding wire handles, and high weight-to-volume efficiency suitable for ultralight trekking, bikepacking, and tactical camping.
- Deep-drawn thin-wall architecture (0.4mm to 0.5mm 304/316)
- Stacking taper calculations allowing 100% volumetric nested packaging
- Ergonomic spot-welded folding wire handles resistant to 300N shear loads
Enterprise Sourcing Realities: Supply Chain Optimization
Mitigating landed unit costs, maintaining raw-material price hedge buffers, and standardizing multi-market quality control thresholds.
Landed Cost Modeling & Freight Optimization
Container load factor optimization directly impacts margin viability. Cylindrical vs. conical cup profiles determine whether an FCL 40HQ container carries 42,000 units or 120,000 units.
- High-density nested cup packing reduces ocean freight per unit by up to 61%
- Pre-assembled folding handles minimize packaging air pockets
- Palletization matching European EPAL (1200x800) and US standard (48x40) specifications
Tiered MOQ & Tooling Amortization
OEM customization demands balanced capital expenditure between progressive deep-draw stamping dies and bespoke logo embossing modules.
- Stock mold utilization for custom laser engraving / PVD coatings from 1,000 pcs
- Custom tooling amortization schedules for bespoke capacity/taper ratios over 50,000 pcs
- Dynamic material hedging contracts protecting against nickel and chromium market volatility
Full Supply Chain Chain-of-Custody Audits
Procurement teams must guard against greenwashing penalties by enforcing rigorous third-party traceability from raw scrap receipt to finished warehouse dispatch.
- GRS Transaction Certificates (TC) provided per commercial shipment
- Spectrographic composition readouts confirming Cr-Ni balance per coil heat
- Sedex SMETA 4-Pillar and BSCI certified workplace social compliance
Metallurgical Specifications: Recycled Stainless Alloys
Evaluating chemical tolerances, tensile strength, and food-grade passivation performance for outdoor thermal hardware.
| Alloy Classification | Composition (Cr / Ni / Mo) | Tensile Yield (MPa) | Corrosion Resistance | Circular Feedstock Feasibility | Target Outdoor Application |
|---|---|---|---|---|---|
| Post-Consumer Recycled 304 (Austenitic) | 18.0 - 20.0% Cr / 8.0 - 10.5% Ni | ≥ 205 | Excellent (Neutral & Acidic Foods) | High (Up to 90% PCR scrap content) | Ultralight bushcraft cups, single-wall camp mugs, mess kits |
| Marine Grade Recycled 316 (Austenitic) | 16.0 - 18.0% Cr / 10.0 - 14.0% Ni / 2.0 - 3.0% Mo | ≥ 220 | Superior (Chloride & Sea Salt Spray) | Moderate (Dedicated alloy sorting required) | Coastal expeditions, alpine mountaineering, high-salinity field gear |
| Ferritic 430 Stainless (Economic Grade) | 16.0 - 18.0% Cr / 0% Ni (Magnetic) | ≥ 240 | Moderate (Sensitive to strong organics) | High (Abundant post-industrial scrap) | Entry-level promotional camping sets, dry storage canisters |
| Direct Induction 201 Stainless | 16.0 - 18.0% Cr / 3.5 - 5.5% Ni / 5.5 - 7.5% Mn | ≥ 310 | Lower (Prone to pitting in humid acidic zones) | High (High scrap volume in Asian markets) | Secondary non-food structural outer shells, handle hardware |
Manufacturing Architecture: From Coil to Finished Cup
Comprehensive breakdown of progressive stamping, ultrasonic degreasing, seam welding, and robotic finishing cells.
Stage 1: Multi-Action Deep Drawing
Continuous hydraulic stamping processes sheet circles into cylindrical cups via progressive deep draw dies. Precise punch radii prevent micro-thinning along bottom stress radiuses.
- Limiting Drawing Ratio (LDR) controlled to 2.1 to prevent micro-fractures
- Intermediate vacuum annealing at 1,050°C relieving work-hardening stress
- Automated visual laser sensors measuring continuous wall uniformity
Stage 2: Rolled Safety Rim & Handle Fusion
The raw upper edge is curled into a smooth 360-degree sanitary lip to prevent bacterial entrapment and ensure safe, burn-free contact for outdoor sipping.
- Rolled rim compression prevents lip splitting under boiling temperature contact
- Capacitor-discharge spot welding attaching folding wire brackets without punch marks
- Resistance pull testing validating weld joint retention over 30kg static load
Stage 3: Chemical Passivation & Surface Treatment
Ultrasonic cleaning strips all hydrocarbon lubricants prior to immersion in eco-compliant citric acid bath solutions, promoting chromium oxide passive film re-formation.
- Citric acid passivation meeting ASTM A967 food-contact standards
- Optional robotic abrasive bead blasting achieving tactical matte anti-scratch finishes
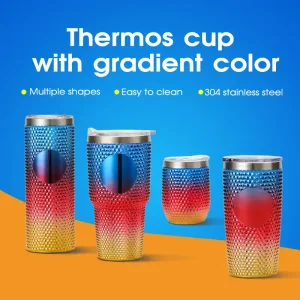
- PVD (Physical Vapor Deposition) titanium-gold, slate-black, or rainbow iridescent coatings
Global Regulatory Frameworks & Quality Mandates
Ensuring frictionless cross-border customs clearance and market compliance across North American, European, and Asia-Pacific retail corridors.
US FDA & California Proposition 65
Full testing verification under FDA 21 CFR 175.300 guarantees total safety under contact with high-temperature liquids and acidic bushcraft beverages (coffee, citrus broths).
- Lead and cadmium leaching verified at zero detection thresholds
- Total extractable fractions tested in distilled water and 8% ethanol
- No volatile organic compounds (VOCs) released across campfire heating
European LFGB & EU Regulation 1935/2004
Stricter than US requirements, European food contact legislation dictates intensive sensory and heavy metal migration testing across repeated use cycles.
- Specific migration limits (SML) for nickel, chromium, manganese, and iron
- Organoleptic testing confirming no metallic flavor transfer into boiling water
- DGCCRF compliance verification for French consumer product entry
GRS (Global Recycled Standard) Traceability
End-to-end chain of custody accounting authenticates actual post-consumer scrap input volume, shielding brands from severe false-advertising regulatory penalties.
- Batch-specific Scope Certificates (SC) and Transaction Certificates (TC)
- Wastewater treatment monitoring under ISO 14001 environmental frameworks
- Ethical workplace compensation audits under BSCI and Sedex monitoring
Engineering Roadmap (2025–2030): Next-Gen Outdoor Vessels
Emerging manufacturing technologies set to redefine performance, weight reduction, and circular accountability over the next five years.
Green Hydrogen DRI Steel Integration
By 2027, tier-1 smelting partners will transition secondary scrap melting into 100% green-hydrogen direct reduced iron (DRI) processes, achieving true net-zero embodied carbon.
Digital Product Passports (DPP) via Laser QR
Direct-to-metal fiber laser etching of serialized micro-QR matrixes, granting consumers and municipal recyclers instant smartphone access to material heat composition, scrap percentage, and recycling hubs.
Plasma-Assisted Superhydrophobic Nanocoatings
Fluorine-free chemical vapor deposition (CVD) creating nano-textured silica barriers inside the cup that repel grease, tea stains, and coffee residue, drastically cutting trail water needed for camp dishwashing.
Frequently Asked Questions: B2B Sourcing & Engineering
Critical metallurgical, logistics, and compliance data for sourcing directors, brand managers, and quality assurance leads.
Does utilizing recycled stainless steel alter the mechanical strength or corrosion resistance compared to virgin steel?
No. When processed via certified secondary metallurgy in Electric Arc Furnaces, post-consumer scrap is refined down to molecular elements. Once the chemical balance of Chromium (18-20%) and Nickel (8-10.5%) is verified and homogenized, recycled 304 stainless steel exhibits identical yield strength (≥205 MPa), elongation (≥40%), and passive corrosion resistance to virgin mined steel. Metallurgical test coupons are provided with every batch mill certificate.
What documentation is supplied to verify authentic recycled content claims to retail consumers?
We supply official Global Recycled Standard (GRS) Transaction Certificates (TC) issued by accredited certification bodies (such as IDFL or Intertek) linking our finished batch lot numbers directly to upstream scrap procurement inputs. In addition, Material Test Reports (MTR) according to EN 10204 type 3.1 are provided to authenticate chemical composition and mechanical properties.
Can these small recycled camping cups be heated directly over open fires or camp stoves?
Single-wall construction cups are 100% campfire- and gas-burner safe, provided there are no plastic or silicone trim accessories attached. We utilize high-temperature spot welding for handles and high-purity alloy compositions that withstand direct flame contact up to 800°C without structural warping or delamination. For double-wall vacuum cups, direct flame contact is strictly prohibited due to internal pressure expansion hazards.
What are your standard factory Minimum Order Quantities (MOQs) and sampling lead times?
For standard existing tooling configurations utilizing in-stock GRS-certified recycled steel coils, our baseline MOQ begins at 1,000 units with custom laser etching or single-color pad printing. For custom Pantone powder coatings or bespoke physical vapor deposition (PVD) finishes, the MOQ is 3,000 units. Prototype tooling samples require 10–14 business days, while volume mass production runs typically complete within 30–40 days post-sample approval.
How do you prevent metallic aftertaste in stainless camping drinkware?
Metallic odor or taste in low-grade steel is caused by residual micro-scale drawing oils and unpassivated free iron molecules on the cup interior. We employ a rigorous three-step prevention process: high-frequency ultrasonic chemical degreasing, followed by automated immersion in a heated citric acid passivation bath (conforming to ASTM A967), and completed with high-temperature deionized water sanitization. This establishes an impervious chromium-oxide layer that ensures zero beverage flavor alteration.
What surface decoration techniques offer maximum longevity against rugged outdoor abrasions?
For extreme alpine or tactical environments, we recommend high-precision fiber laser annealing or mechanical stone-washing/bead-blasting, both of which are completely immune to chipping or peeling. For branded coloration, our robotic thermoset matte powder coating delivers superior scratch resistance (4H pencil hardness rating) compared to conventional wet liquid spraying, easily enduring contact with carabiners, rocks, and outdoor pack hardware.
Commercial Lineup & Production Matrix (Batch B)
Explore additional high-demand drinkware models ready for private label OEM/ODM customization and container volume distribution.