Precision Engineering Solutions
Flagship Sublimation-Ready Stainless Steel & Eco Vessel Systems
Explore our top-tier catalog engineered for intense vacuum thermal stability, optimal pigment acceptance, and premium retail conversion.
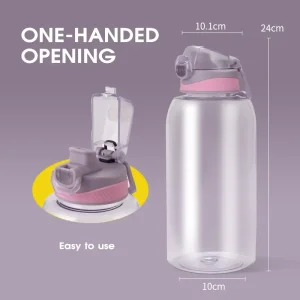
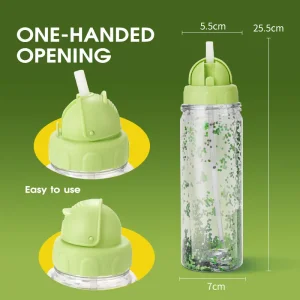
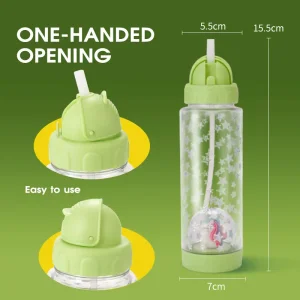
Technical Whitepaper
Macro Industry Solutions: Engineering the Circular Drinkware Paradigm
Navigating stringent Scope 3 reporting, carbon cross-border adjustments (CBAM), and high-yield sublimation requirements without sacrificing thermal dynamics.
PCR 304/316 Metallurgy
Raw scrap recovery is rigorously governed through induction refining to maintain austenitic crystal integrity. We integrate up to 90% certified Post-Consumer Recycled (PCR) steel, lowering cradle-to-gate embodied carbon by over 68% relative to virgin smelting while retaining identical yield strength.
Sublimation Polymer Coating
Standard stainless steel cannot natively absorb disperse dyes. Our automated cleanrooms deposit an electrostatically balanced, micron-precise cross-linked polymeric resin. This coating exhibits extreme thermal resistance during heat transfer (200°C/392°F) without micro-cracking or yellowing.
Zero-VOC Eco Finishing
To safeguard green tier procurement standards, our surface preparation utilizes closed-loop de-ionized washing followed by ultra-low VOC waterborne polyurethanes. The finish satisfies FDA 21 CFR §175.300 and LFGB standards for indirect food packaging compatibility.
68.4%
Carbon Emissions Reduction
200°C
Cure Heat Tolerance
5B
Cross-Hatch Adhesion Grade
100%
Chain-of-Custody Traceability
Market Dynamics
Global Commercial & Industrial Landscape
How regional sustainability regulations, retail trends, and print-on-demand infrastructure are driving bulk procurement shifts worldwide.
North America (POD Expansion)
The North American promotional merchandise and creator economy sectors are witnessing exponential demand for blank sublimation cylinders. Wholesalers demand tight dimensional tolerances (±0.2mm) to ensure uniform pressure during rotary heat-press cycles and convective oven sublimation.
Europe (CSRD & CBAM Enforcement)
European importers face direct reporting requirements under the Corporate Sustainability Due Diligence Directive (CSDDD). Providing certified Recycled Content Verification (ISO 14021) is no longer a marketing choice—it is a mandatory customs clearance hurdle.
Asia-Pacific (Supply Chain Integration)
Centering manufacturing in Wuyi, Zhejiang leverages hyper-localized raw material clusters. From deep-drawing machinery to robotic liquid coating lines and in-house tooling, end-to-end integration lowers unit costs while safeguarding strict export quality standards.
Commercial Scenarios
Targeted Commercial Applications & Deployment
Engineered across specific verticals requiring edge-to-edge color permanence, food safety, and mechanical endurance.
Retail Merchandising
Direct drop-ship blanks for national gift chains, licensed sports franchises, and boutique lifestyle brands requiring rich, full-bleed 300+ DPI photograph prints.
Corporate ESG Programs
High-end employee onboarding kits and sustainable corporate incentives backed by third-party recycled material certificates and transparent life-cycle analysis.
Outdoor & Adventure
Double-wall vacuum vessels built to endure drop impacts, harsh washing conditions, and thermal retention specs (up to 24hr cold / 12hr hot) for adventure gear brands.
Specialty Beverage
Custom tumbler bodies combined with specialized splash-proof lids (helmet, spring-loaded, and straw caps) tailored for coffeehouse chains and drive-thru retail programs.
Risk Mitigation
Institutional Compliance & Quality Engineering
Our engineering protocols bridge Chinese manufacturing capacity directly to Western compliance frameworks.
Chain of Custody (GRS/RCS)
Every shipment includes authentic Transaction Certificates (TC) tracking stainless steel scrap from certified collectors straight through melt, re-rolling, forming, and finishing. No greenwashing risks.
Food Contact Toxicological Tests
Both the interior lining and sublimation coating undergo rigorous analytical checks: California Prop 65 (Lead/Cadmium limits < 90 ppm), REACH SVHC screening, and heavy metal leachability tests conducted via accredited labs (SGS/TÜV).
Ningbo Maritime Corridor Logistics
Located in Wuyi, Jinhua, our operations sit adjacent to Ningbo and Shanghai maritime hubs. We manage bonded warehousing, consolidated container packing, and verified gross mass (VGM) declarations seamlessly.
Future Innovations
Technical Roadmap: Next-Gen Sublimation Metallurgy
Advancing circular thermal drinkware through bio-polymers, laser sintering, and automated visual defect detection.
Phase 1: Present
PCR 90 Optimization
Standardizing 90% certified post-consumer scrap steel across all vacuum blank series, cutting production energy consumption by 45%.
Phase 2: Next Gen
Bio-Based Coatings
Formulating plant-derived, solvent-free sublimation receivers that achieve commercial dishwasher endurance up to 100+ residential wash cycles.
Phase 3: Smart QC
AI Inline Spectroscopy
Deploying machine vision to verify coating micro-thickness within ±1.5 microns across curved geometries to guarantee zero color banding.
Phase 4: Full Circle
Closed-Loop Takeback
Partnering with regional distributors to facilitate post-use re-collection and re-melting, establishing true cradle-to-cradle product lifecycles.
Procurement Intelligence
Frequently Asked Technical Questions
Clear, engineering-level answers to address bulk purchasing, coating performance, and compliance inquiries.
What differentiates recycled stainless steel from virgin stainless steel in drinkware manufacturing?
From a metallurgical and crystal structure perspective, certified Post-Consumer Recycled (PCR) 304 or 316 stainless steel is virtually identical to virgin steel. During electric arc furnace (EAF) induction remelting, impurities are fully removed, achieving equivalent tensile strength, corrosion resistance, and food-contact inertness. The critical distinction lies in environmental impact: PCR steel consumes roughly 70% less energy and slashes greenhouse gas emissions by up to two-thirds compared to virgin bauxite/iron-ore smelting routes.
How does the sublimation receiver coating maintain adhesion under intense heat presses?
Sublimation requires transferring disperse inks at roughly 190°C to 205°C (374°F - 401°F) under mechanical contact pressure. Standard organic paints blister or peel under these conditions. We apply specialized thermoset polyester-polyurethane hybrid coatings. These cross-link molecularly with the treated metal substrate at 210°C during pre-curing, creating a high-density, glass-hard polymer lattice that allows gasified sublimation inks to diffuse deeply without degrading the base film.
Can you supply official Transaction Certificates (TC) for global customs audits?
Yes. As a verified supplier adhering to Global Recycled Standard (GRS) and Recycled Claim Standard (RCS) protocols, we generate valid batch-specific Transaction Certificates issued through accredited certifiers. These documents link your export bill of lading directly to the recycled scrap material source, satisfying North American FTC Green Guides and EU anti-greenwashing directives.
What parameters do you recommend for rotary vs. convection oven sublimation?
For cylinder press machinery, our technical team recommends running at 195°C (385°F) for 45 to 60 seconds with medium-to-firm pressure, rotating 180° halfway through if pressing full-bleed wraps. For vacuum tunnel convection ovens using silicone shrink film, optimal curing sits at 200°C (392°F) for 6 to 7 minutes. Exact times may vary slightly based on ambient factory temperature, paper transfer weight, and ink saturation levels.
What are the minimum order quantities (MOQ) and production lead times for custom blanks?
For catalog blank stock with our standard white gloss or matte sublimation coating, MOQs begin at 1,000 units. For fully customized vessel profiles, specialized Pantone gradient base sprays, or proprietary injection lids (such as our Eco-Helmet or Spring-Loaded assemblies), initial tool development requires 15 to 20 days, followed by mass production runs within 30 to 45 days.
Complete Manufacturing Portfolio
Wholesale Product Lineup & Customization Modules
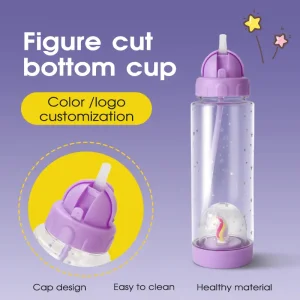
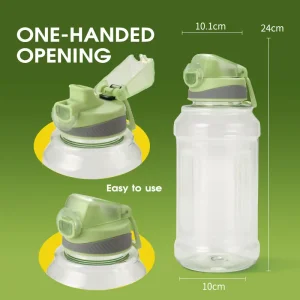
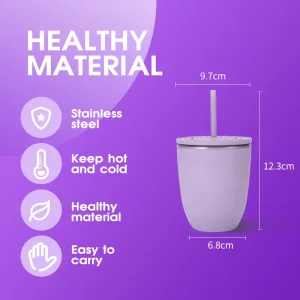
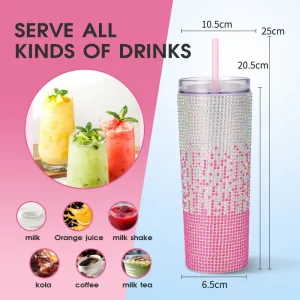
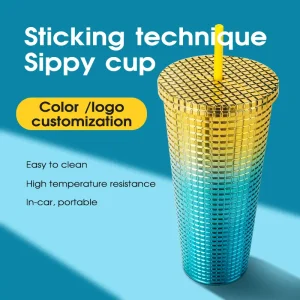
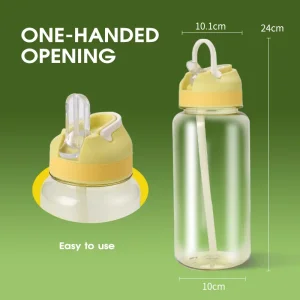
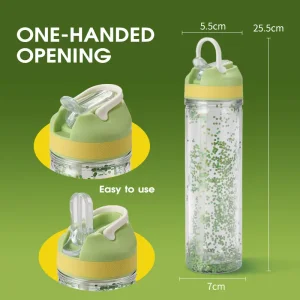
Explore our full line of eco-engineered drinkware, specialized closures, and distinctive electroplated/drill-sticker vessels.